 en
 fr
 es
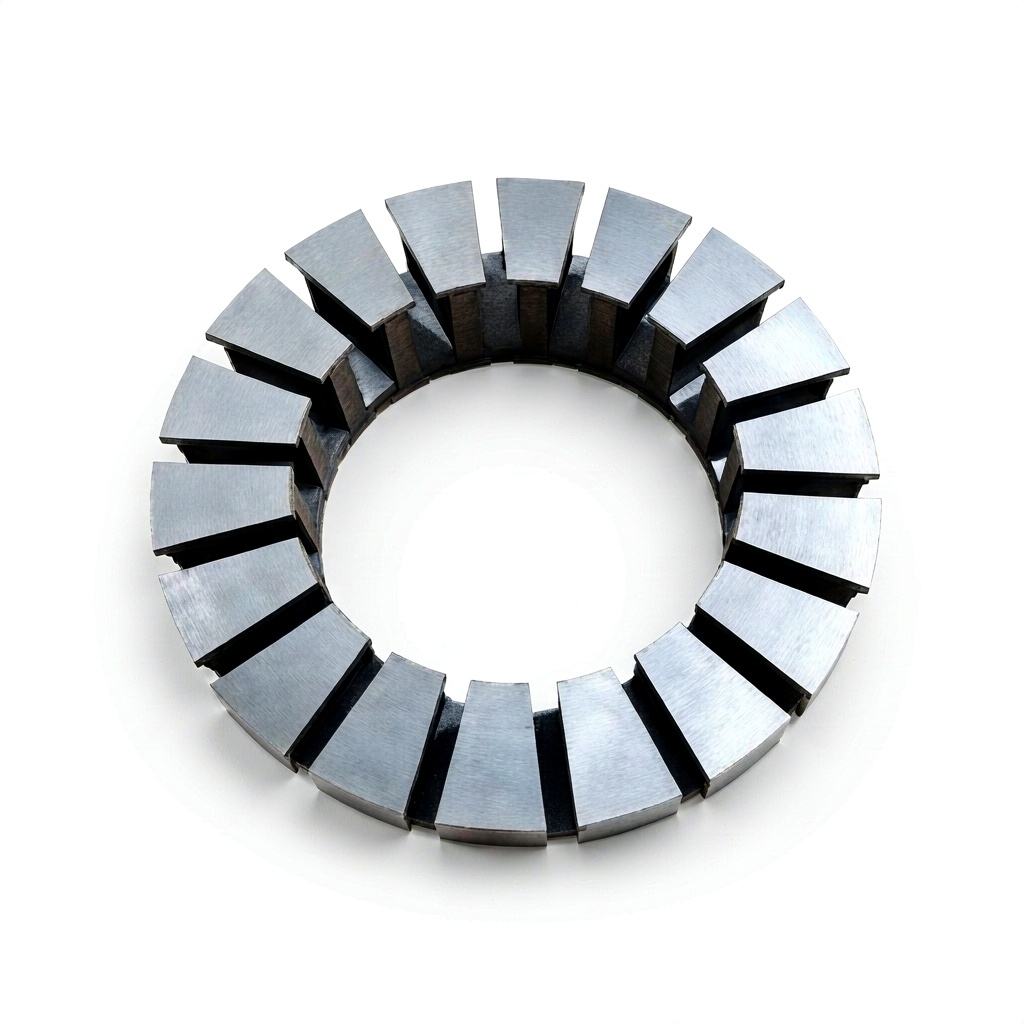
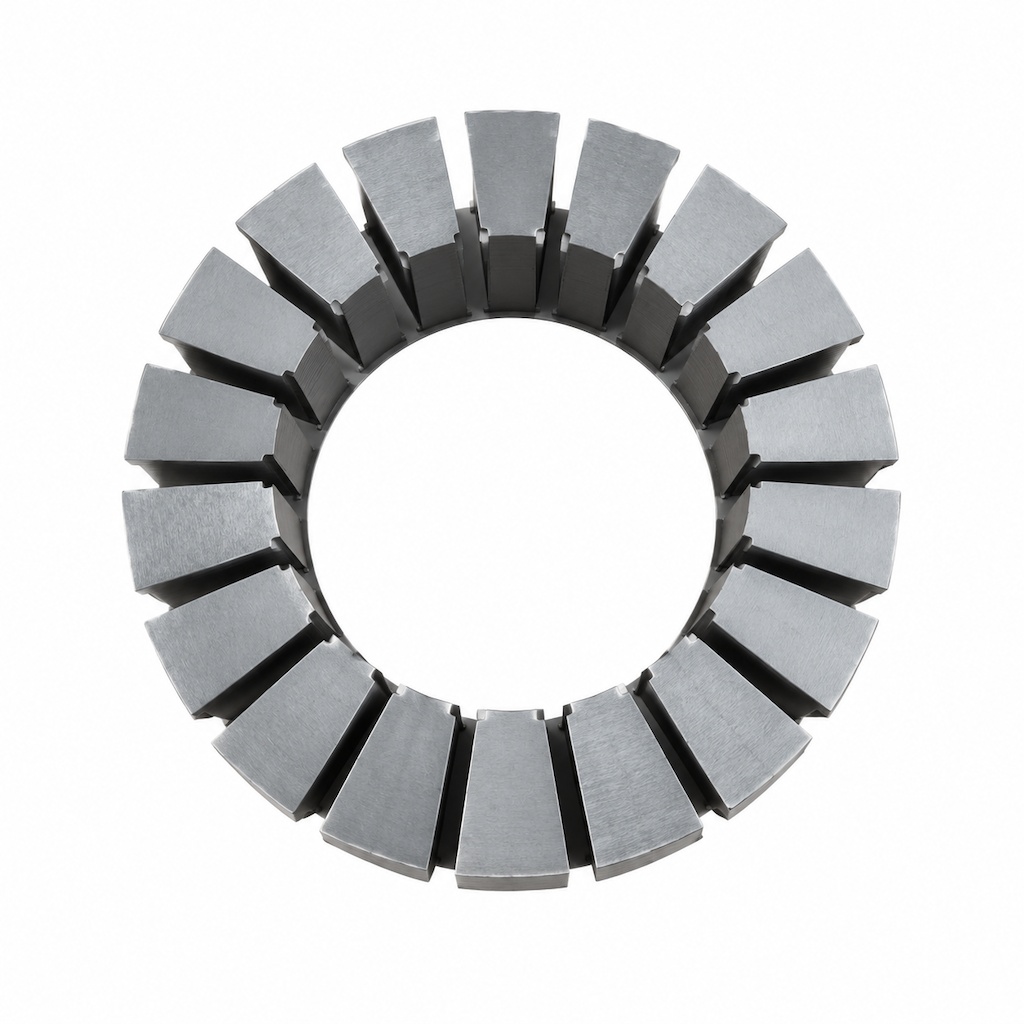
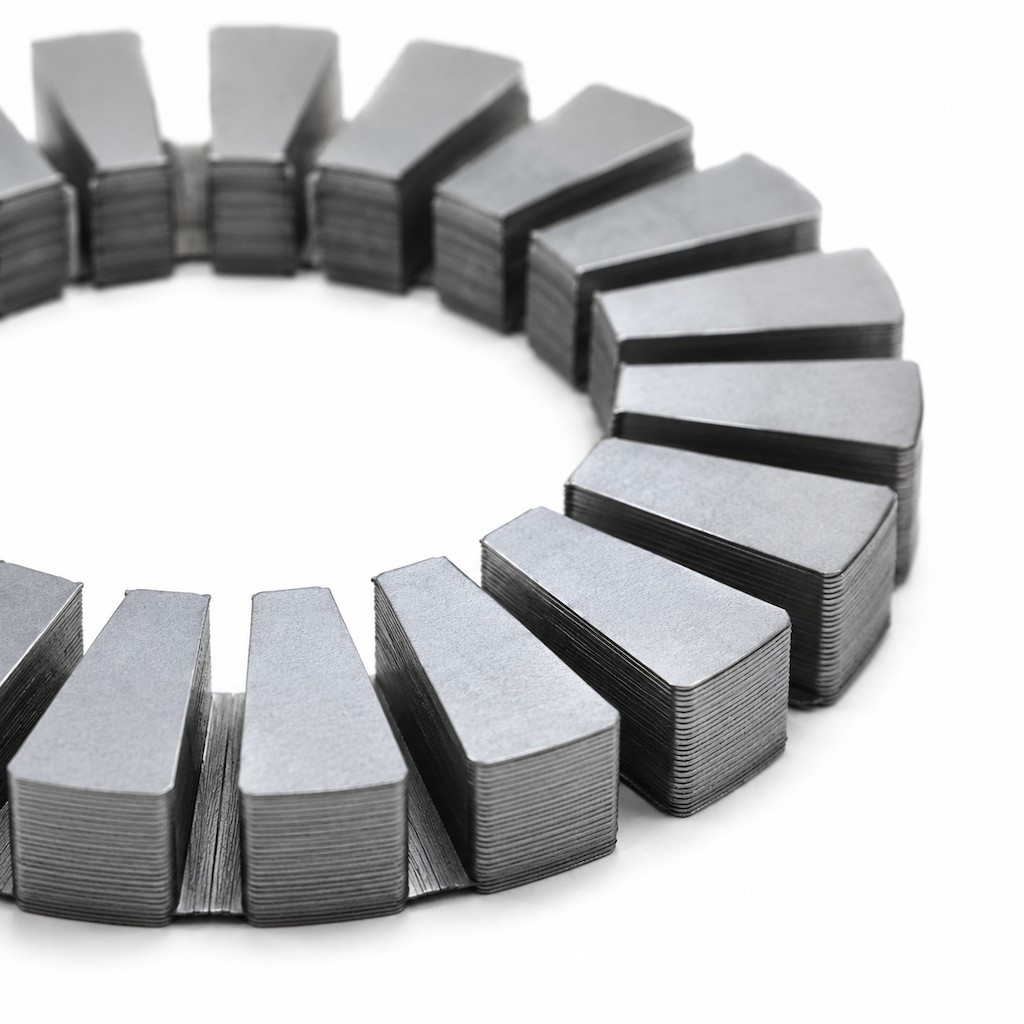
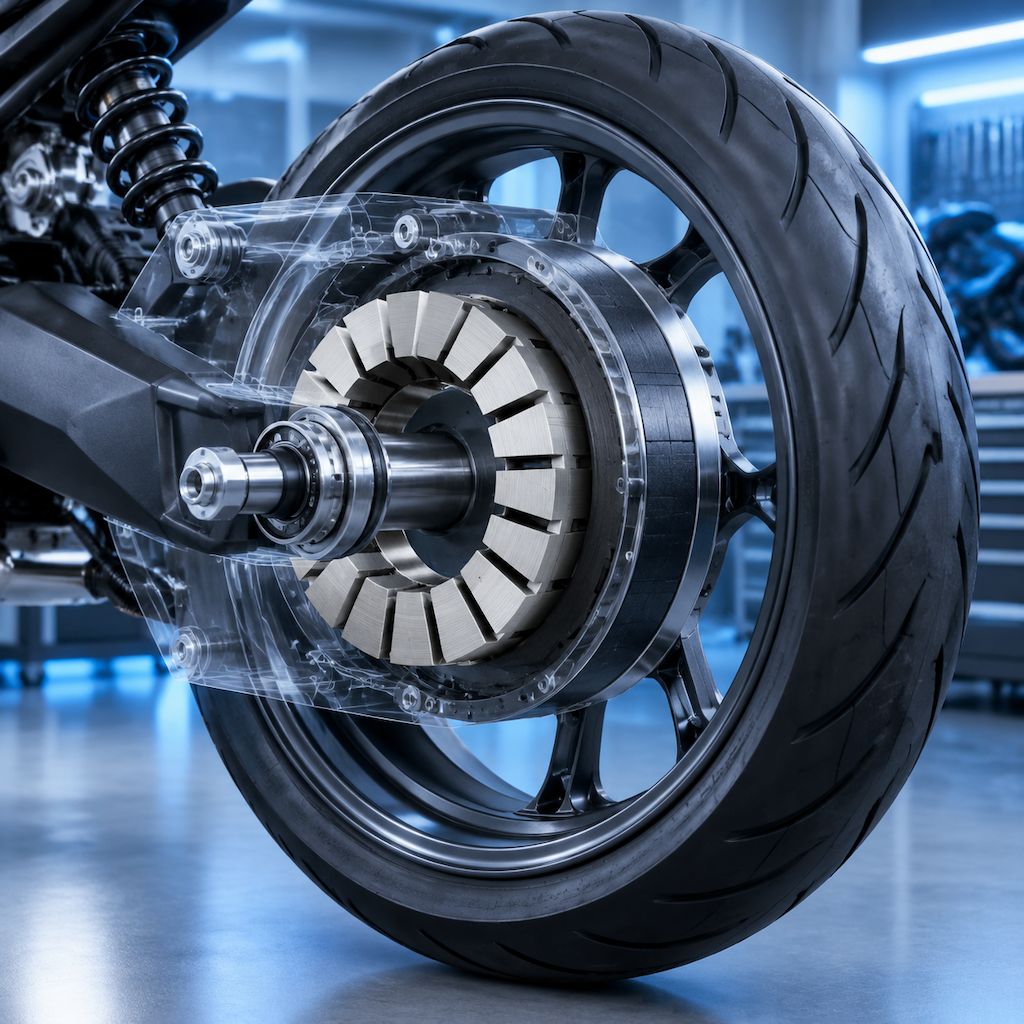
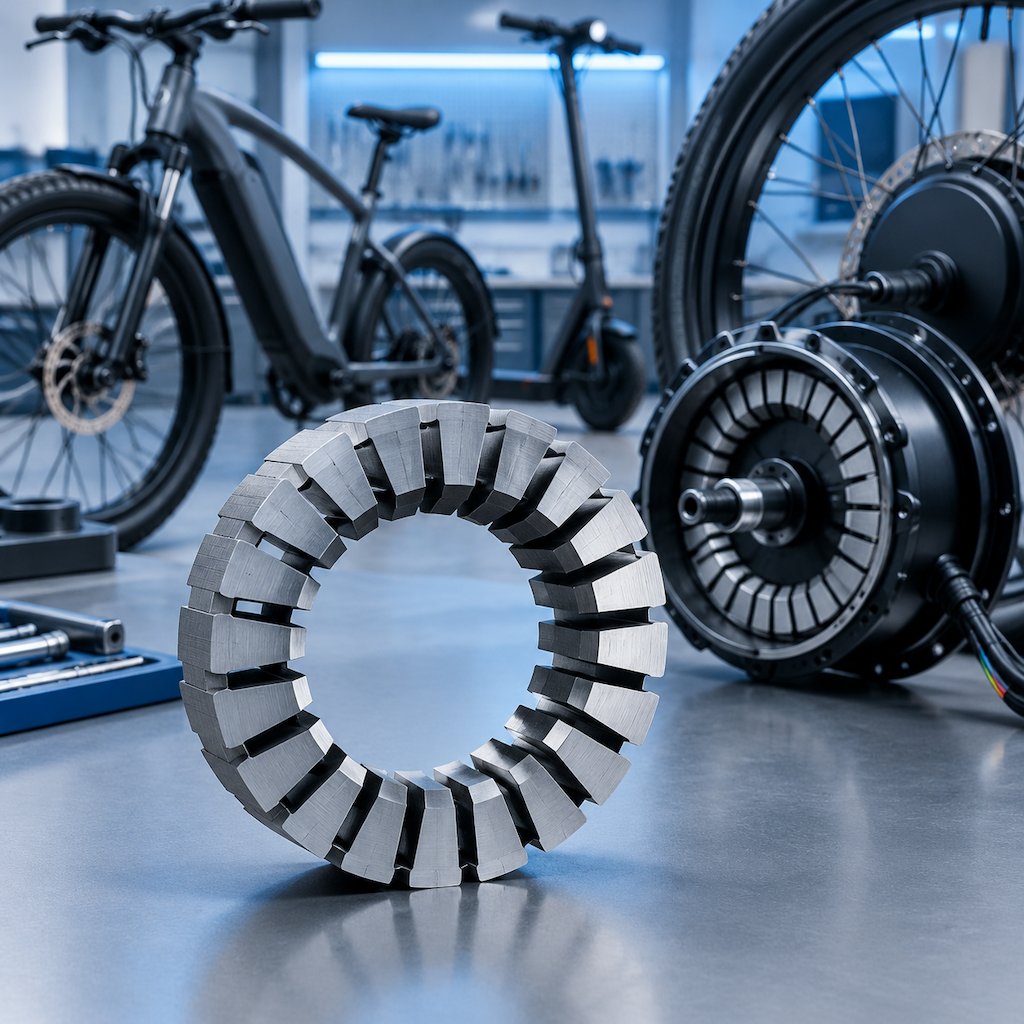
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
Product Origin :
CHINAShipping Port :
NANSHA/SHEKOU/SHANGHAI/NINGBOPayment :
TT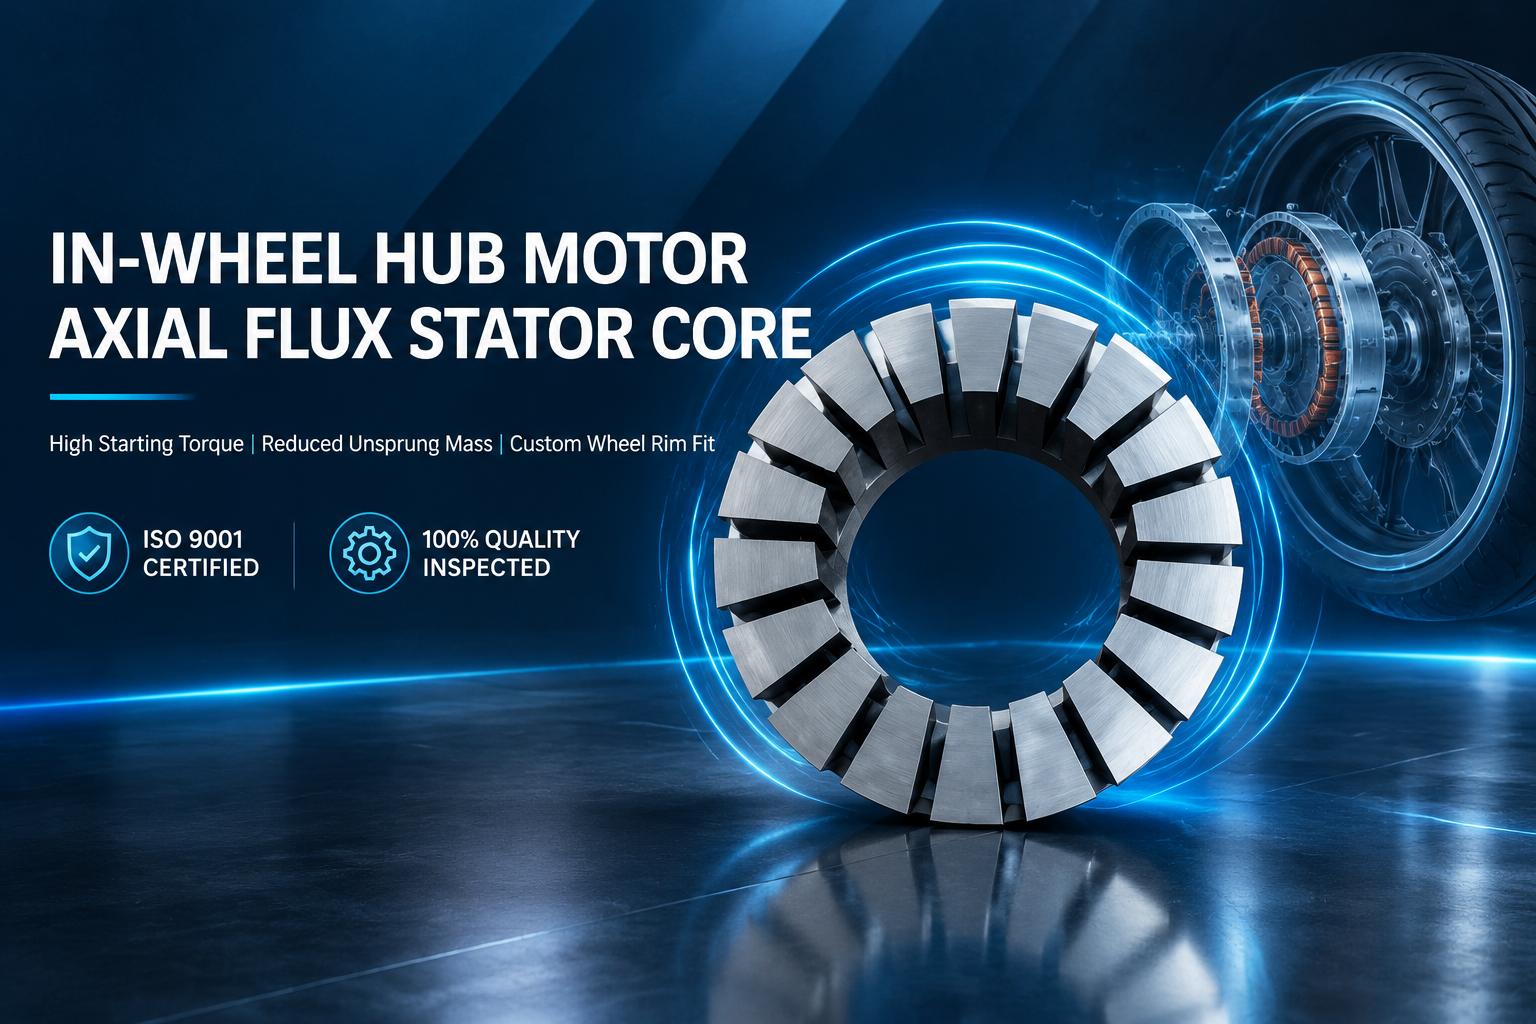
Shunge Steel manufactures custom wound axial flux stator cores specially designed for in-wheel hub motors, direct-drive electric motorcycle powertrains, high-performance e-bikes, and light electric vehicles (LEVs). In hub motor applications, eliminating transmission gears and packaging the motor directly inside the wheel rim demands maximum torque density, compact axial depth, and minimal unsprung weight.
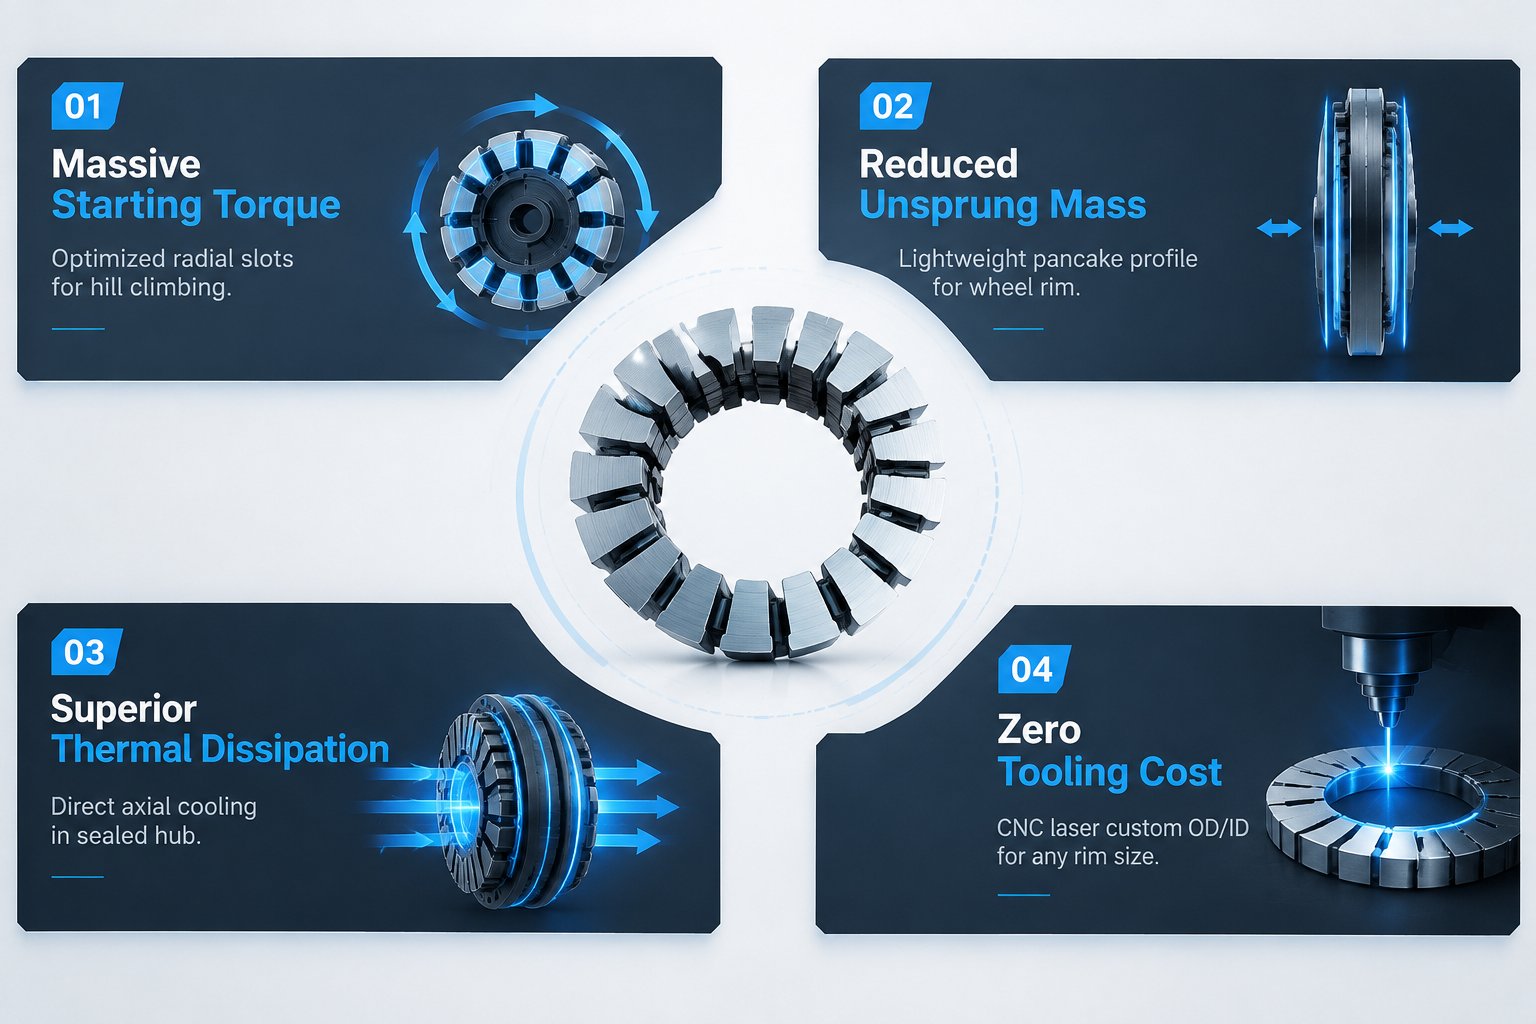
By winding continuous high-grade non-oriented silicon steel into an optimized disc ring and forming deep radial slots via high-precision CNC laser cutting, we deliver stator cores that provide intense magnetic flux utilization, exceptional starting torque, and superior cooling characteristics without costly stamping dies.
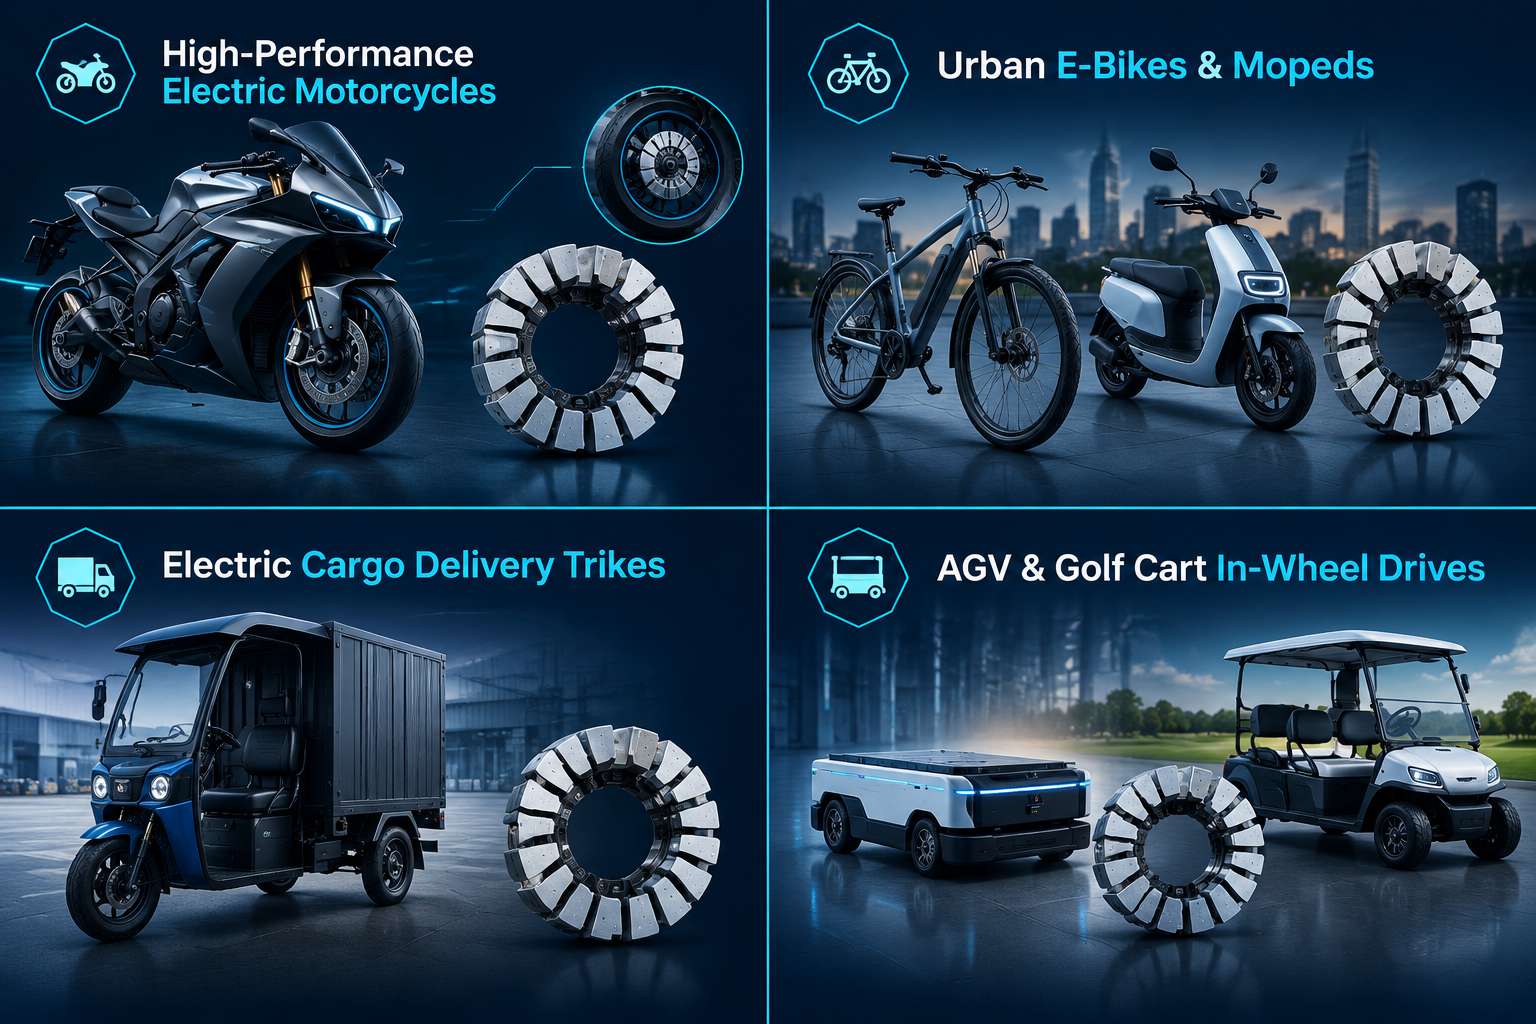
Our custom wound hub motor cores are built to withstand rigorous road shock, heavy vibration, and demanding duty cycles across diverse light electric mobility sectors:
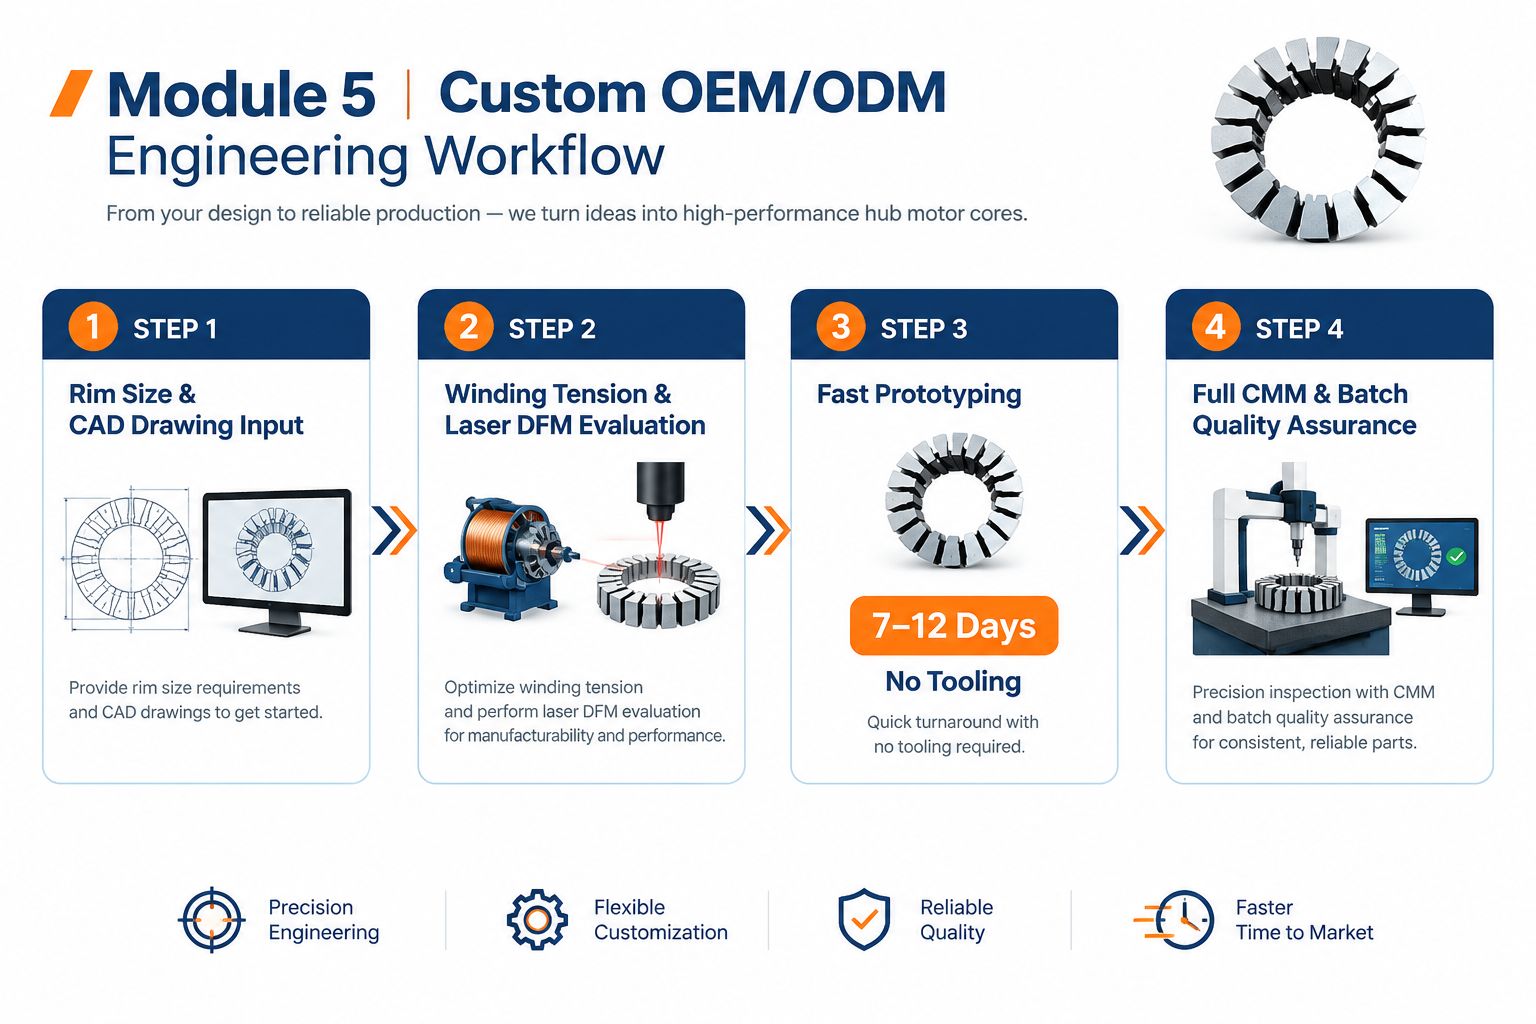
We collaborate closely with electric vehicle motor designers to deliver tailored stator core solutions:
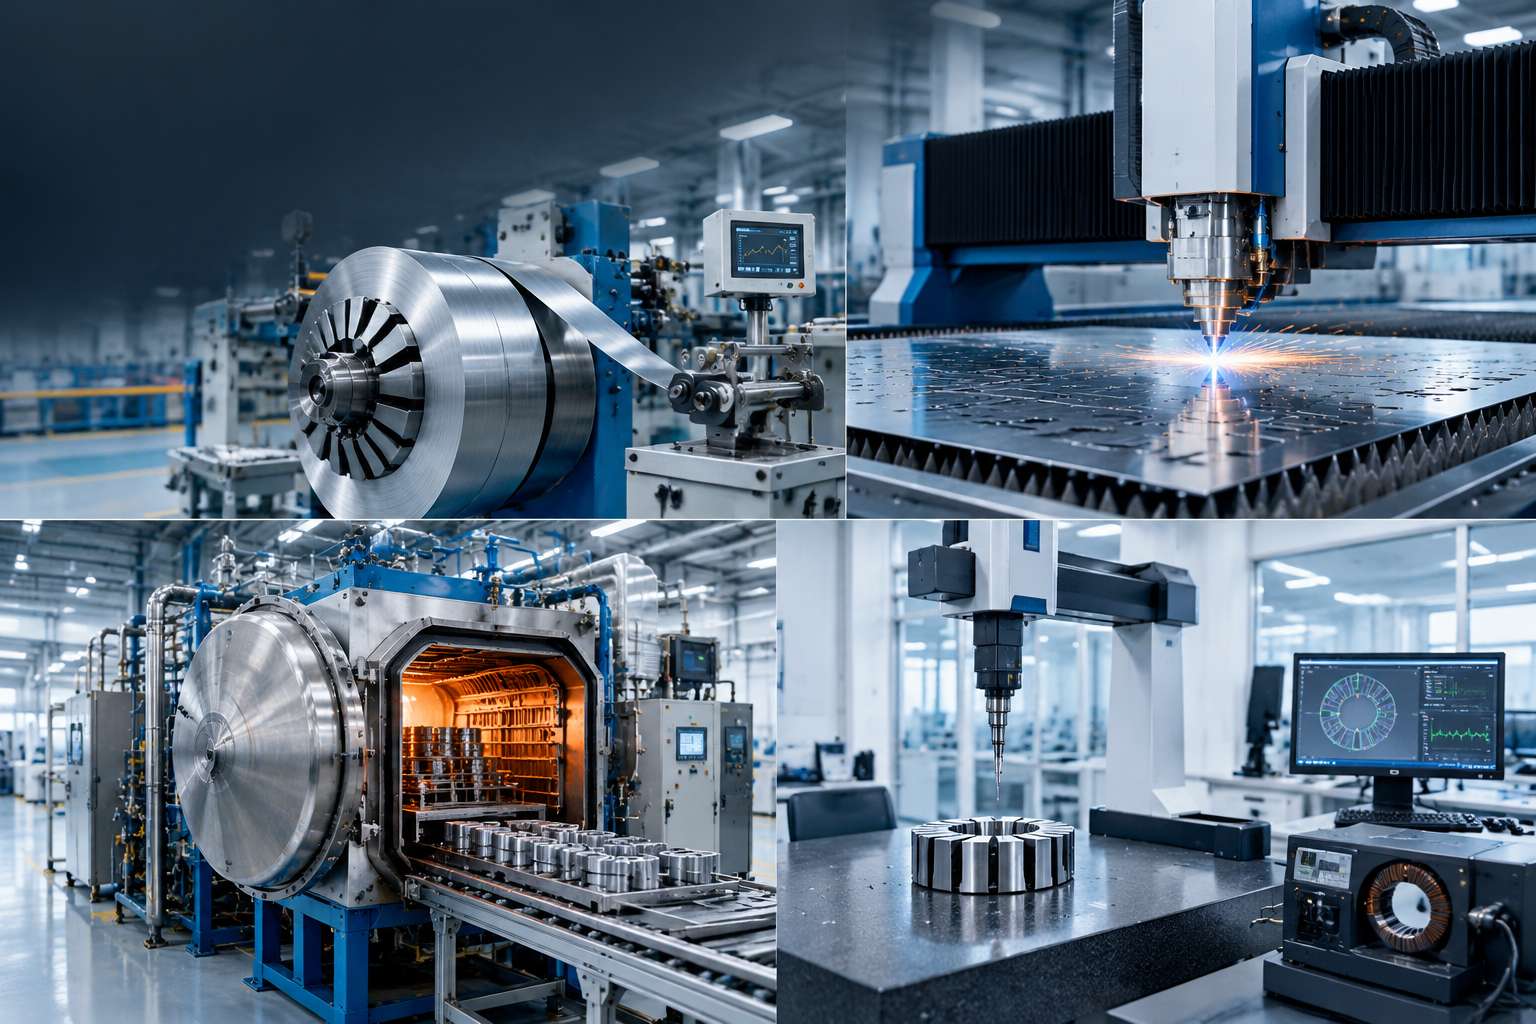
Shunge Steel maintains rigorous quality control across every manufacturing stage to guarantee road-grade reliability:
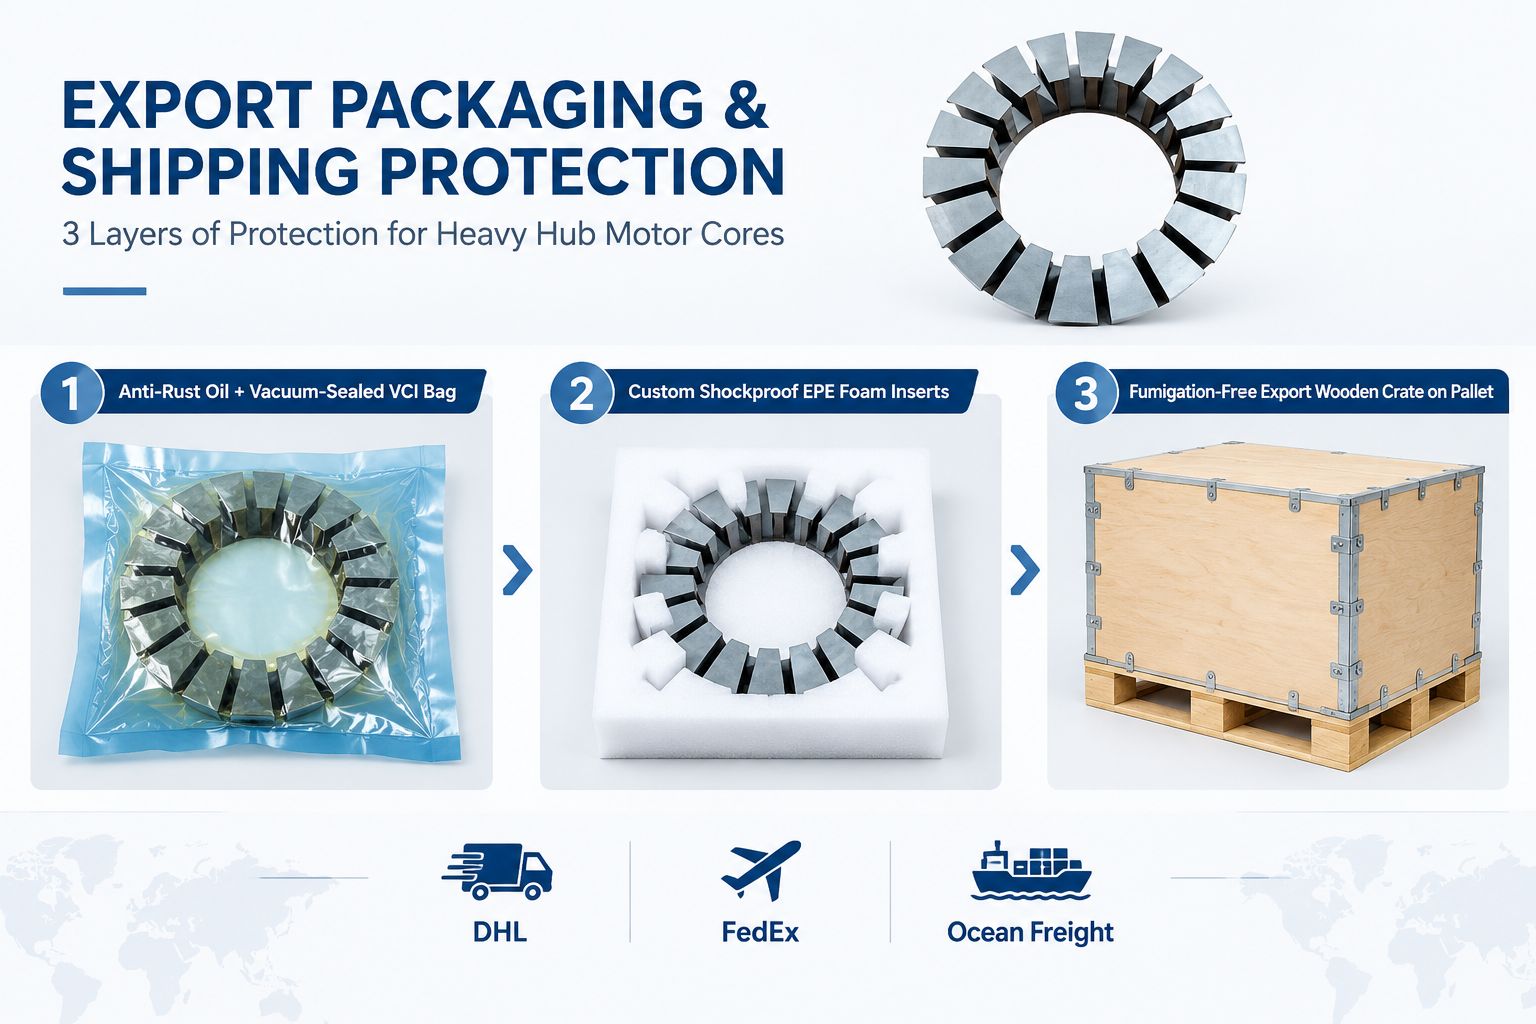
To ensure cores arrive in pristine condition ready for automated winding and assembly:
Q1: Why is an axial flux motor stator core superior for in-wheel hub motors compared to a radial flux core?
A: Axial flux motors produce significantly higher torque density because their active magnetic area is located at a larger diameter near the wheel perimeter. Furthermore, their ultra-flat pancake geometry fits neatly inside wheel rims without requiring transmission gearboxes, reducing unsprung weight and improving vehicle dynamics.
Q2: Can you accommodate large center bore (ID) requirements for hollow-axle hub motor designs?
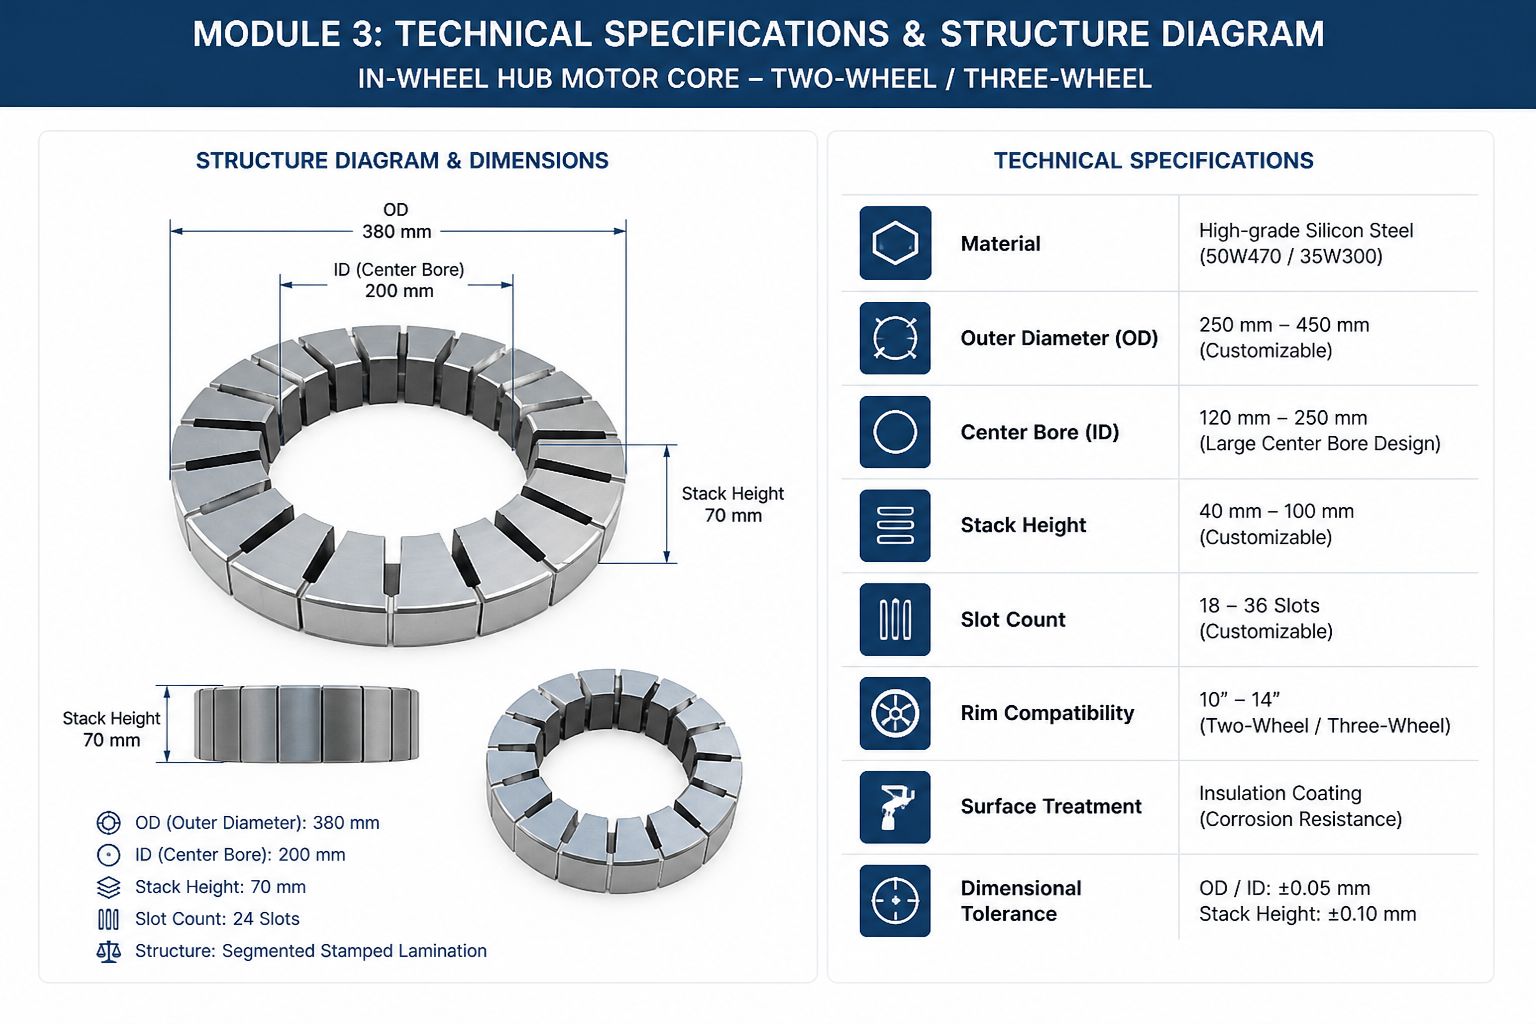
A: Yes. Because our cores are wound from electrical steel strip and laser-slotted, we can customize the inner diameter to match your exact hollow axle, wheel bearing, or internal brake mounting dimensions.
Q3: What electrical steel thickness should be selected for electric motorcycle hub motors?
A: For urban e-bikes and standard speed scooters (operating below 1000 RPM), 0.35 mm or 0.50 mm electrical steel provides excellent torque at high cost efficiency. For high-speed electric motorcycles operating at higher electrical frequencies, 0.20 mm or 0.27 mm thin-gauge steel is recommended to minimize high-speed eddy current losses.
Q4: Do design changes require purchasing new stamping tooling?
A: No. All slot features, skew angles, and diameters are generated by CNC laser cutting. You can iterate and refine your electromagnetic design without paying for costly stamping dies or waiting for tooling lead times.
Q5: What is the typical lead time for prototype hub motor cores?
A: Prototype orders are typically manufactured, inspected, and dispatched within 7 to 12 working days following CAD drawing confirmation.
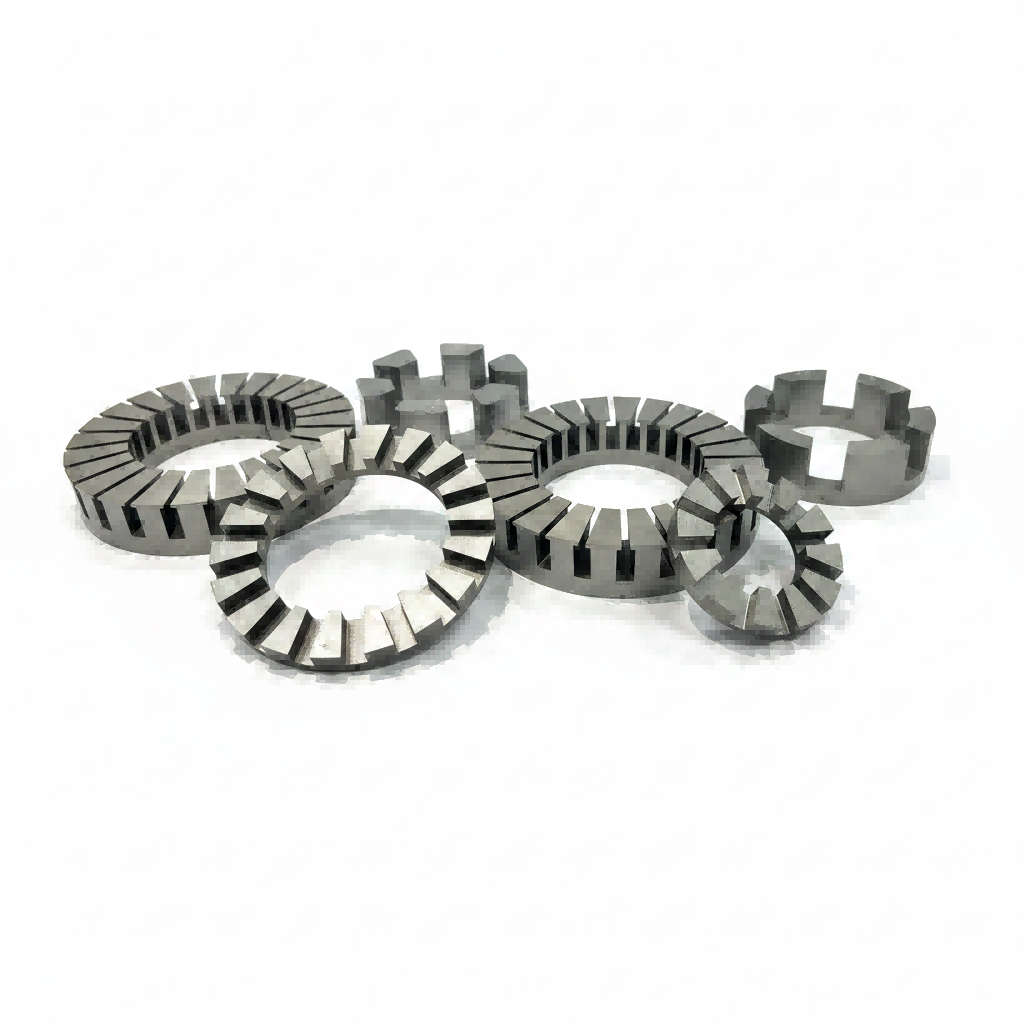
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
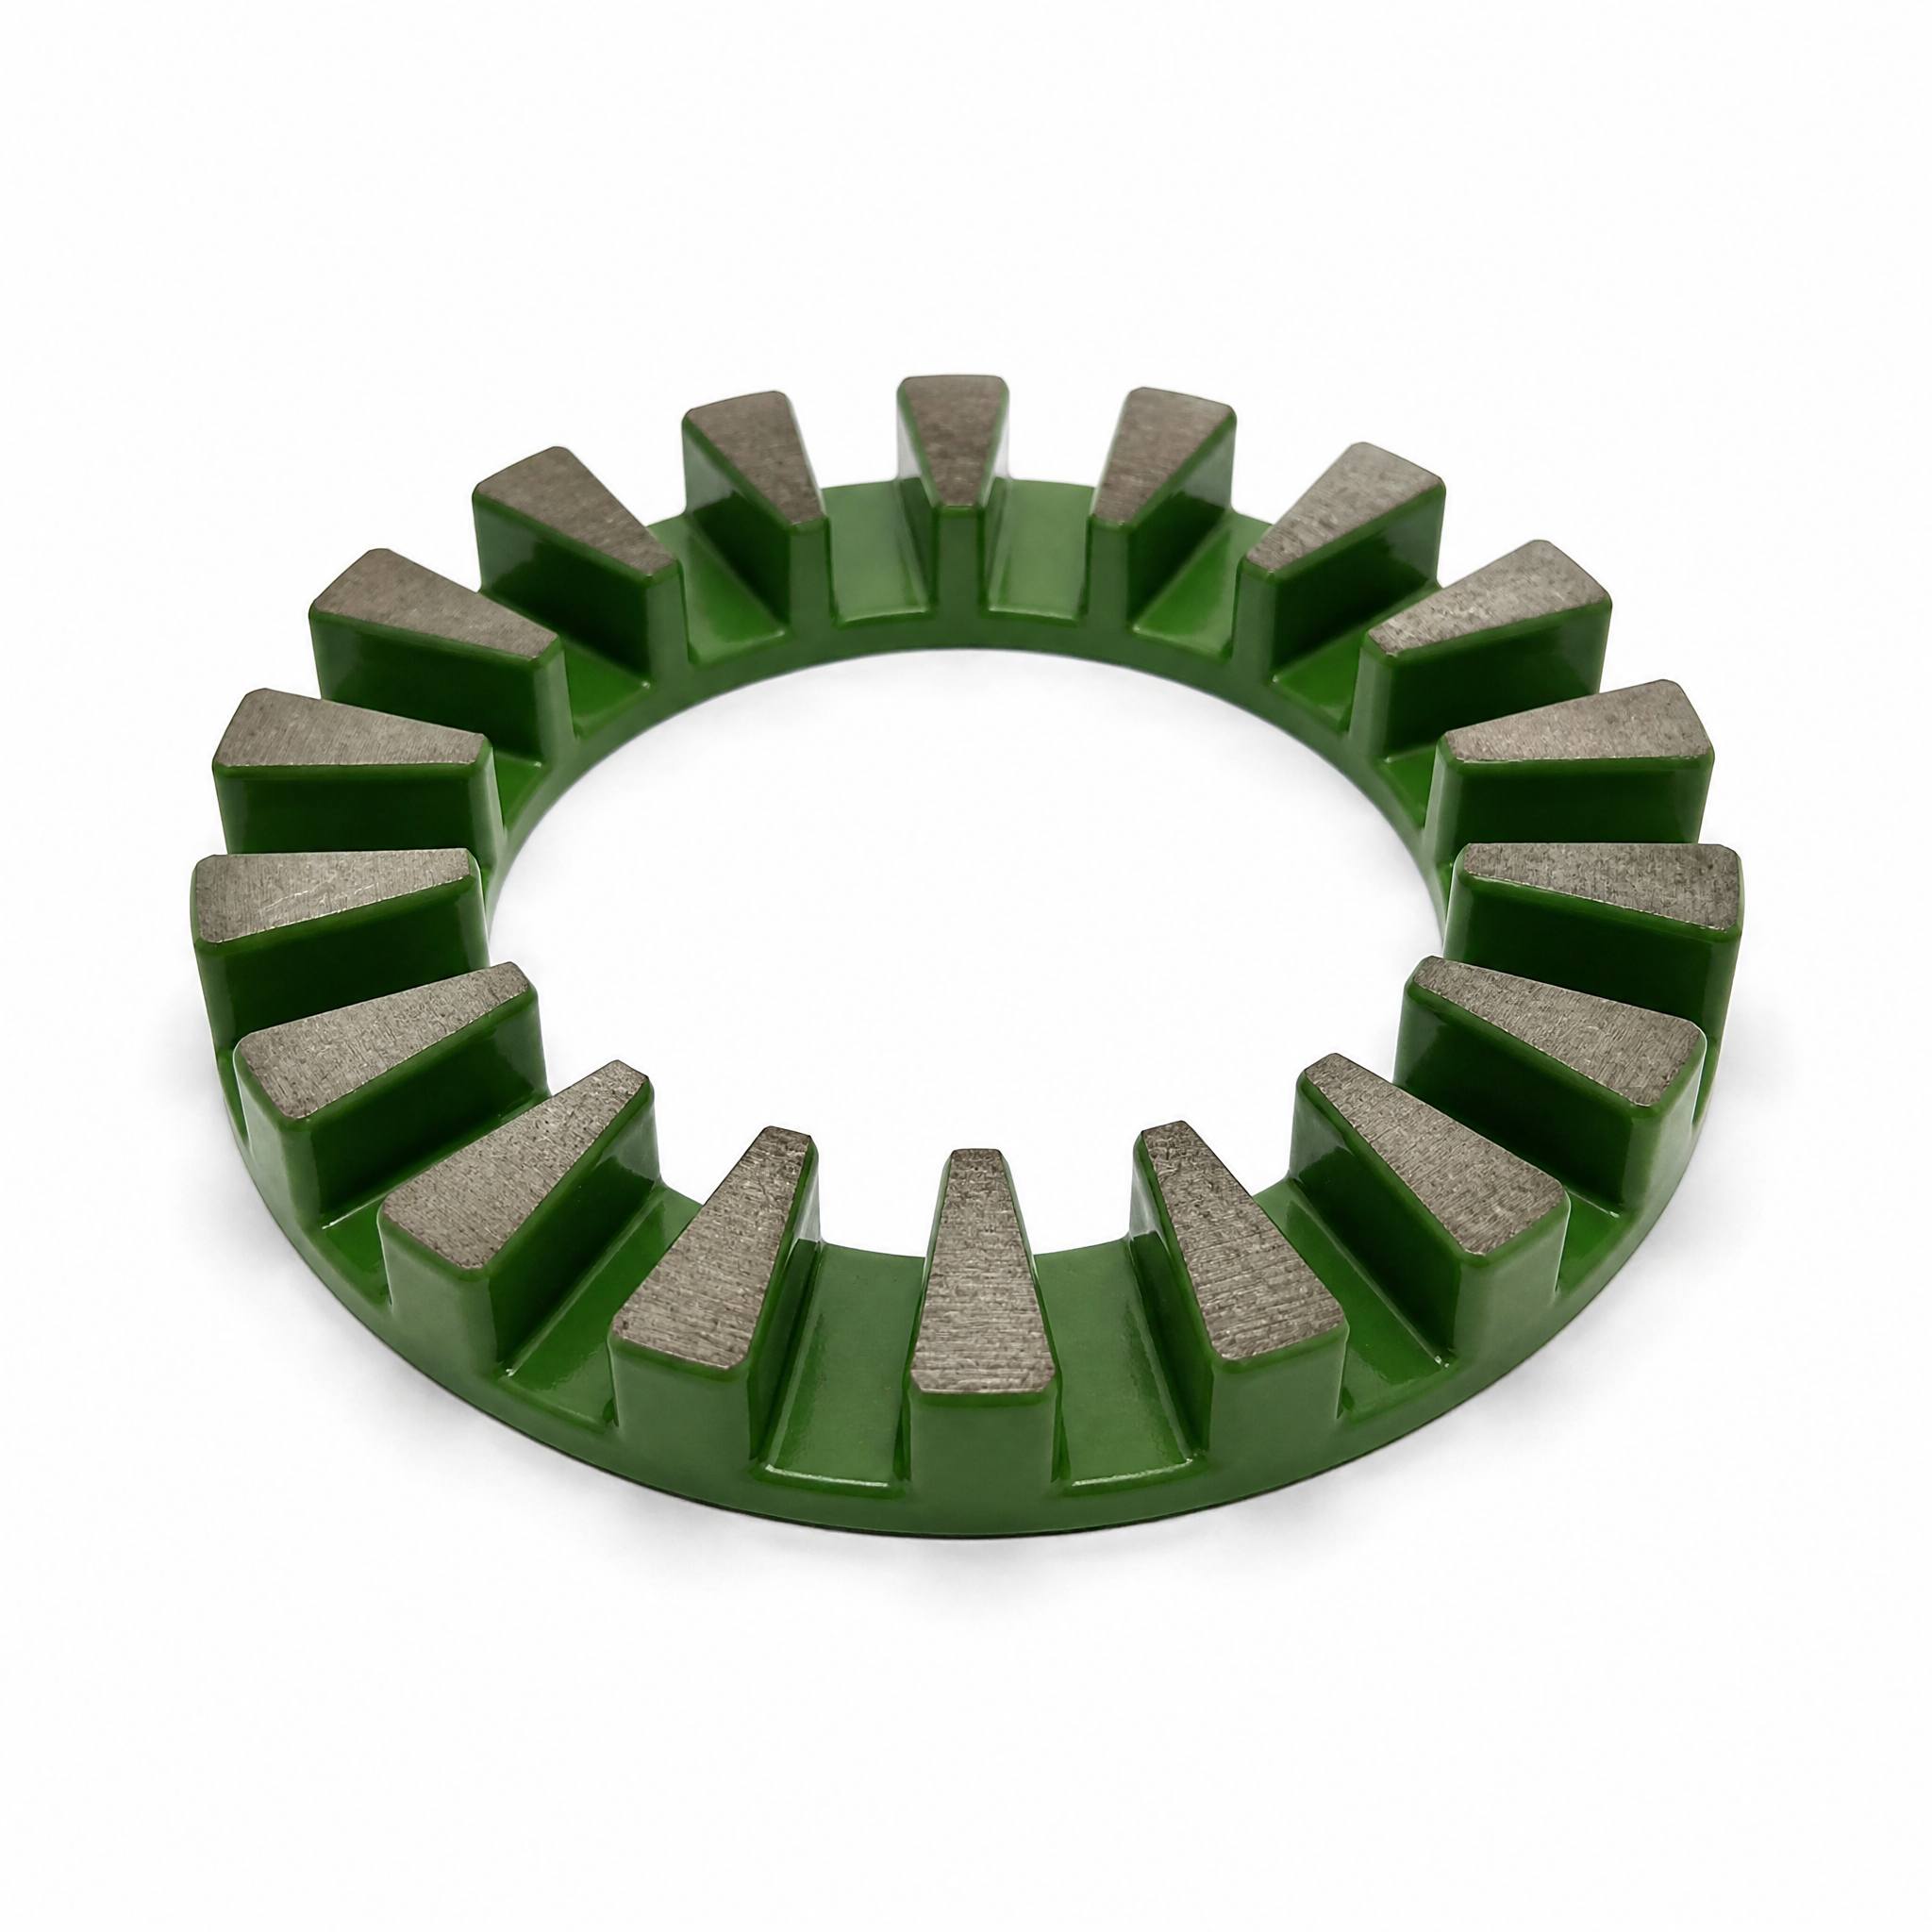
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
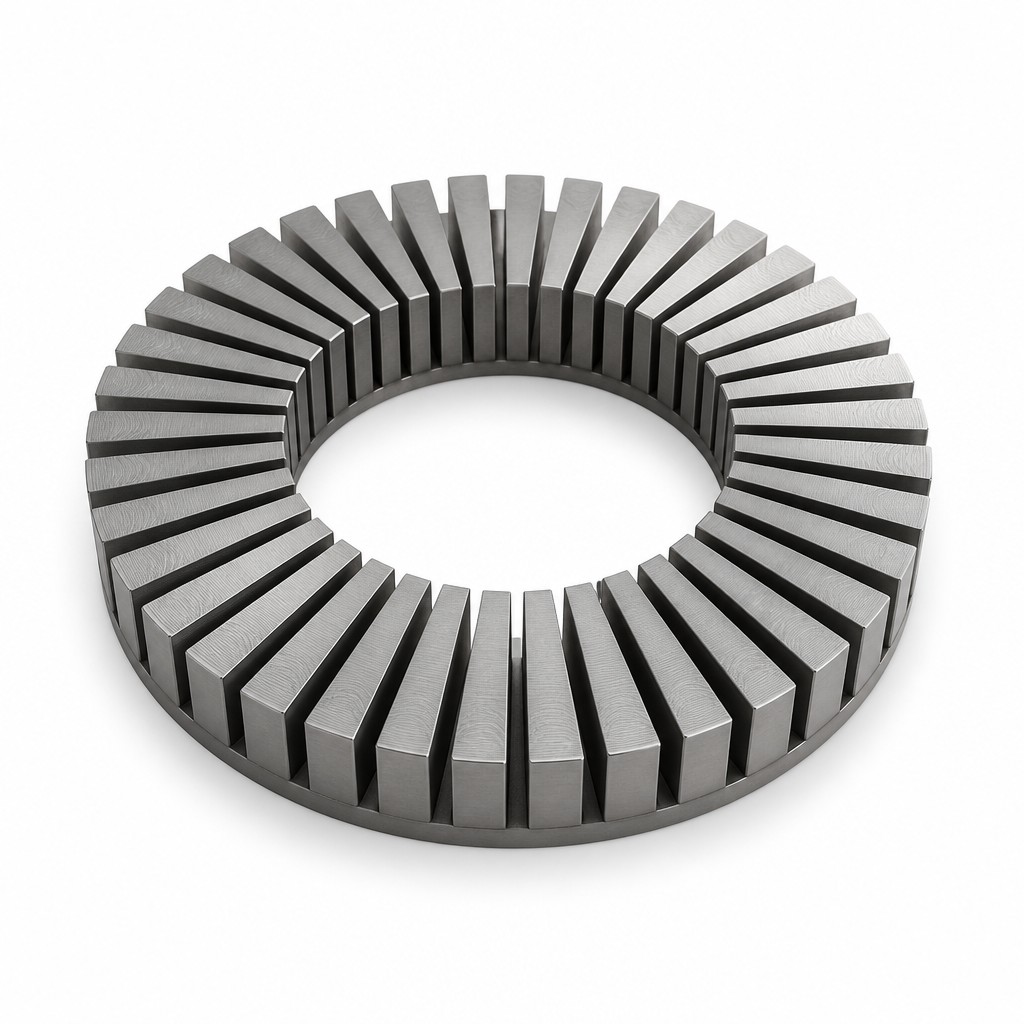
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
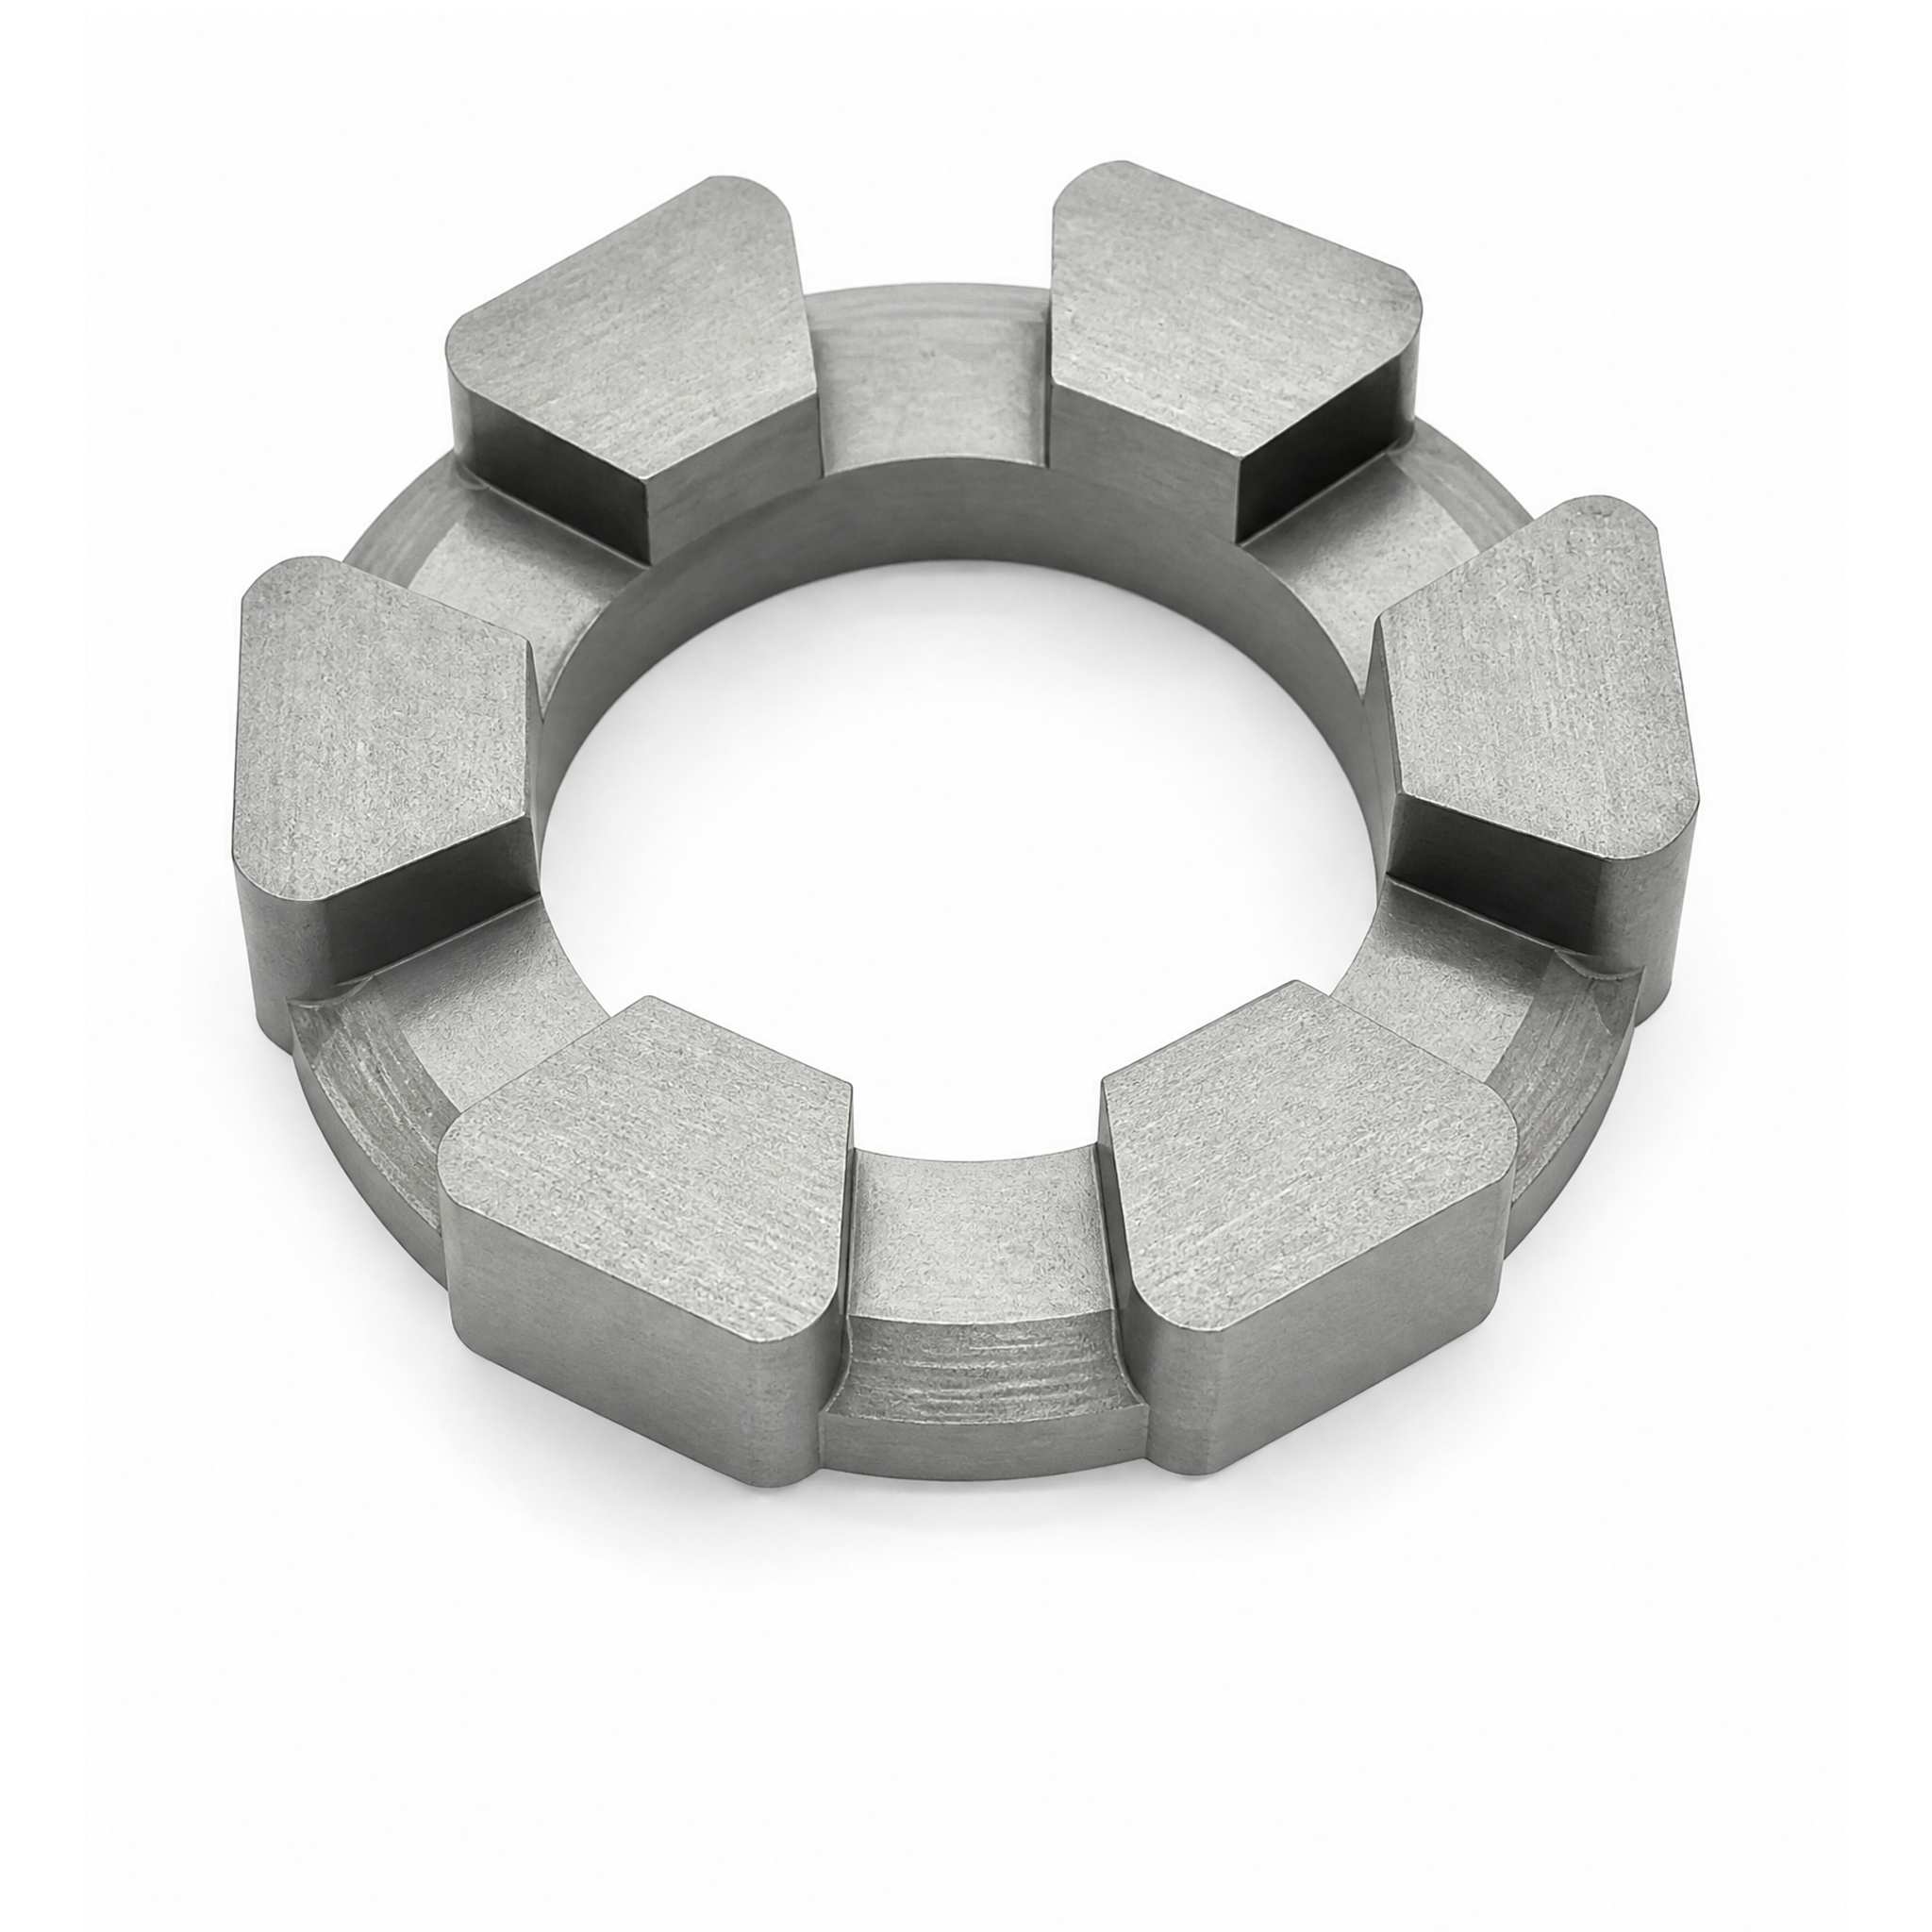
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
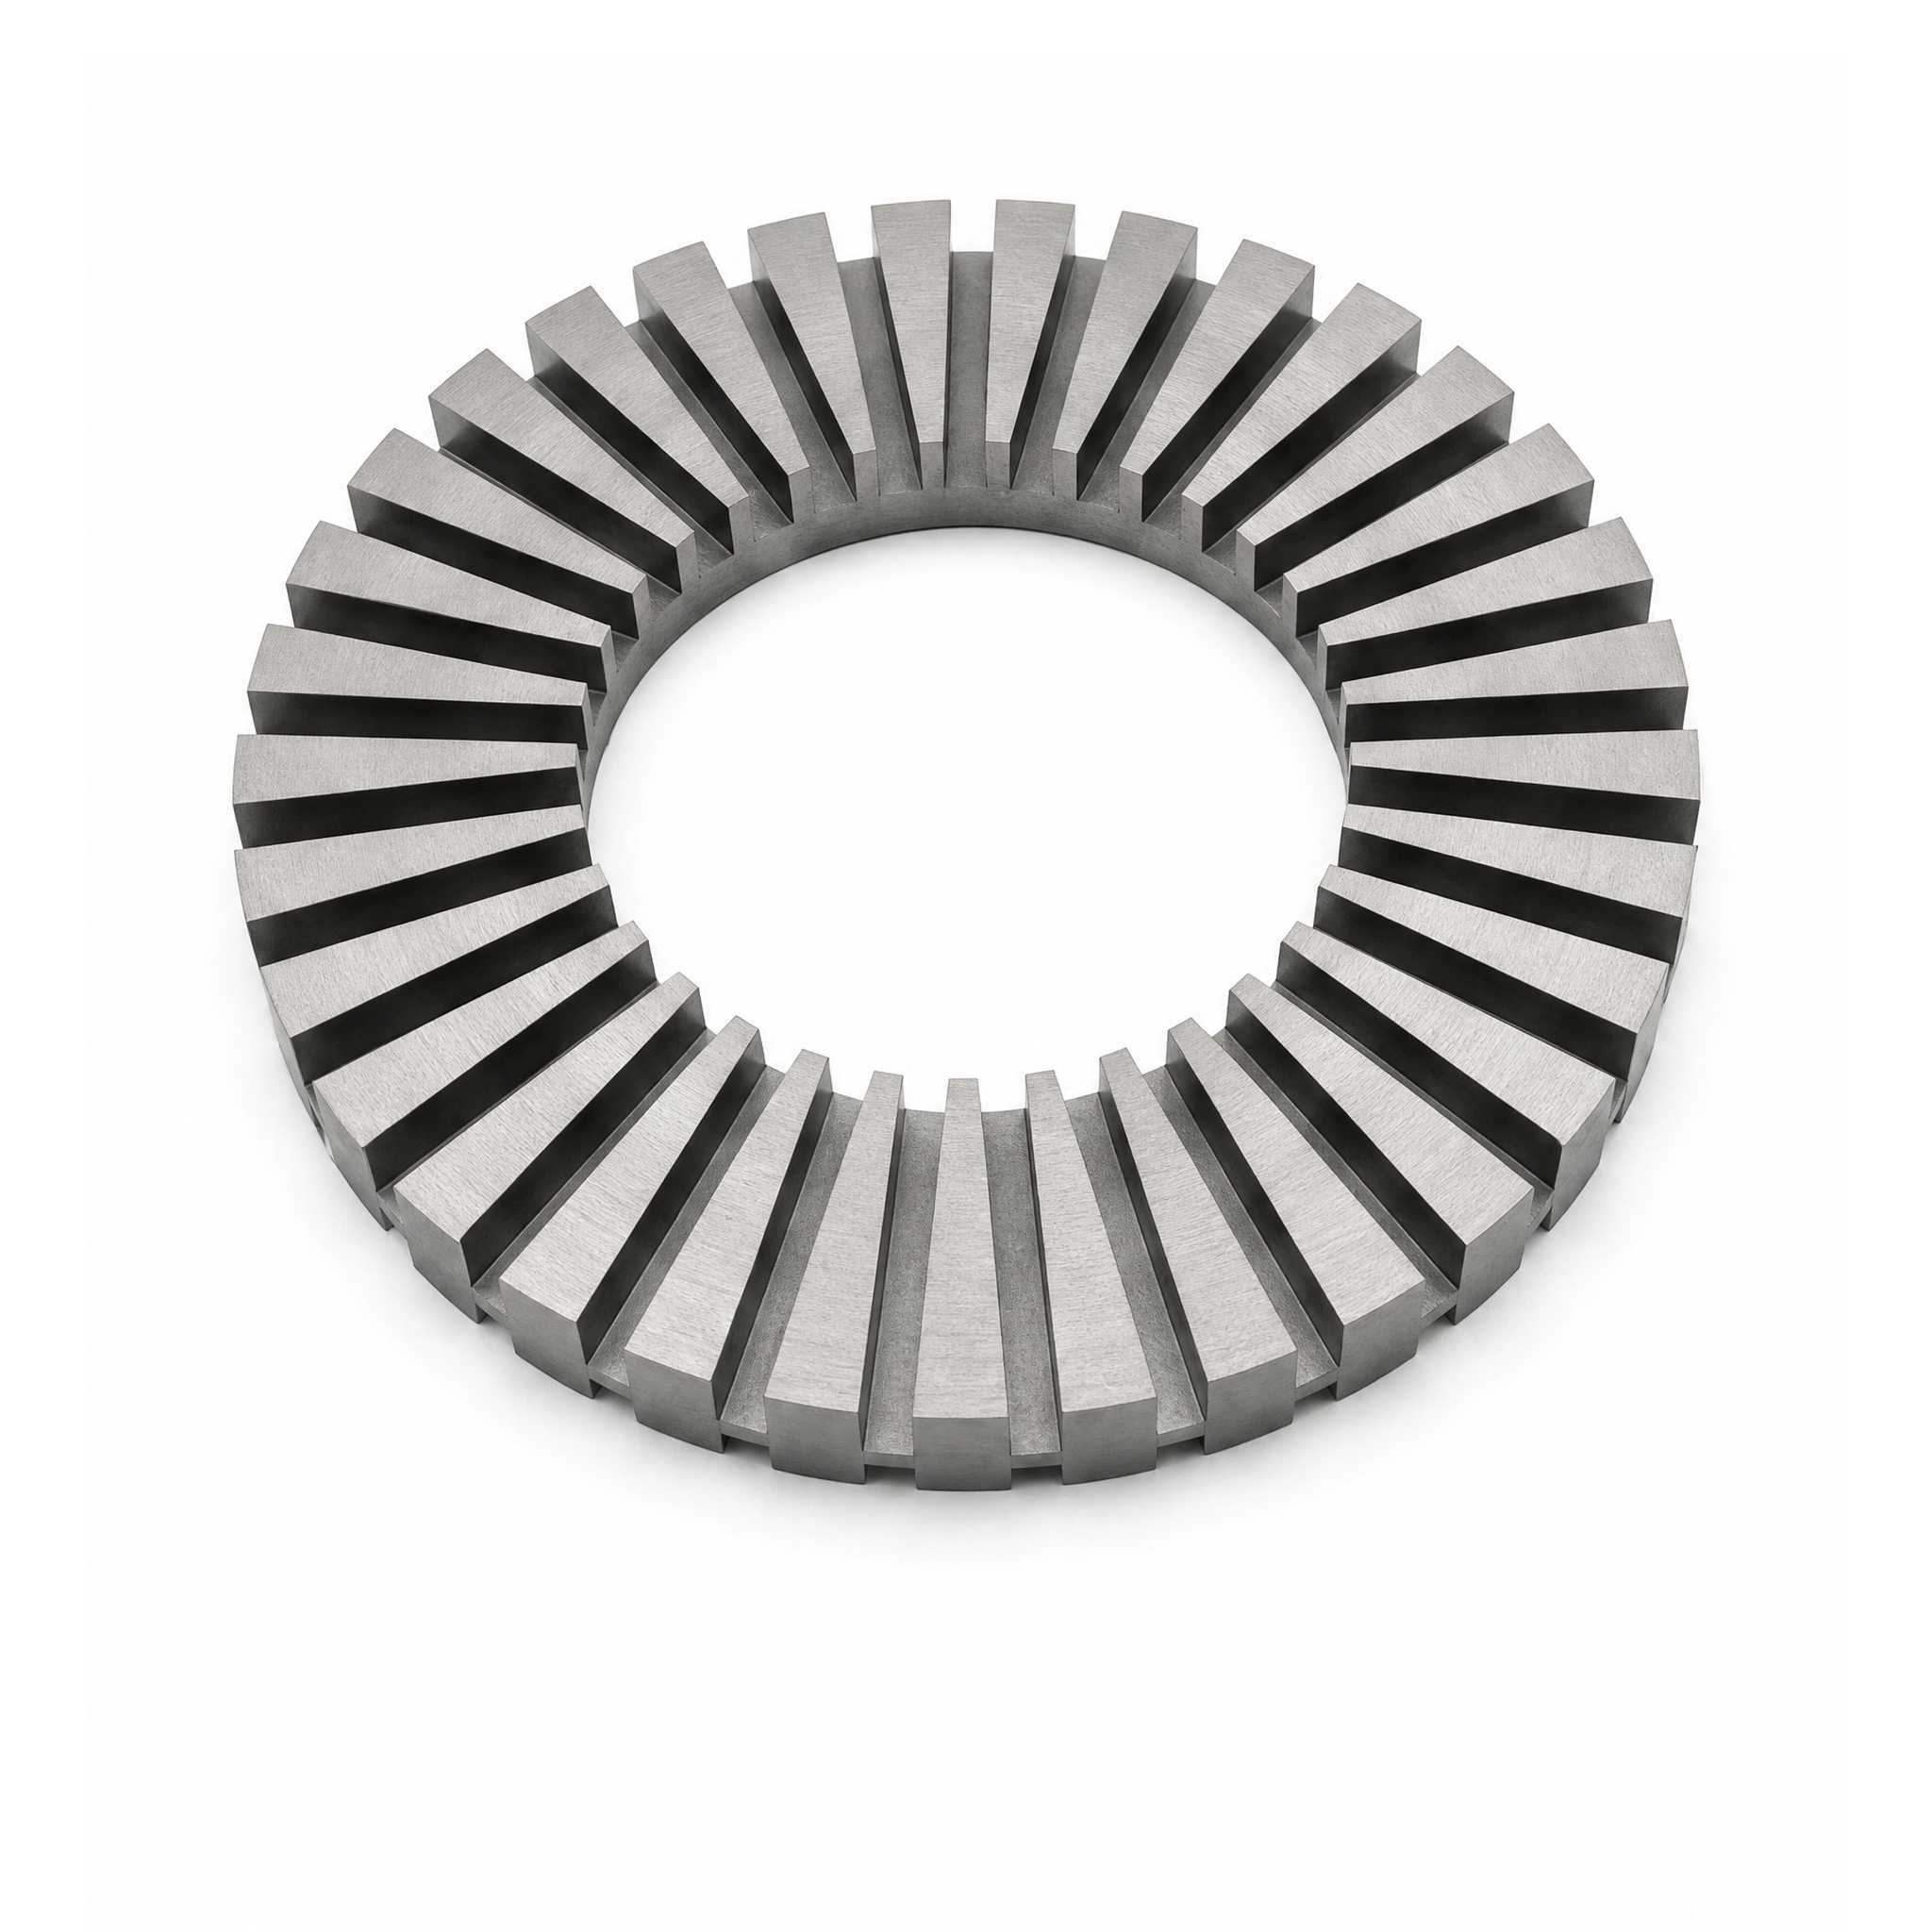
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
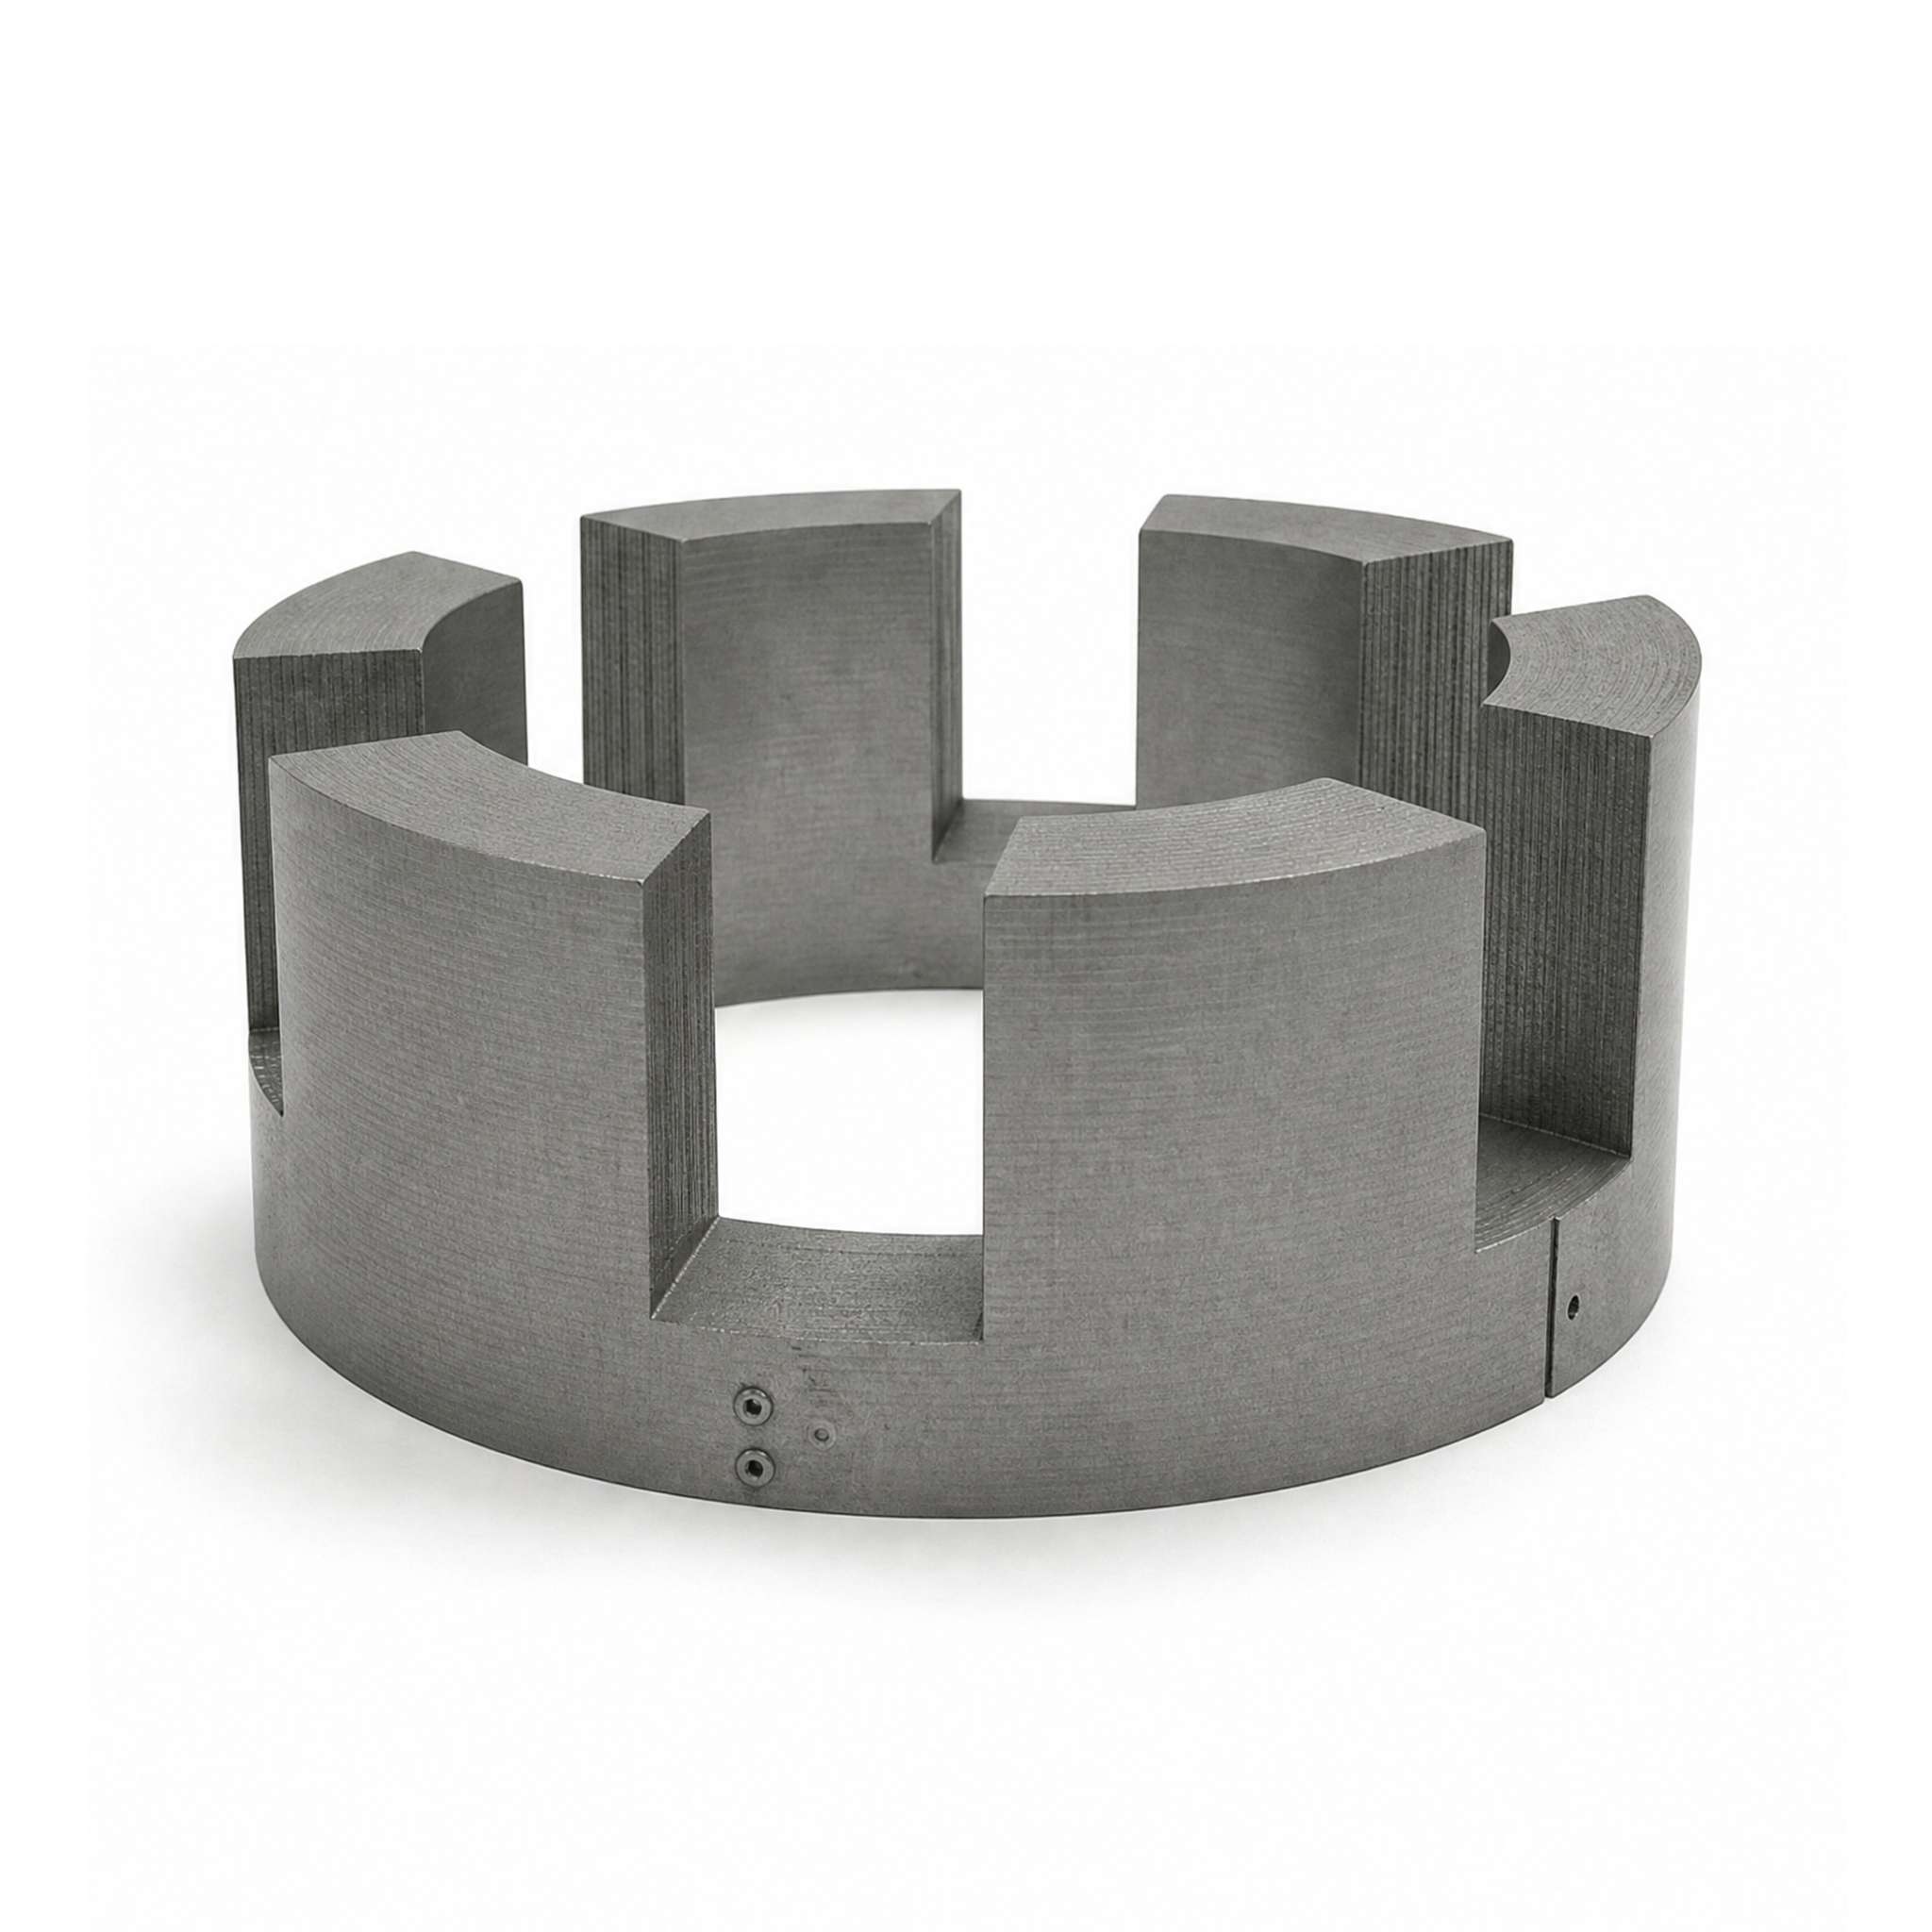
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
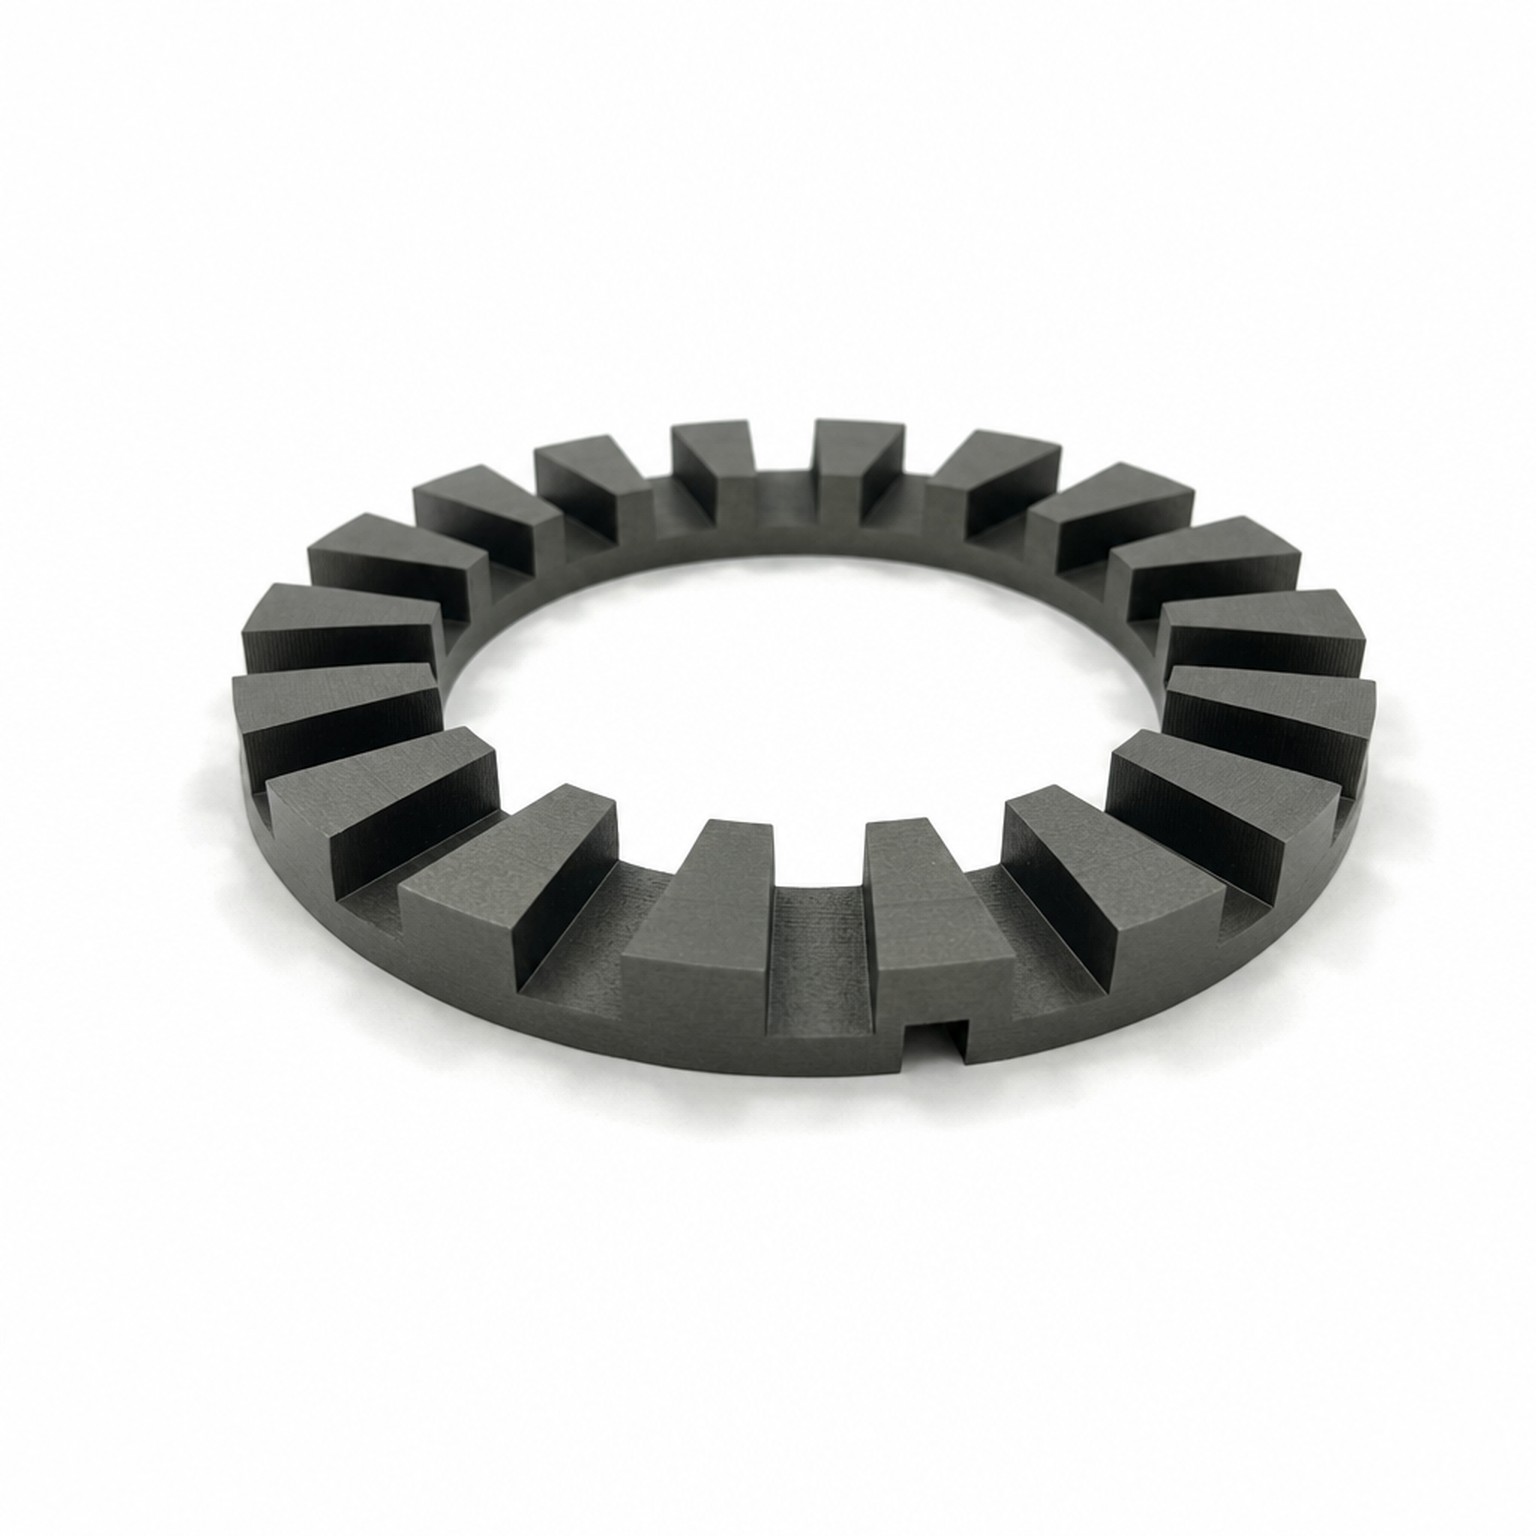
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
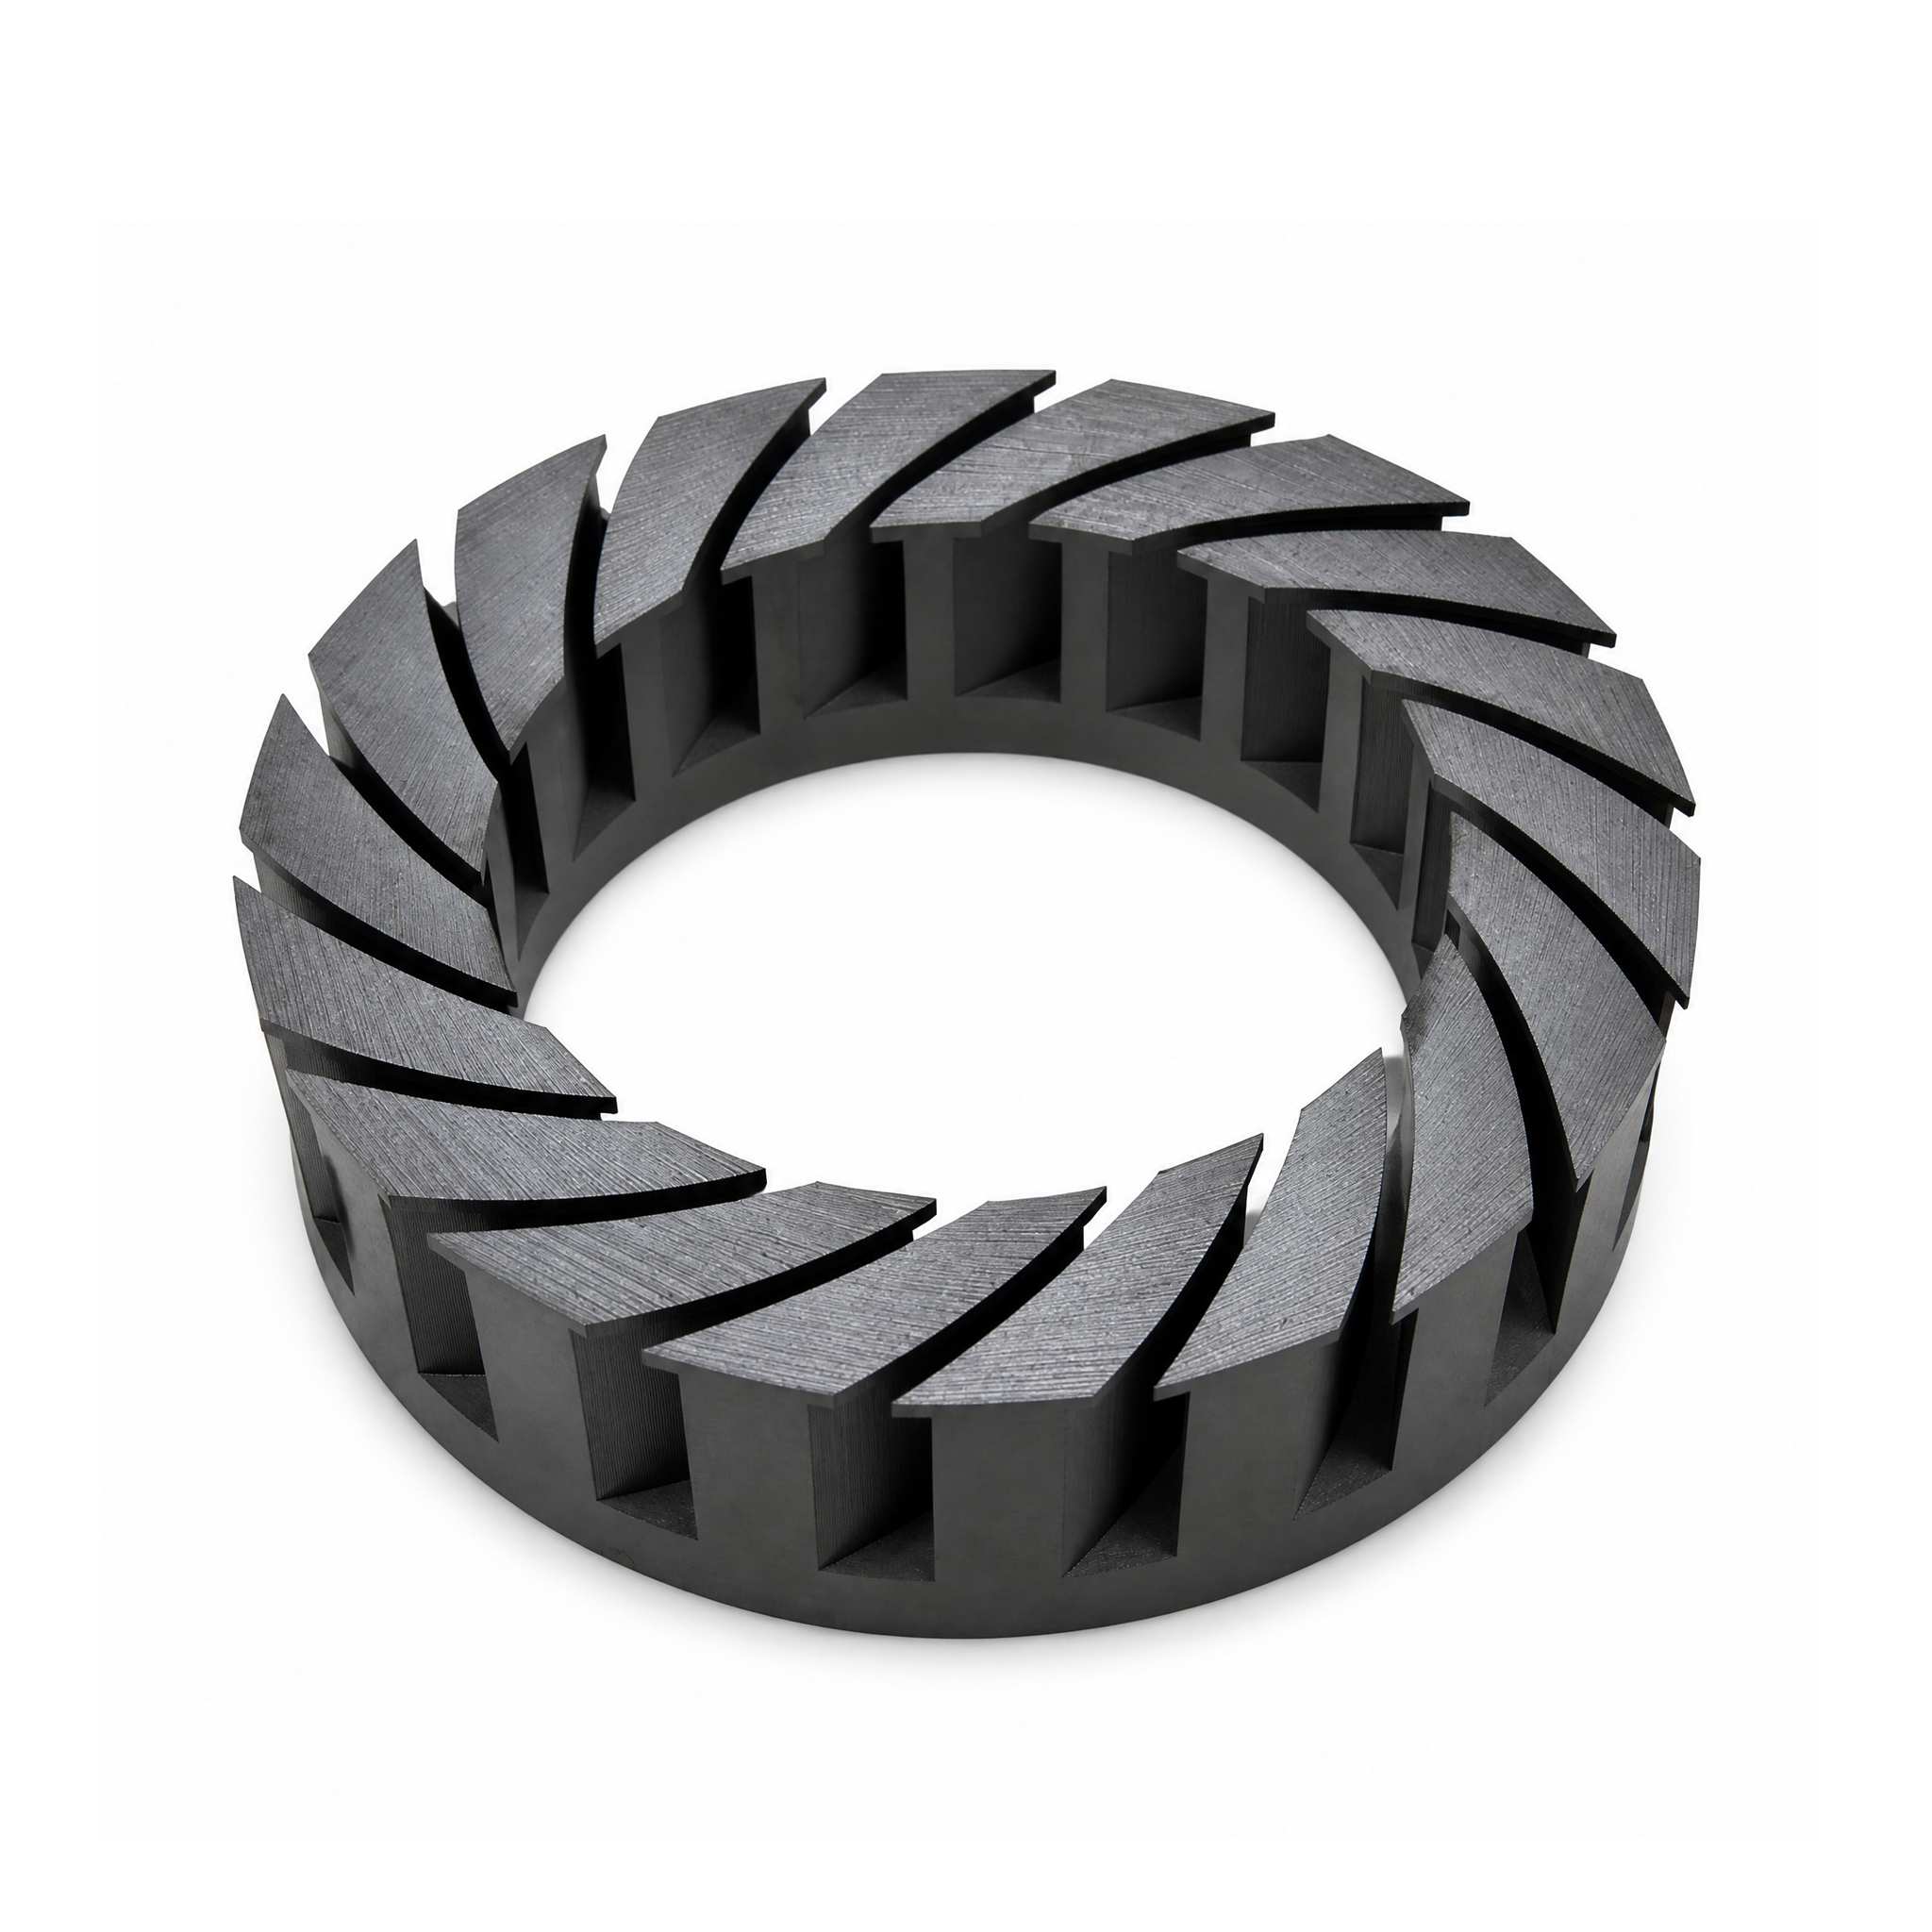
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
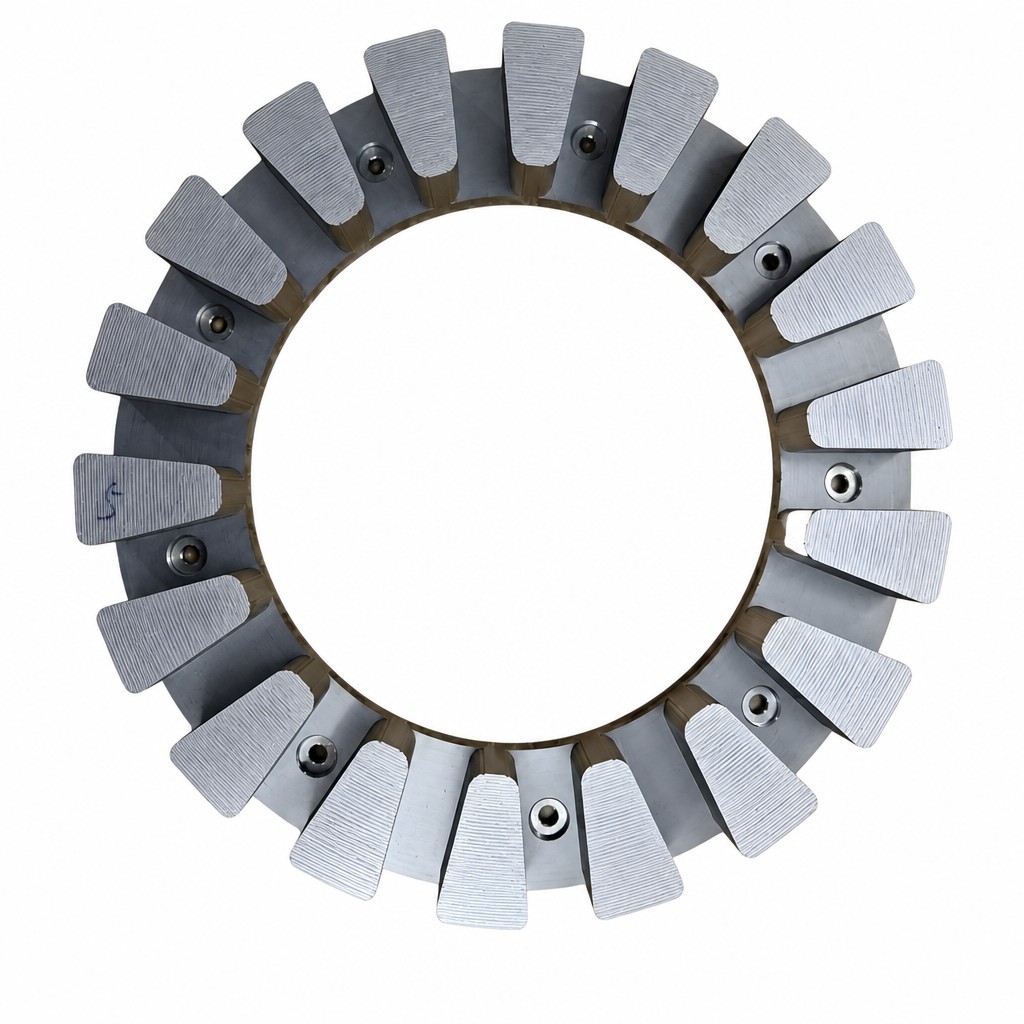
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
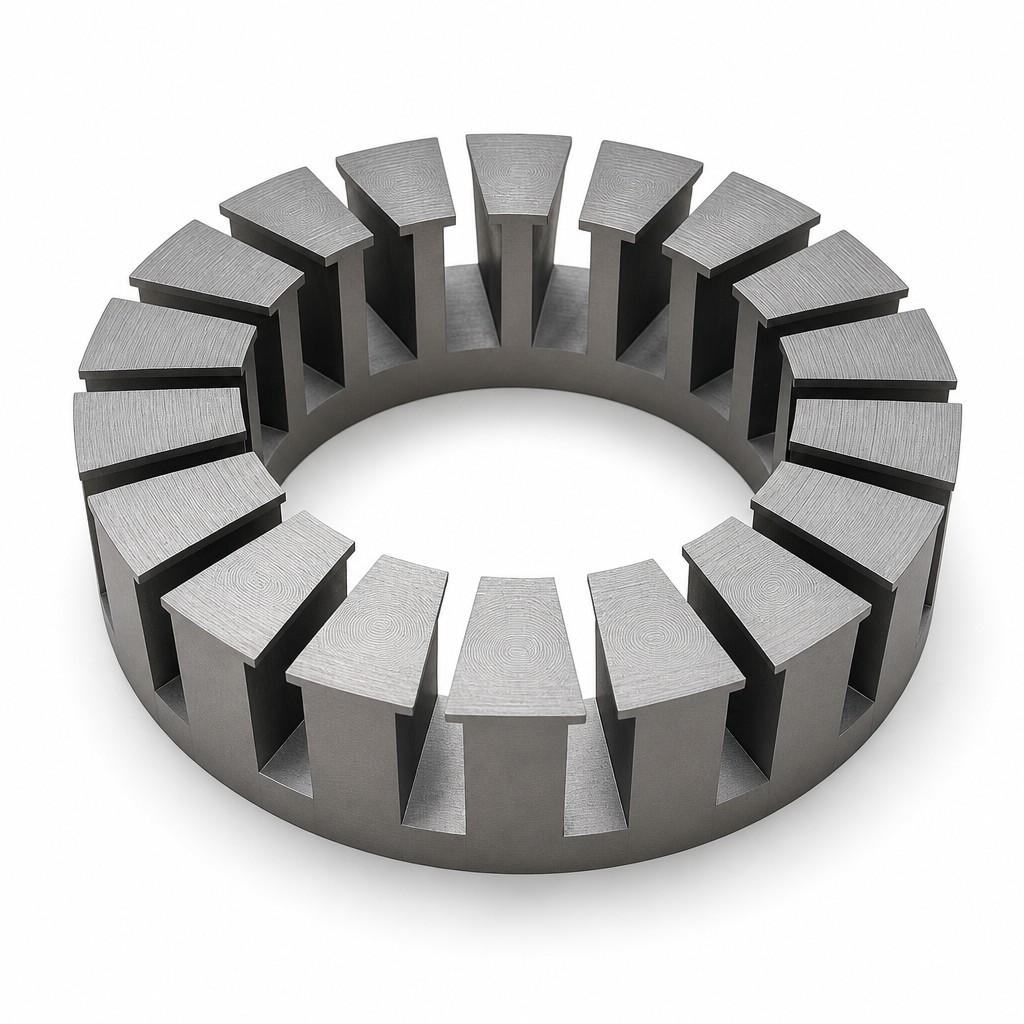
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
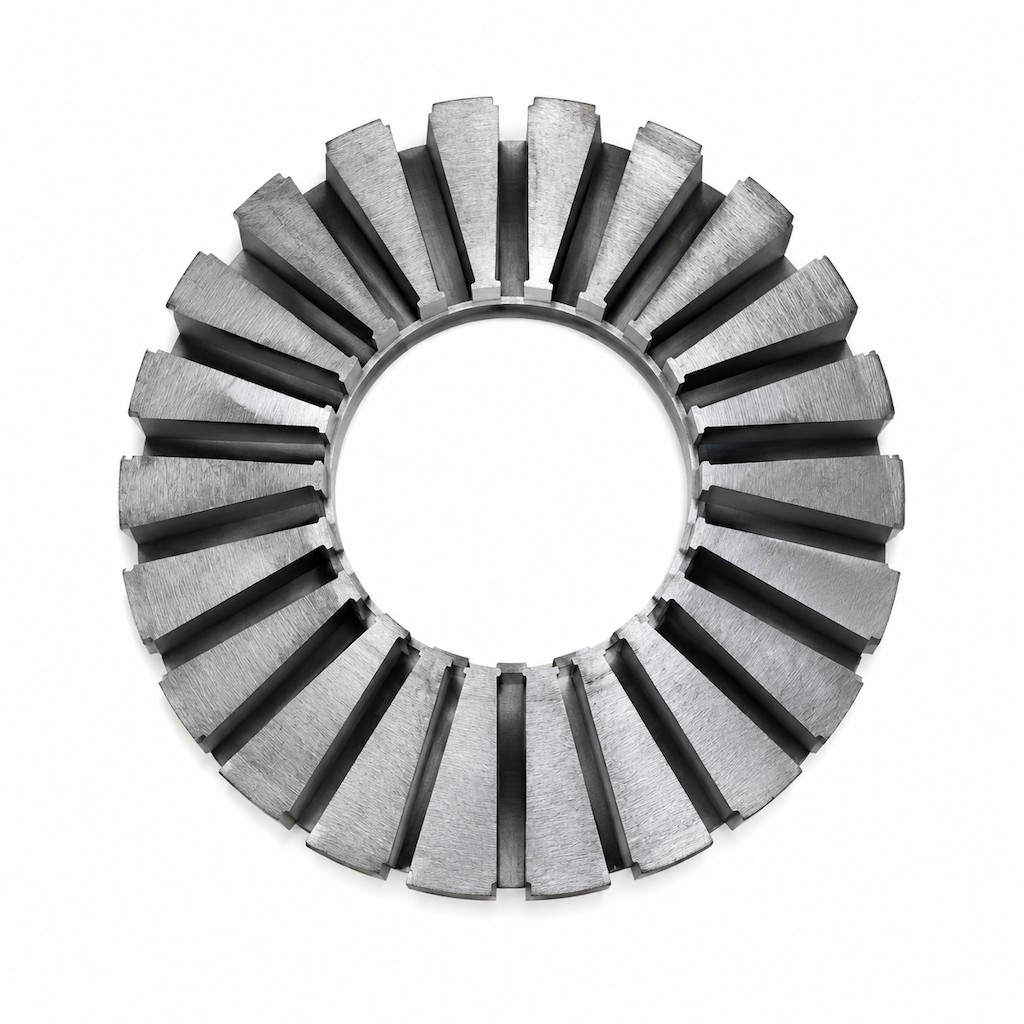
Custom wound axial flux stator cores engineered for in-wheel hub motors, electric motorcycles, e-bikes, and light electric vehicles (LEVs). Crafted from high-permeability electrical steel with precision laser-cut radial slots, delivering superior starting torque density, reduced unsprung wheel mass, excellent thermal dissipation, and zero tooling costs for customized hub dimensions.
Address : Room 201, West Building A, Dawei Logistics, Xihai Industrial Zone, Lecong Town, Shunde District, Foshan City
You may unsubscribe at any moment. For that purpose, please find our contact info in the legal notice.


 IPv6 network supported
We will contact you as soon as possible
Hi! Click one of our members below to chat on