 en
 fr
 es
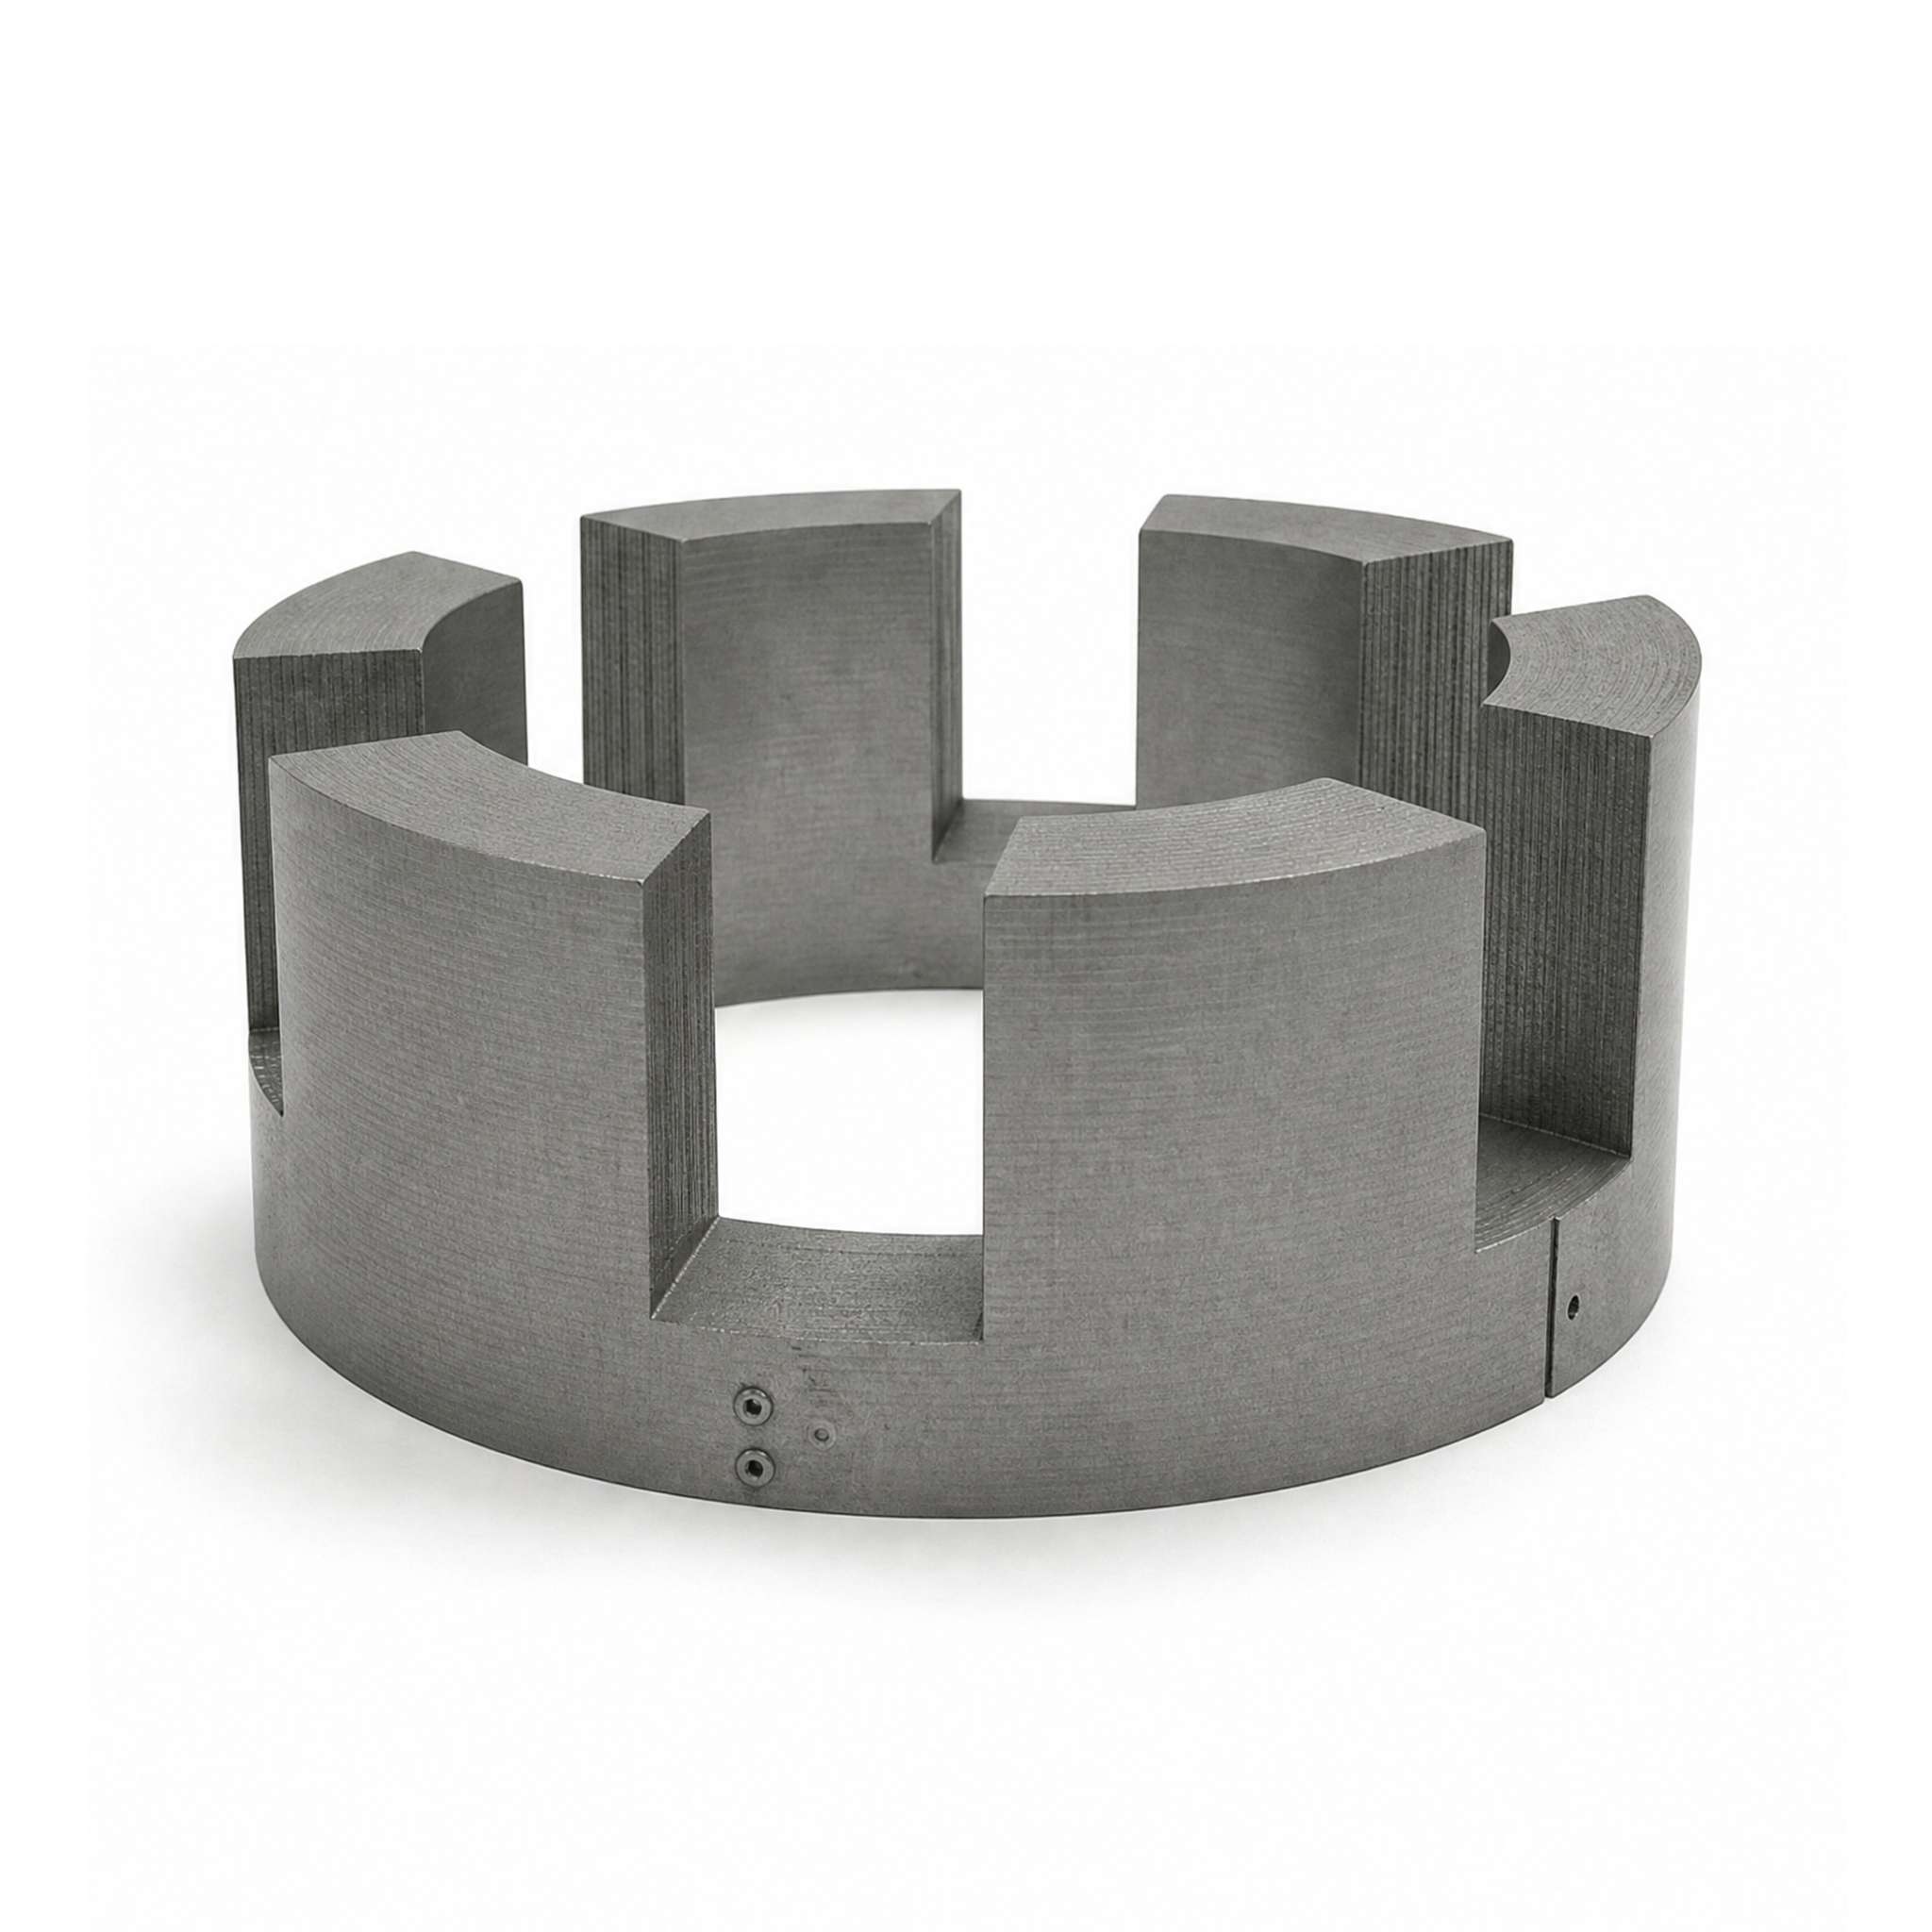
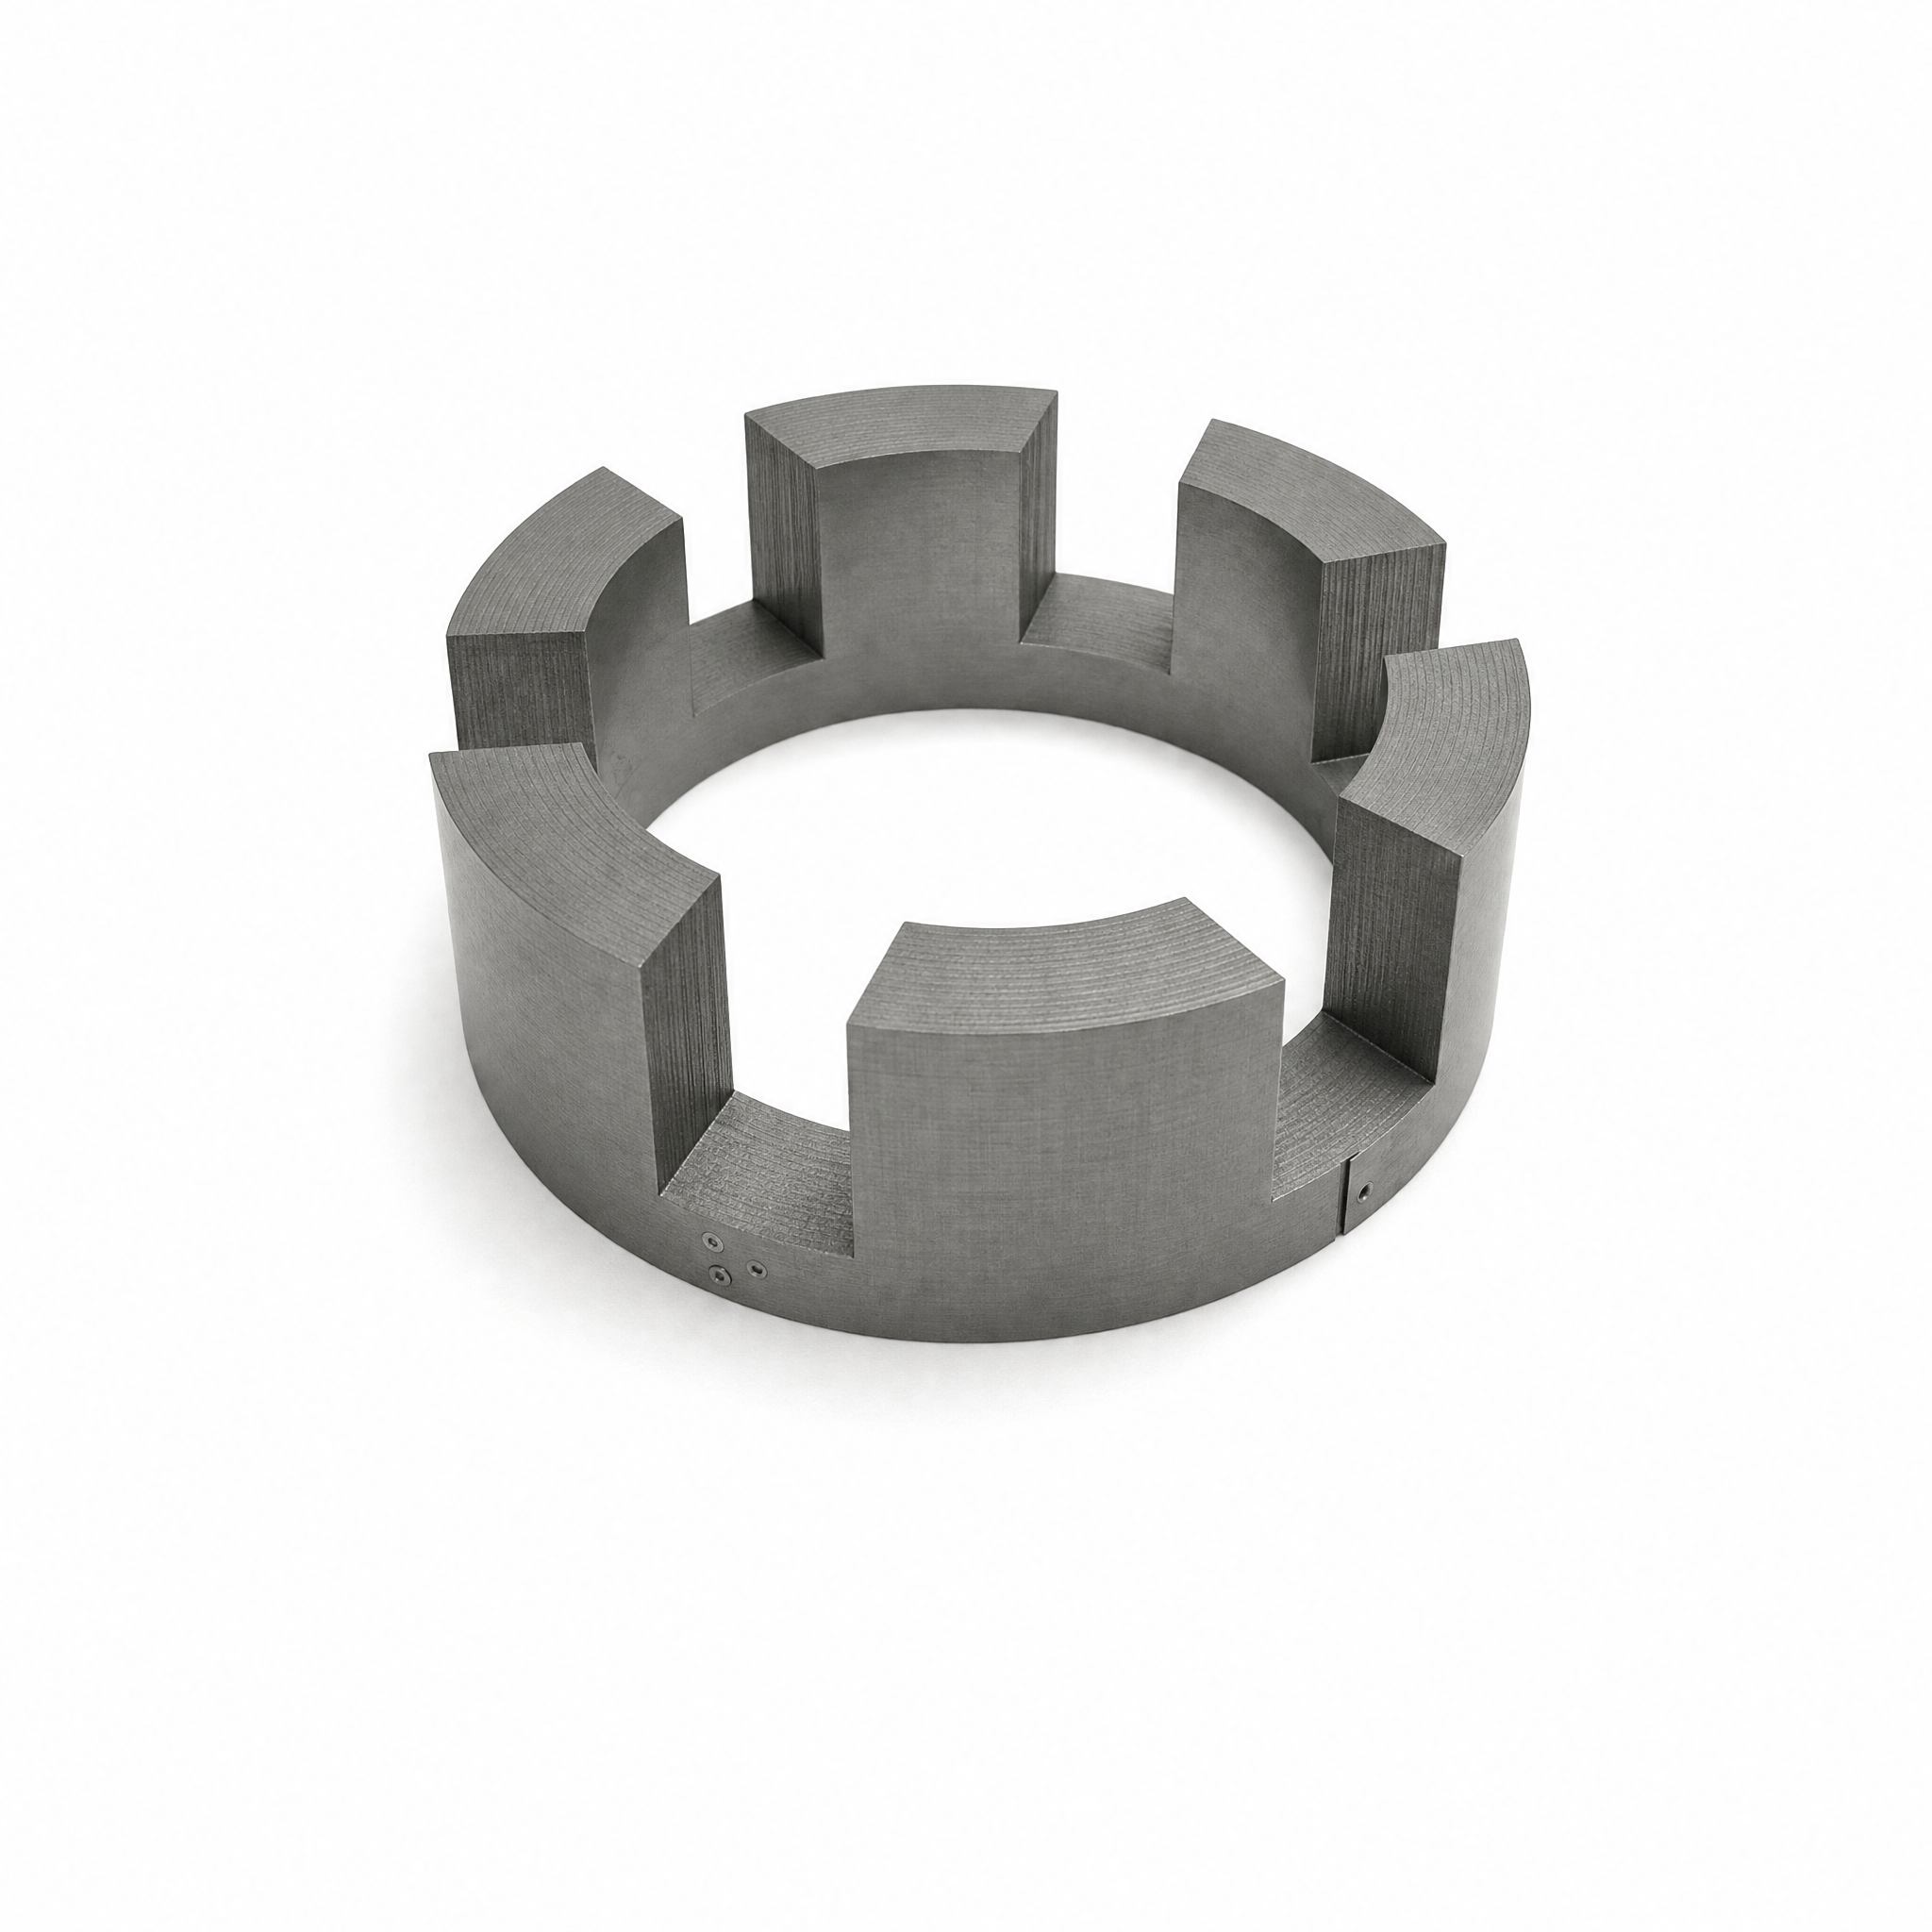
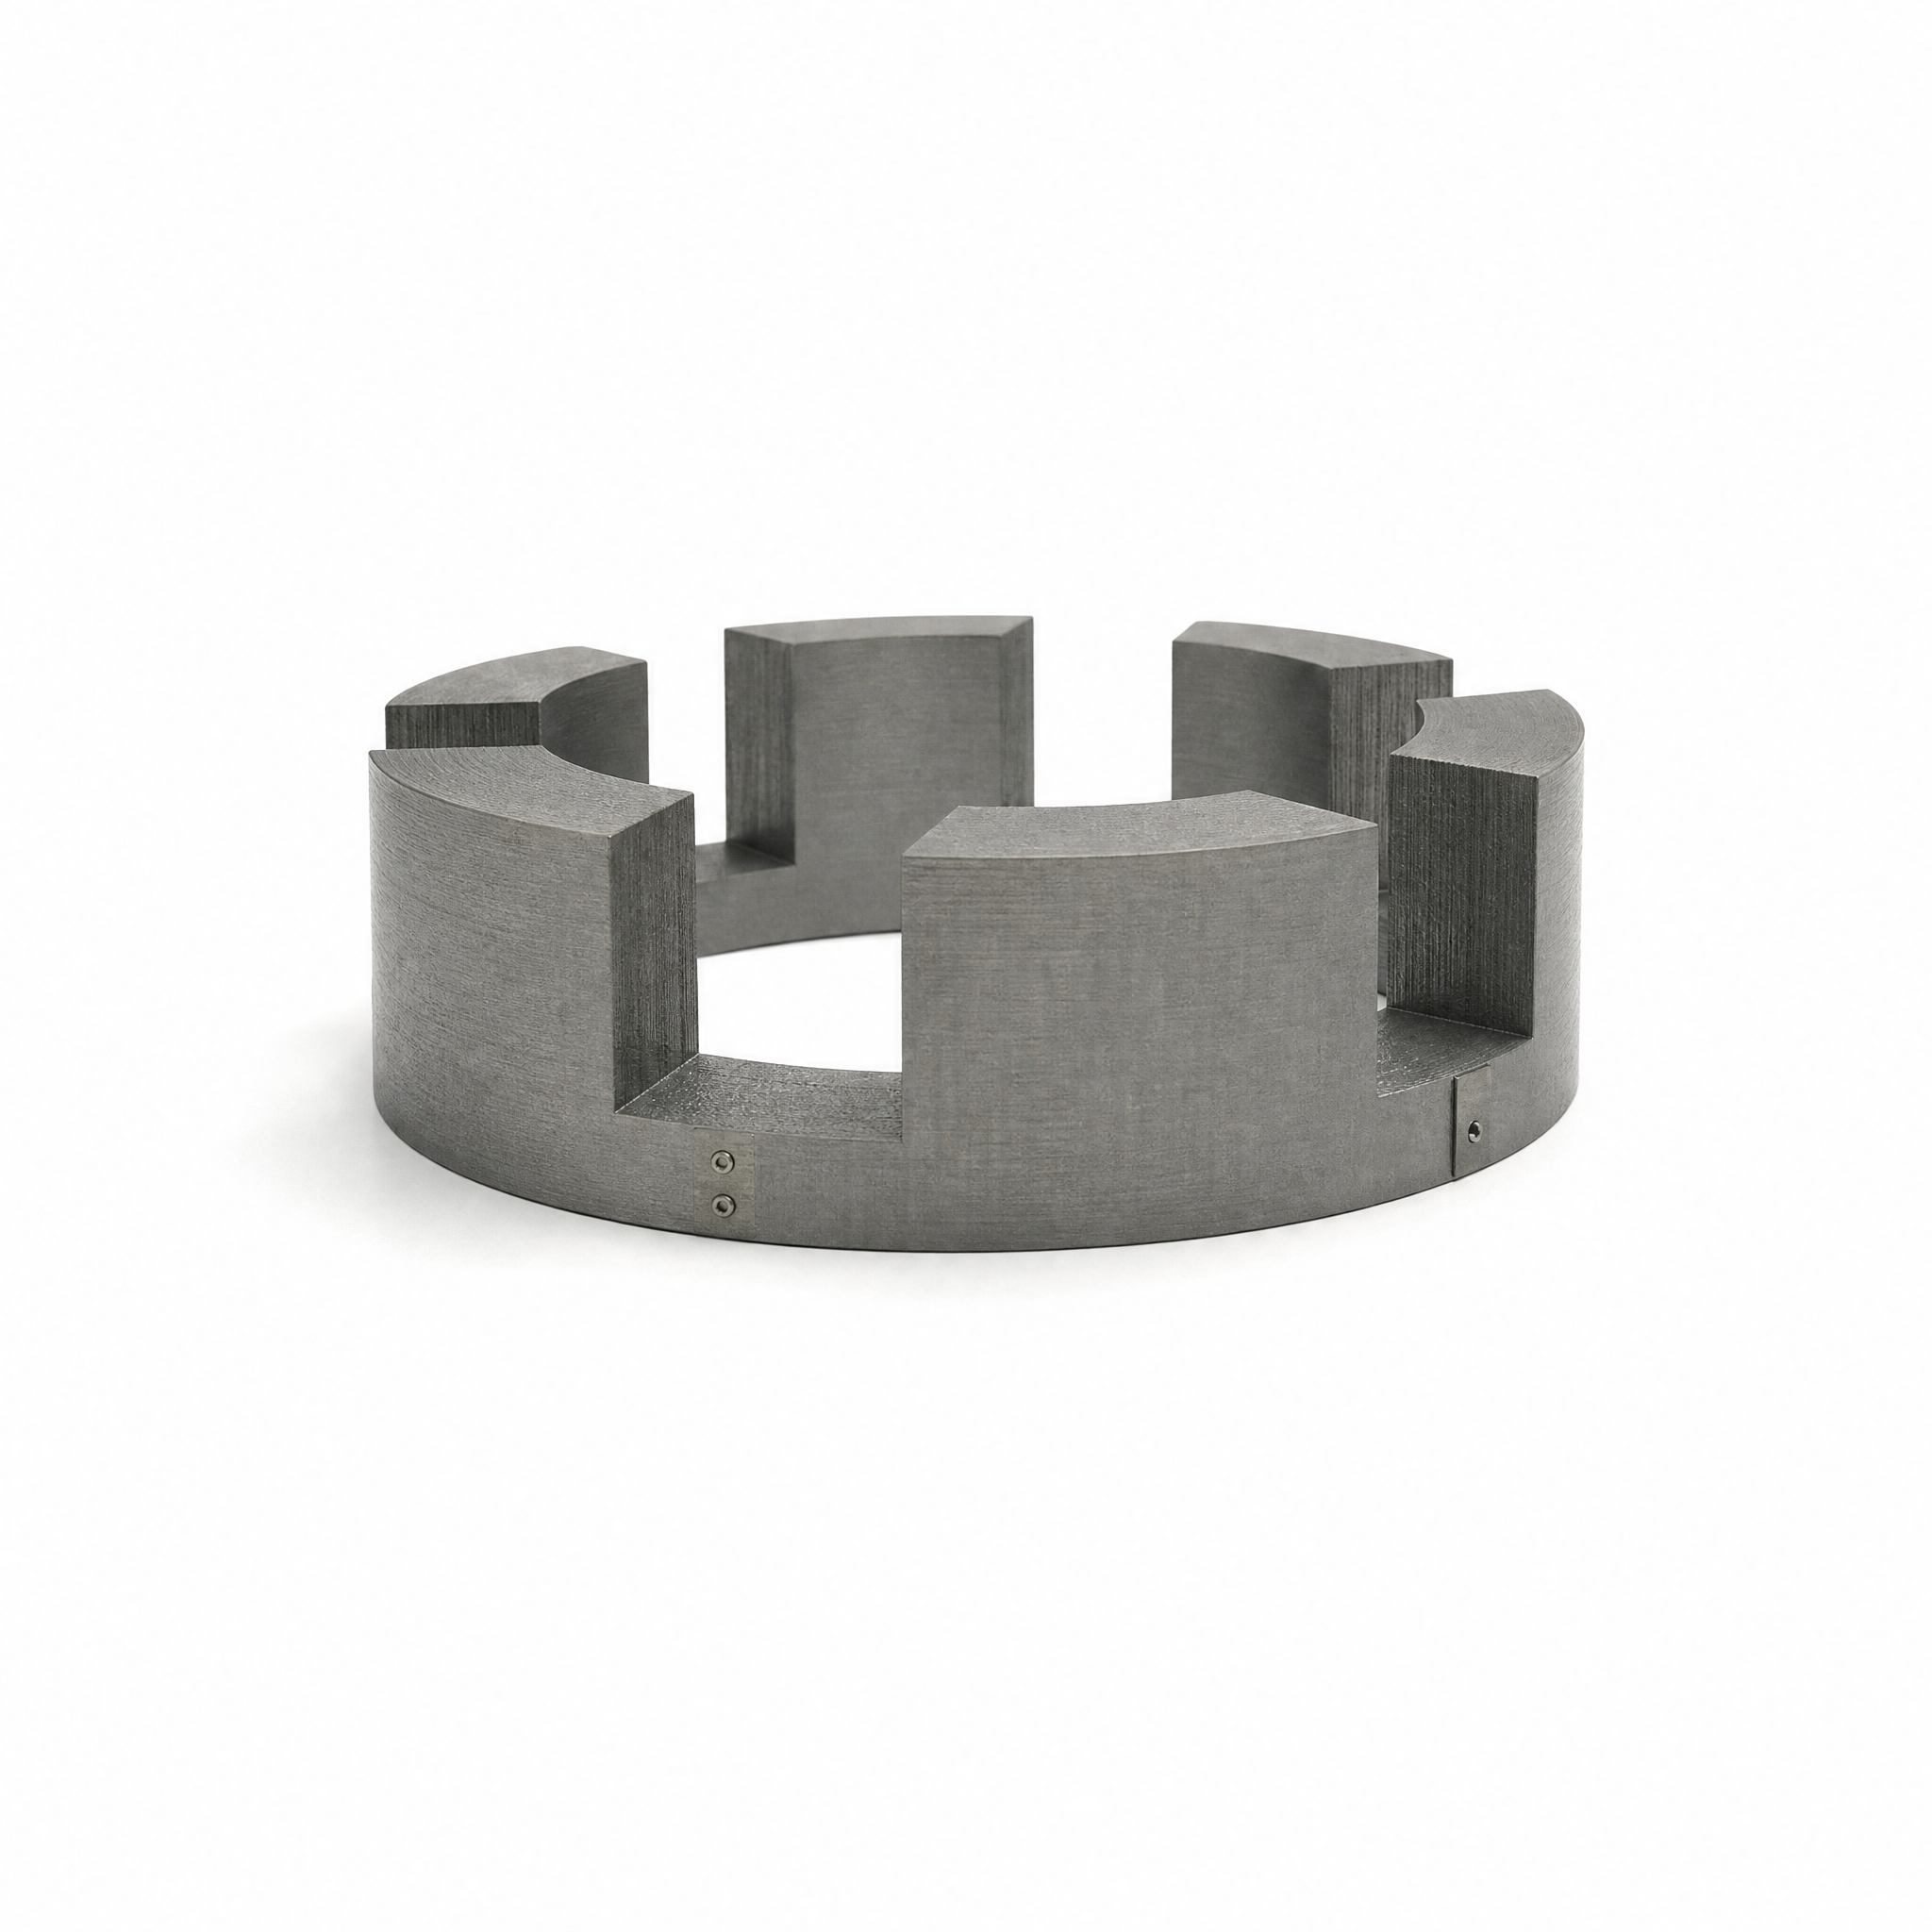
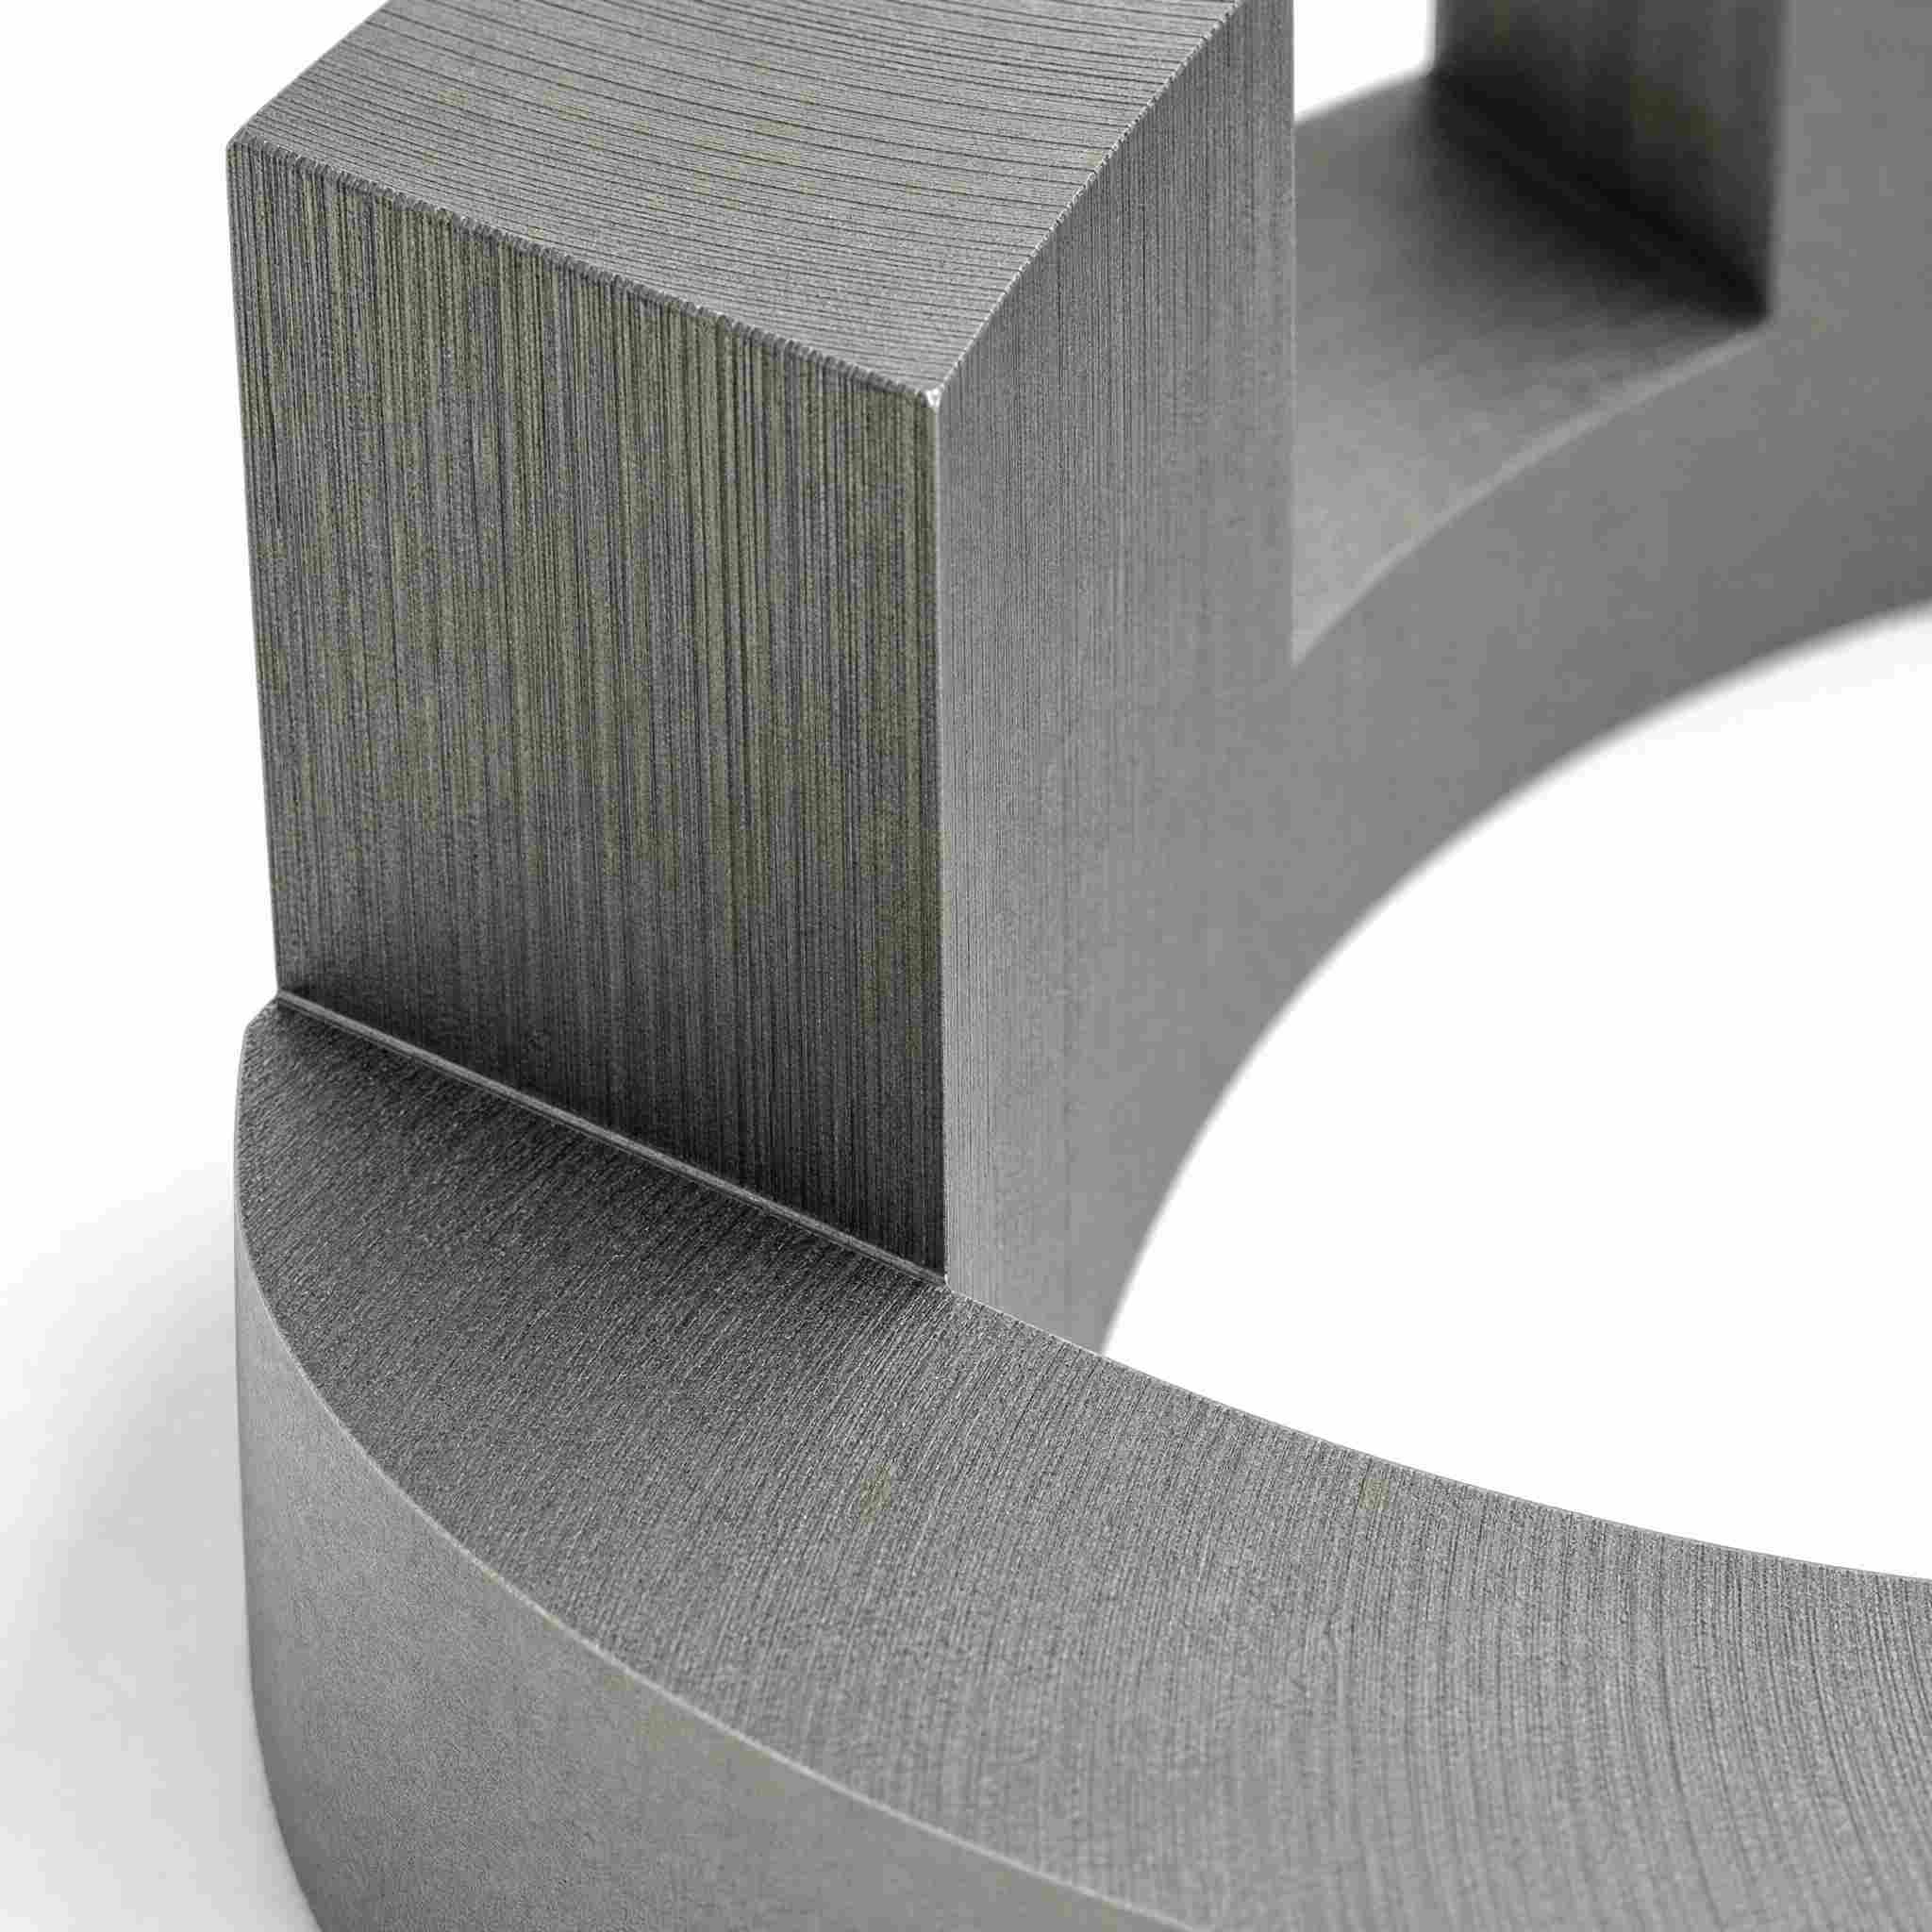
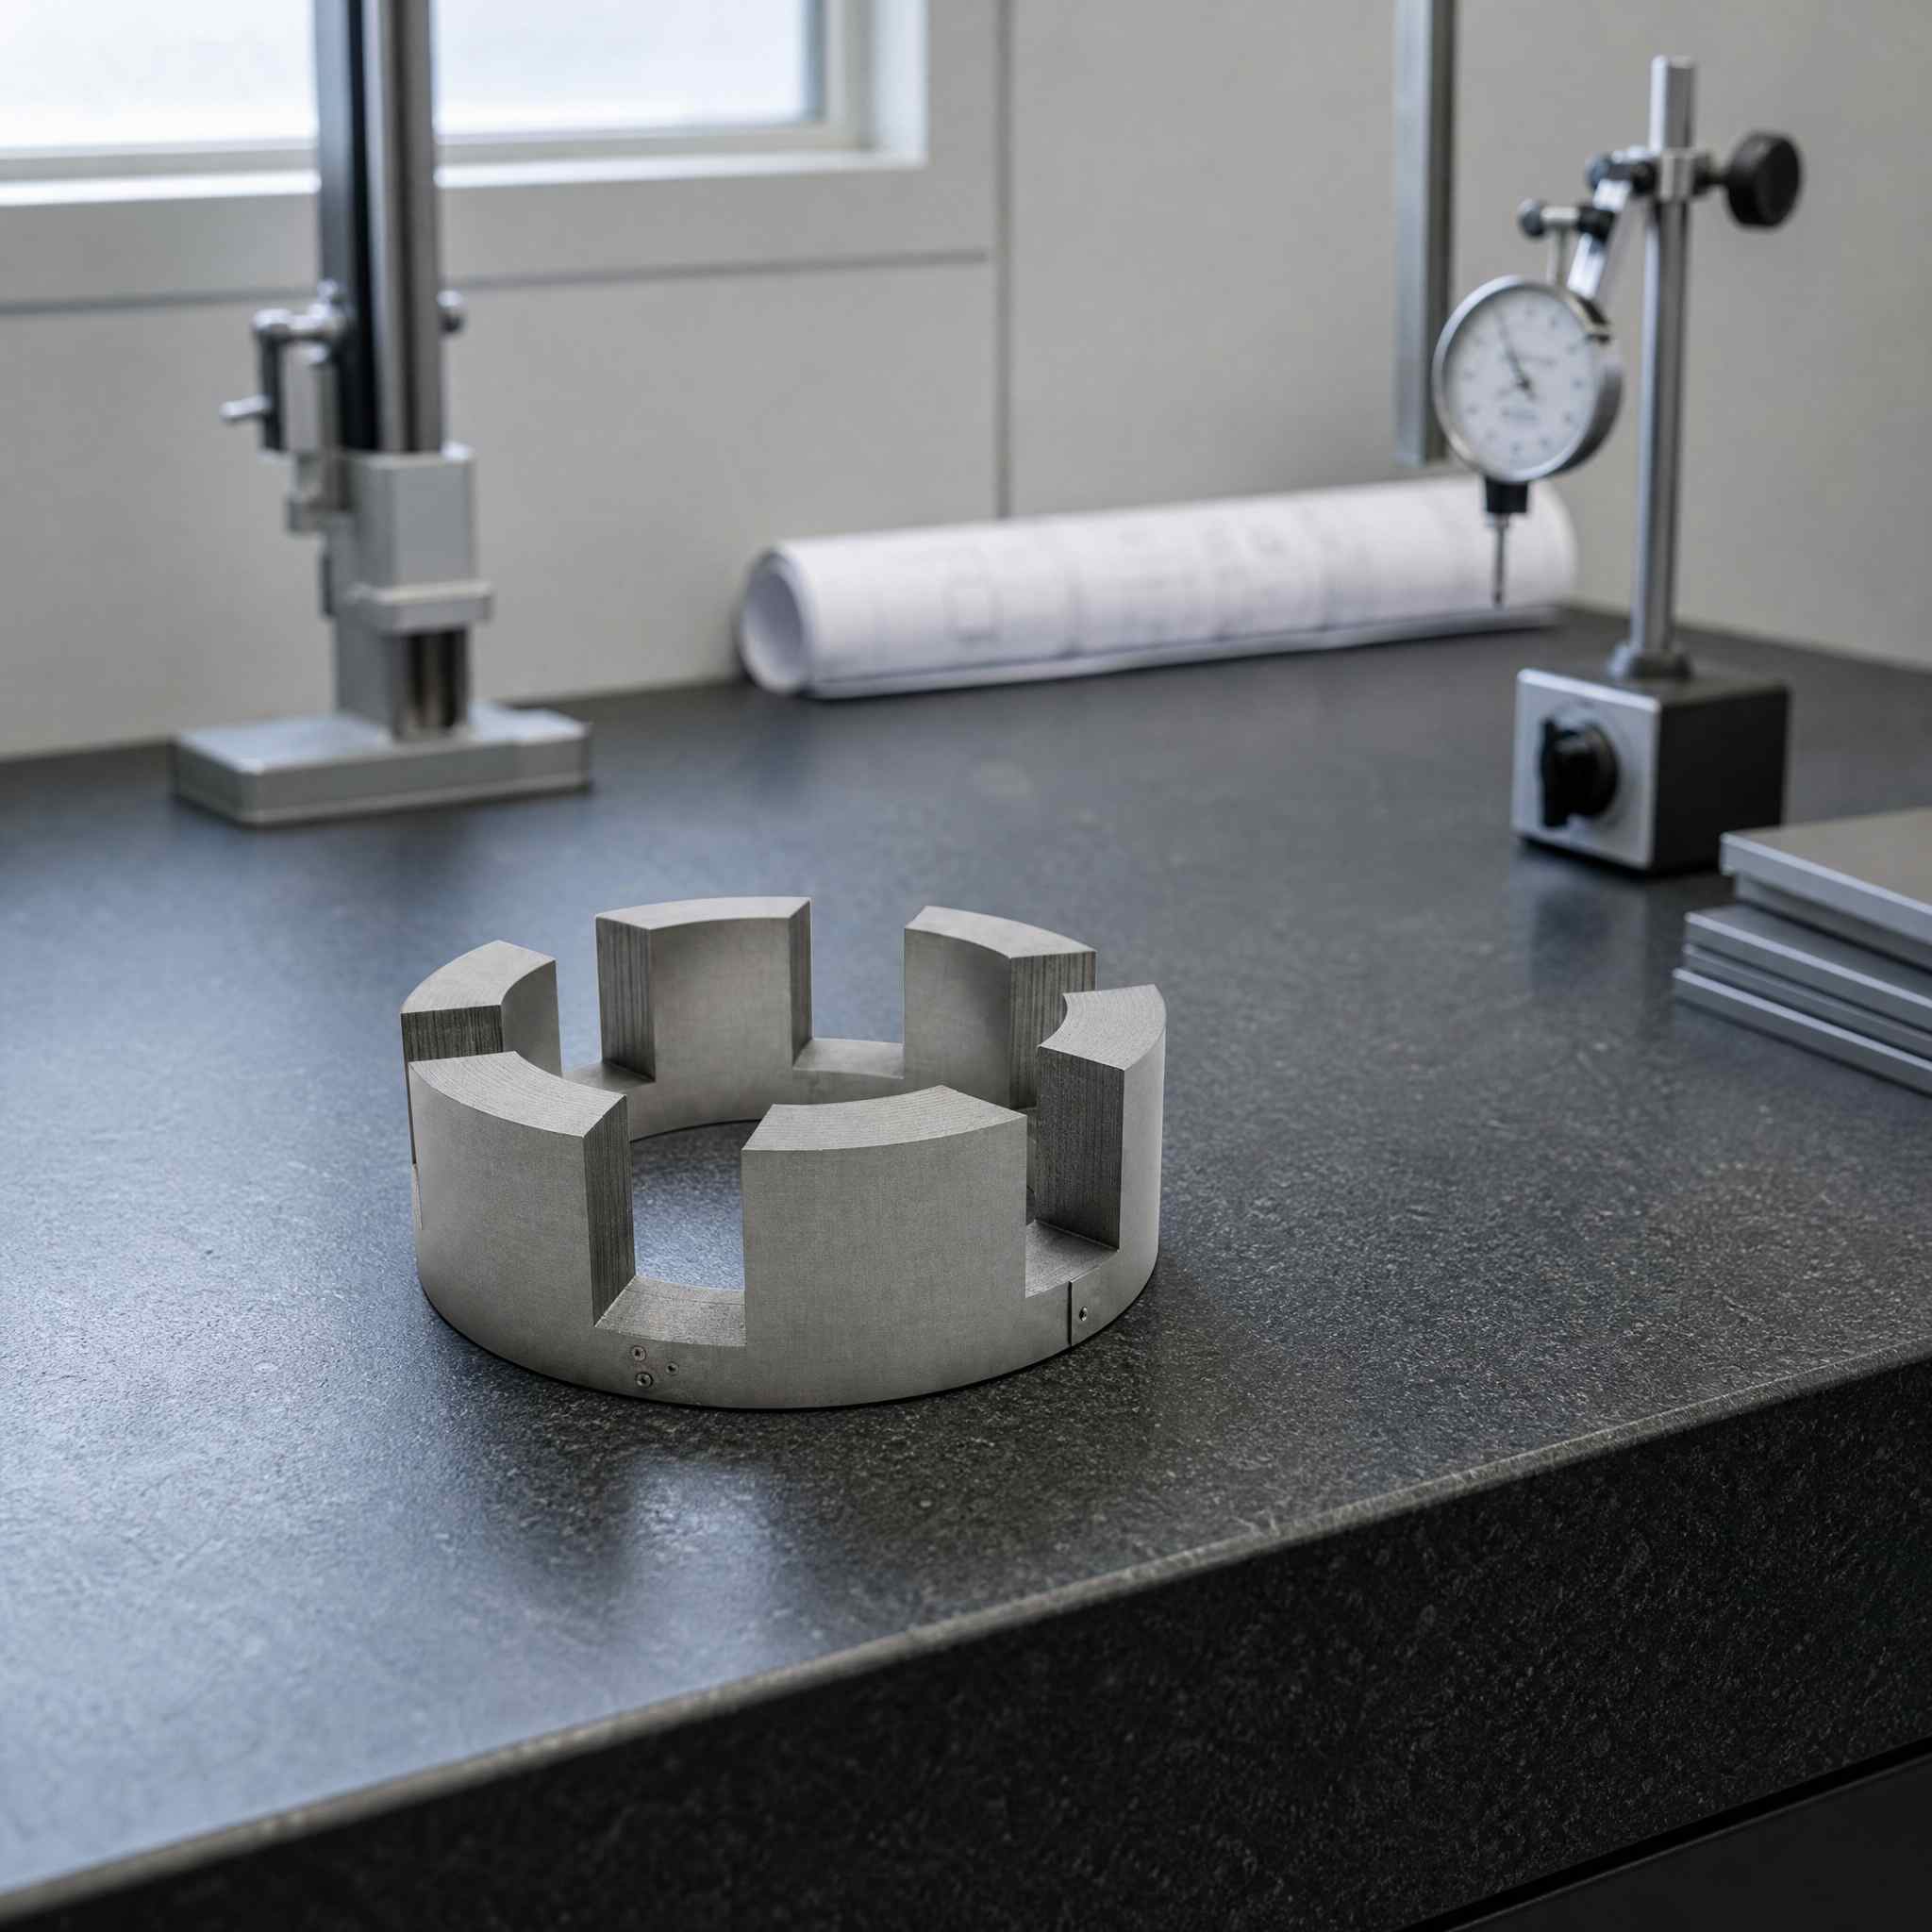
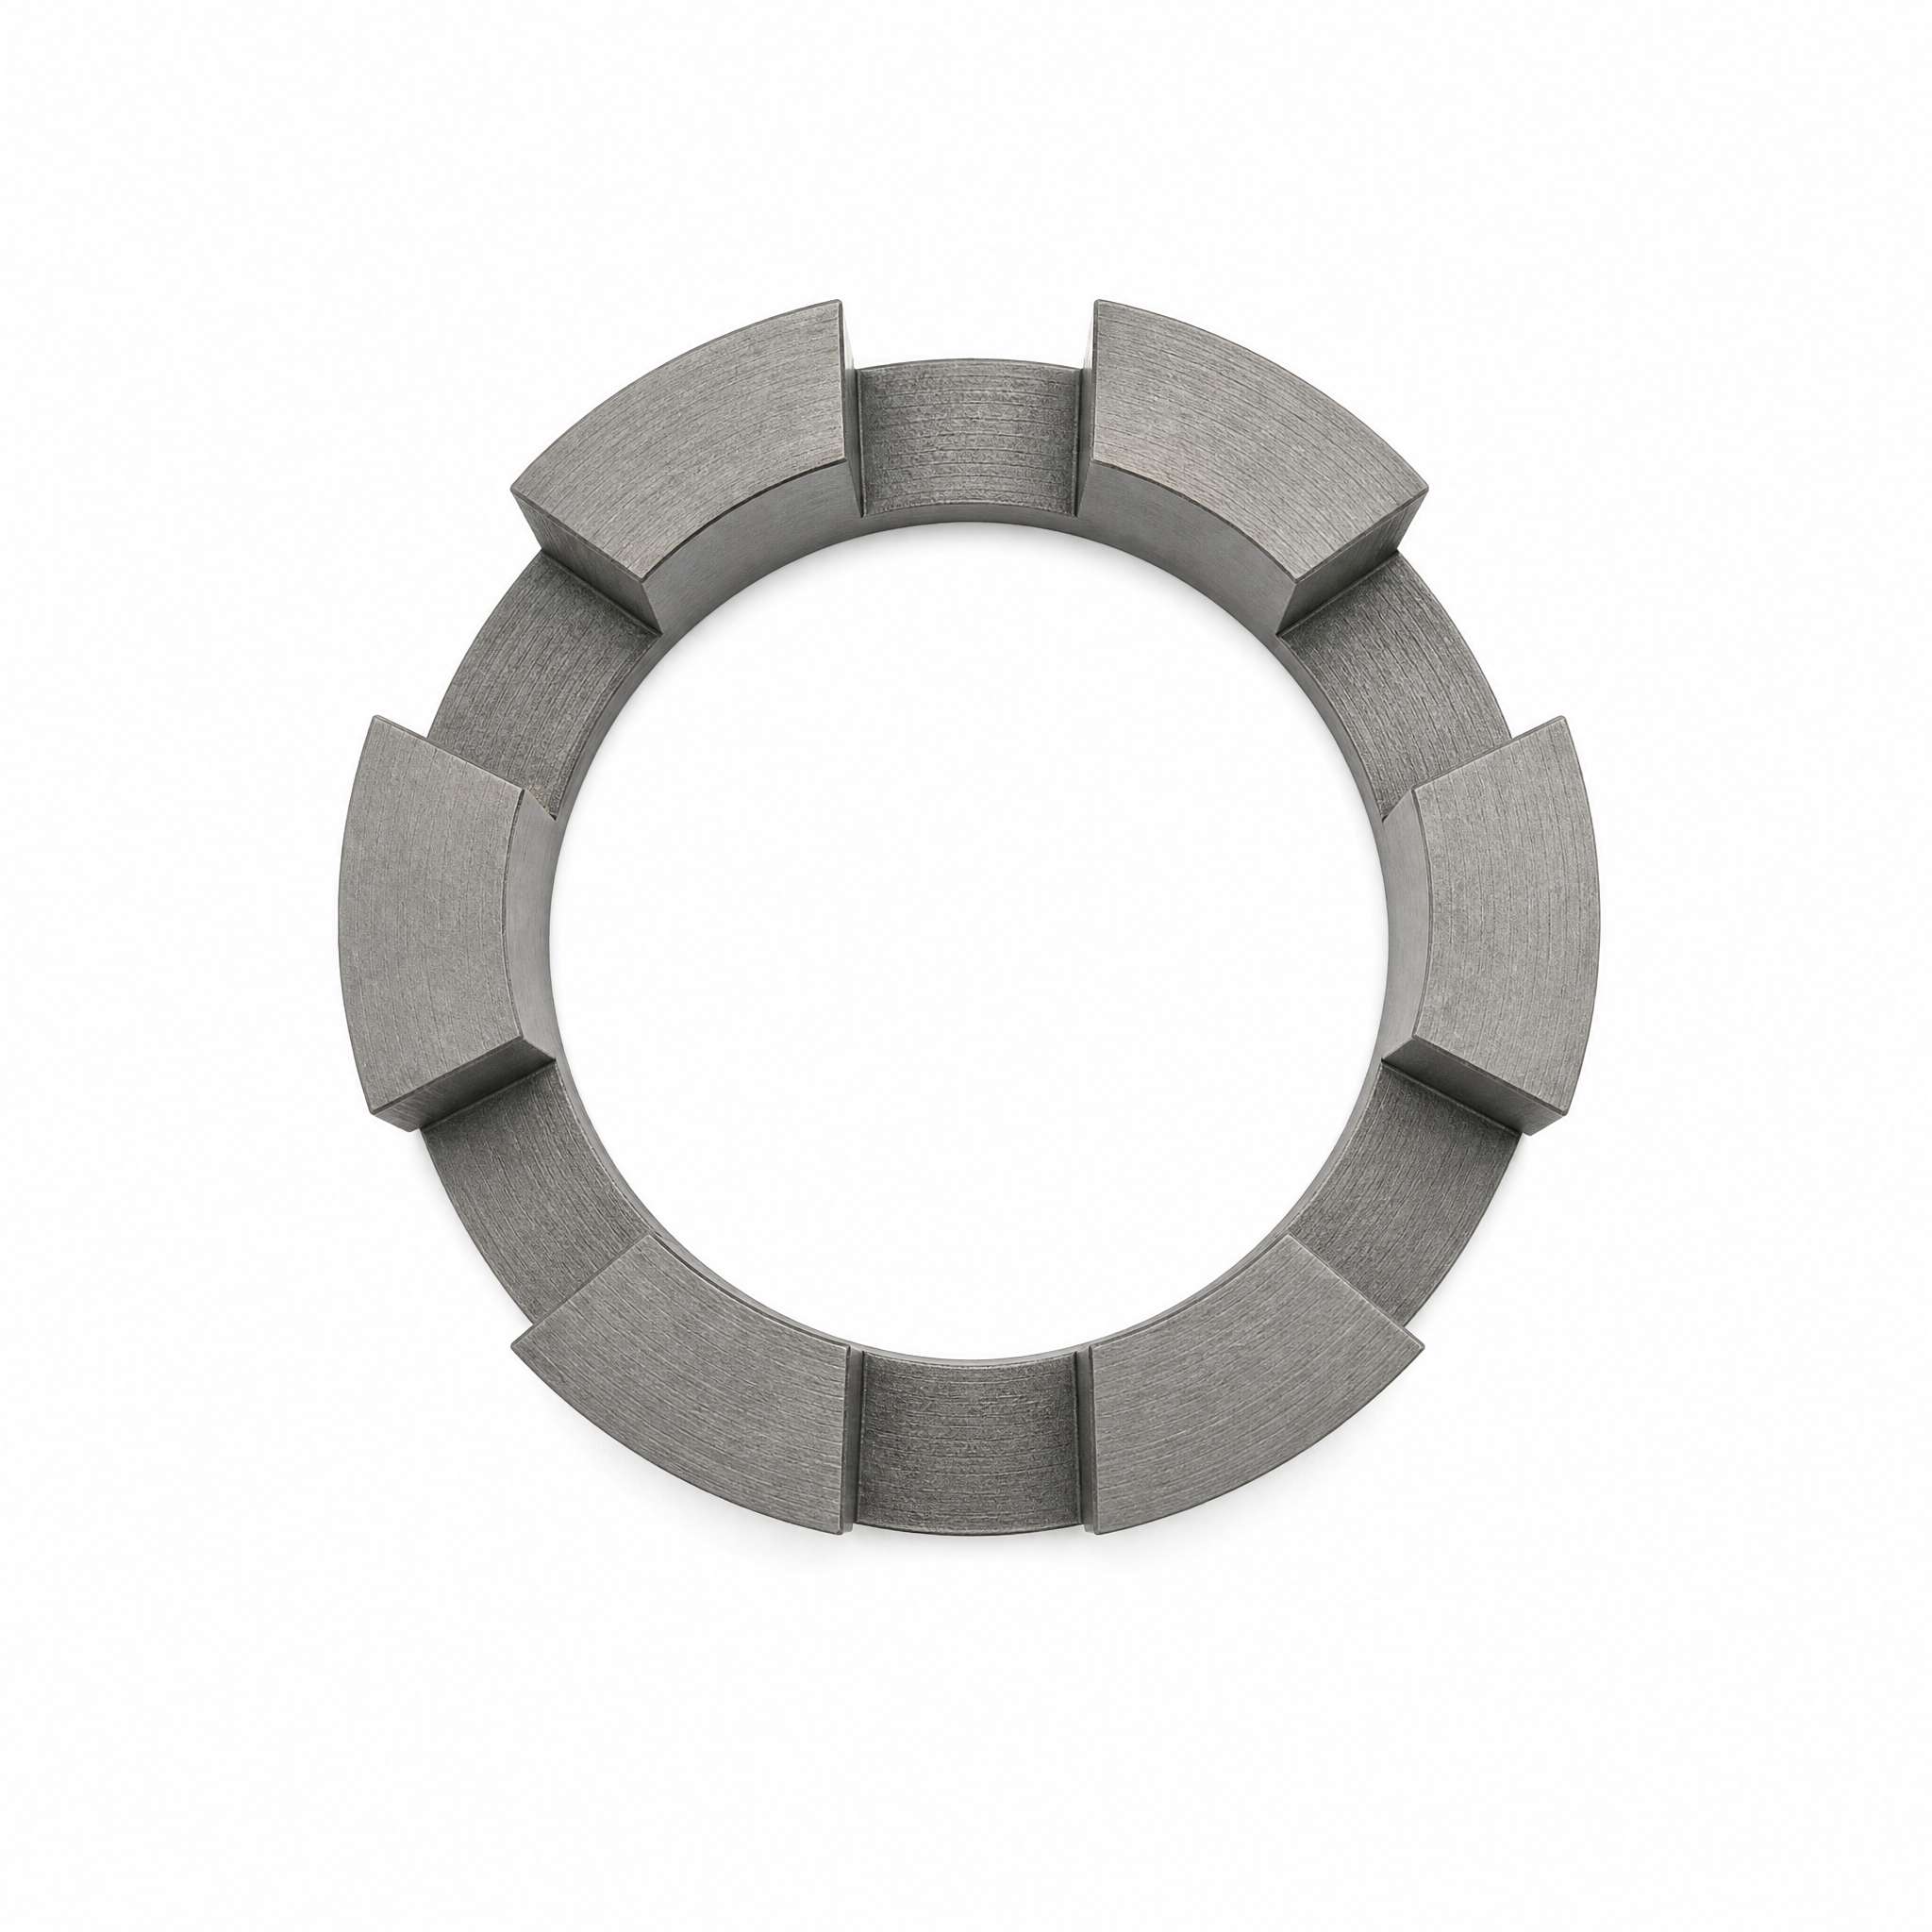
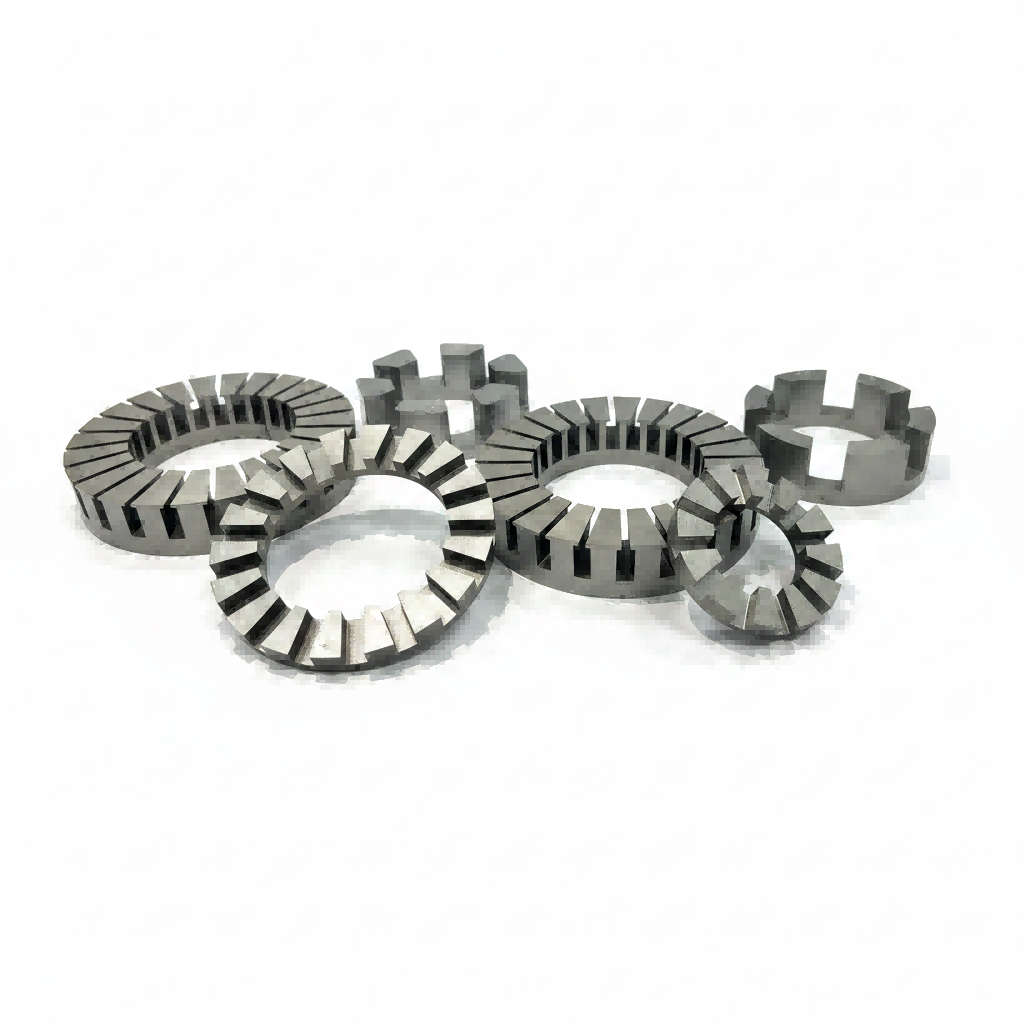
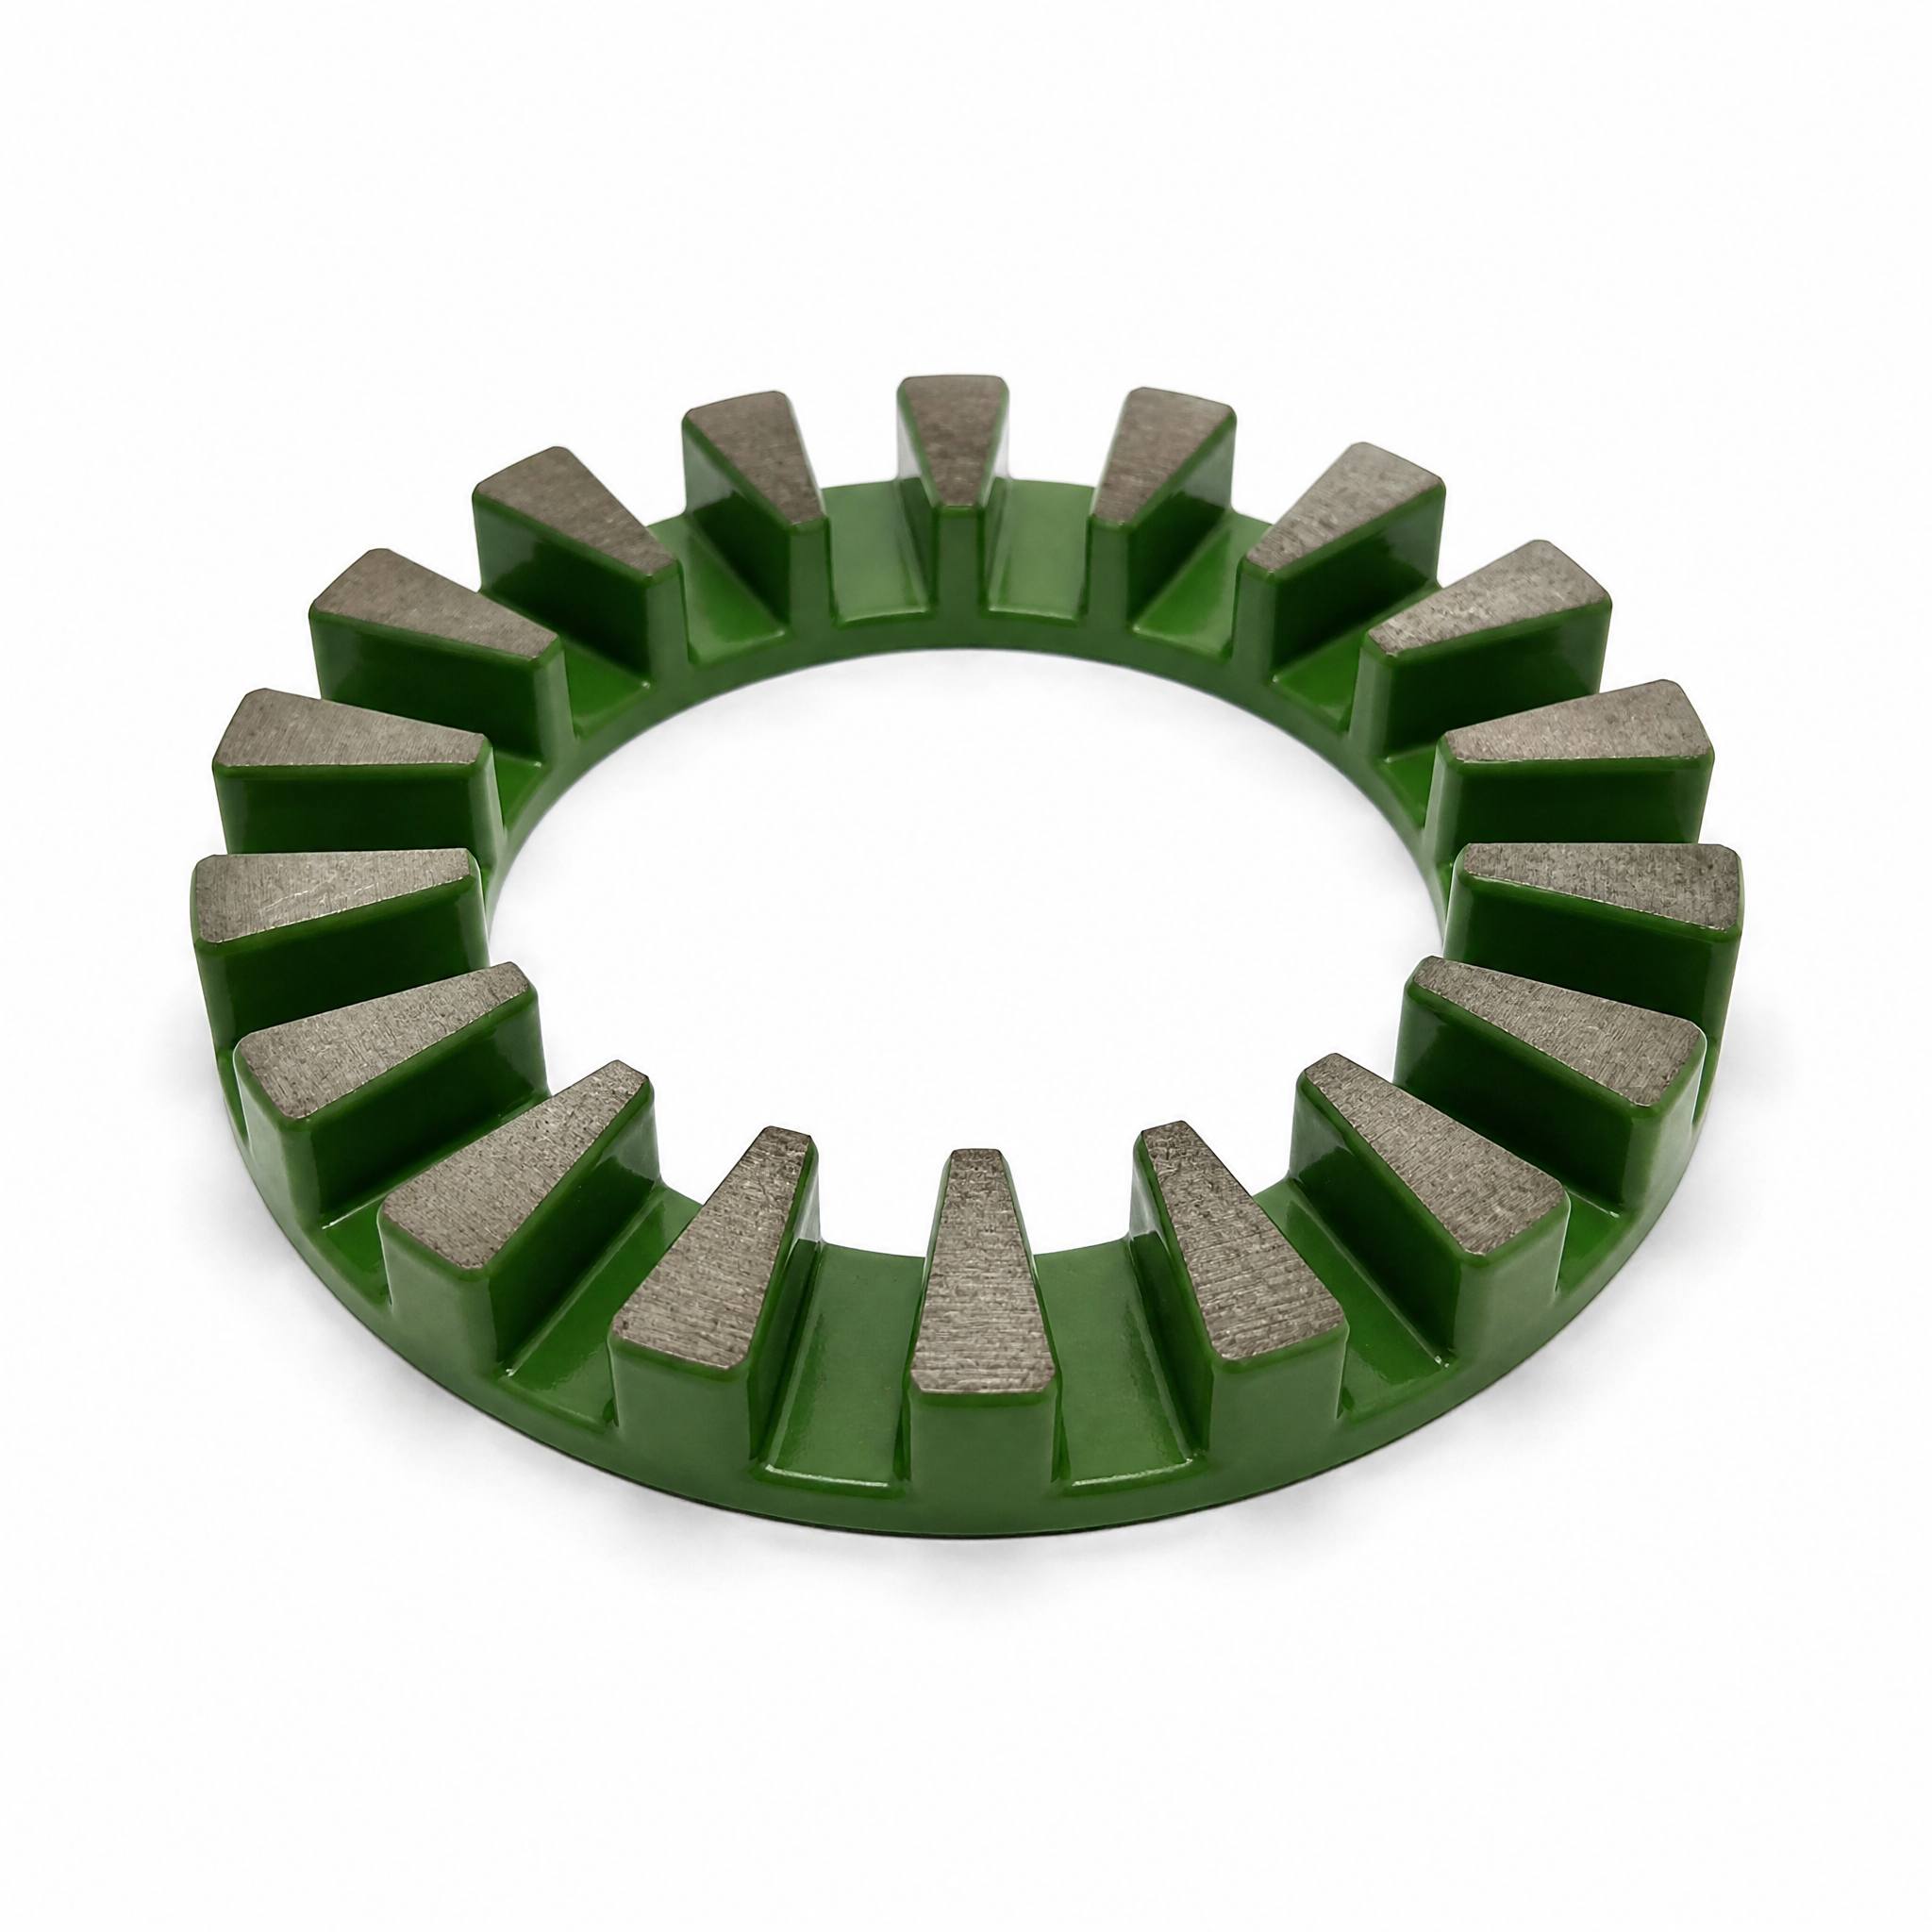
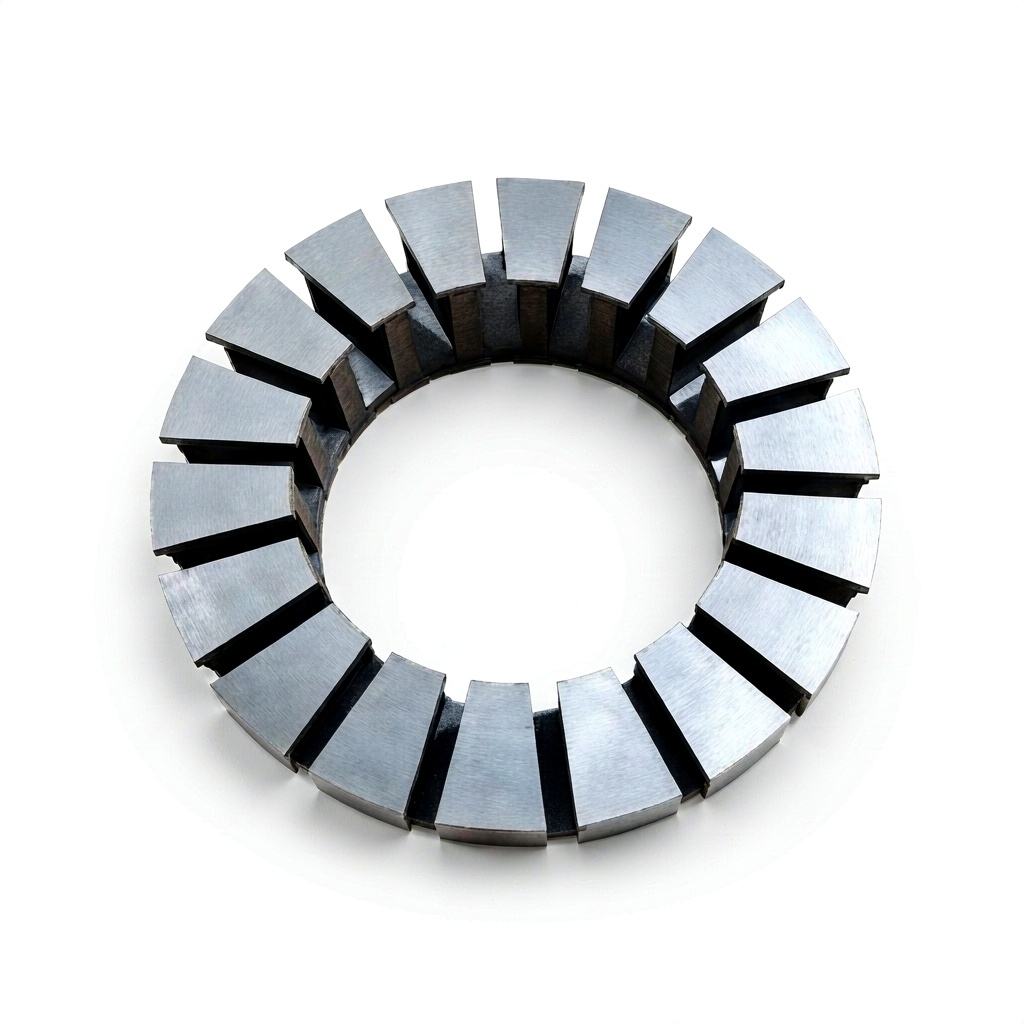
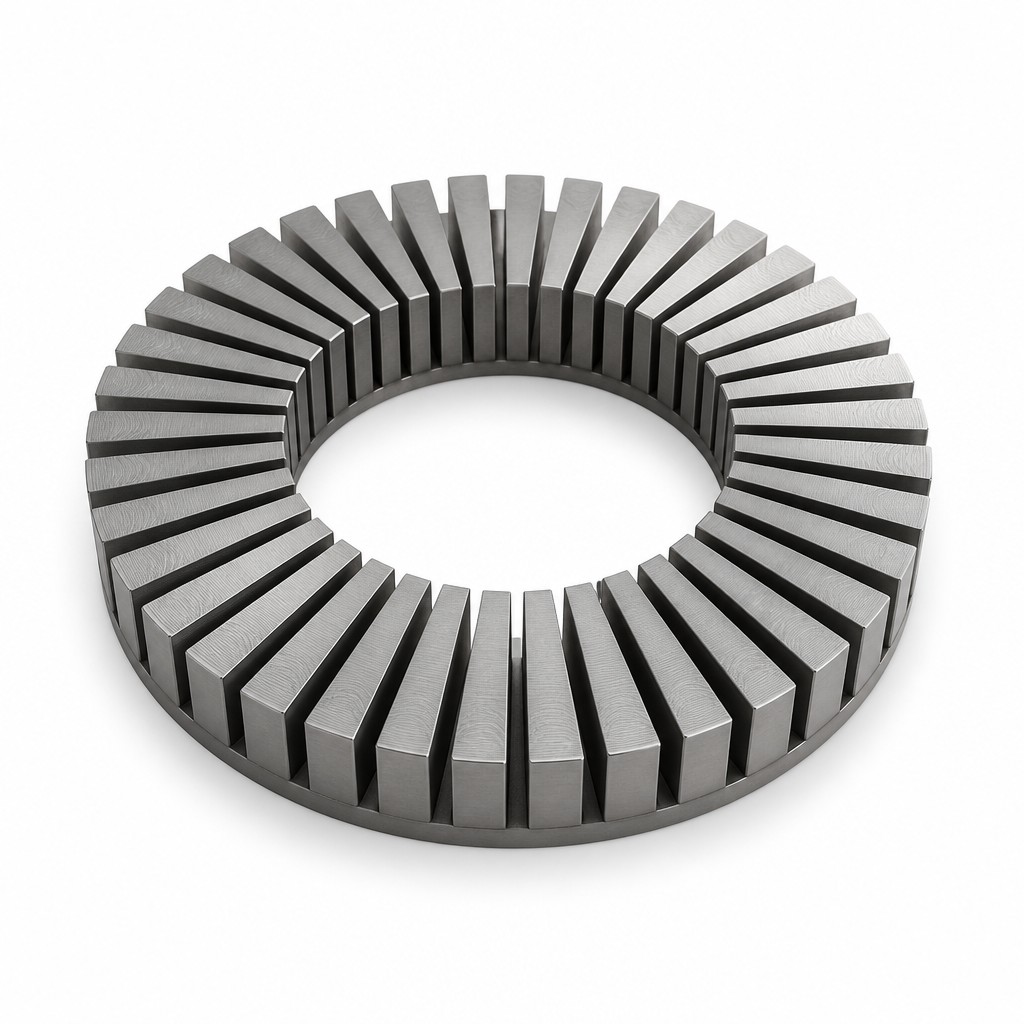
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Product Origin :
CHINAShipping Port :
NANSHA/SHEKOU/SHANGHAI/NINGBOPayment :
TT
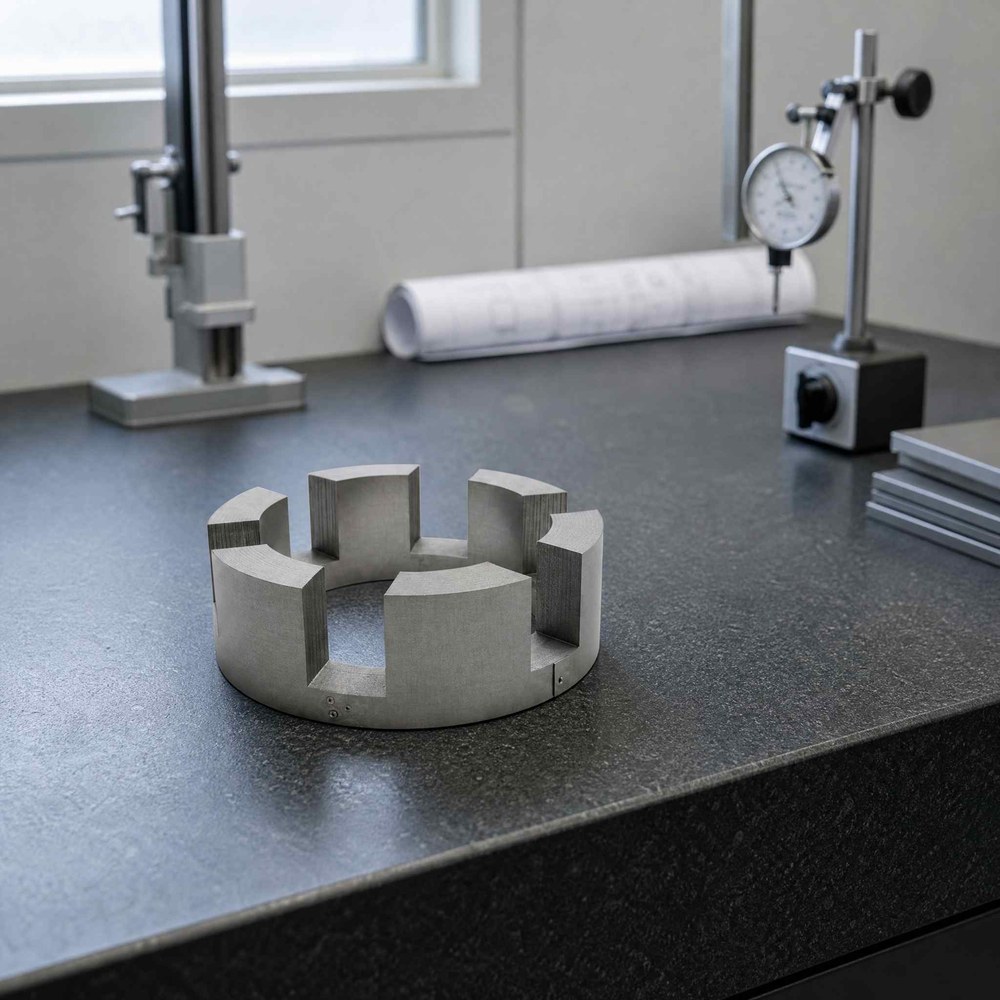
Shunge Steel manufactures custom, high-precision axial flux micro motor stator cores in Foshan, Guangdong, China. Engineered specifically for miniature high-torque and ultra-compact motion systems, our wound axial flux cores deliver exceptional power density in constrained axial spaces where conventional cylindrical (radial flux) micro motors cannot fit.
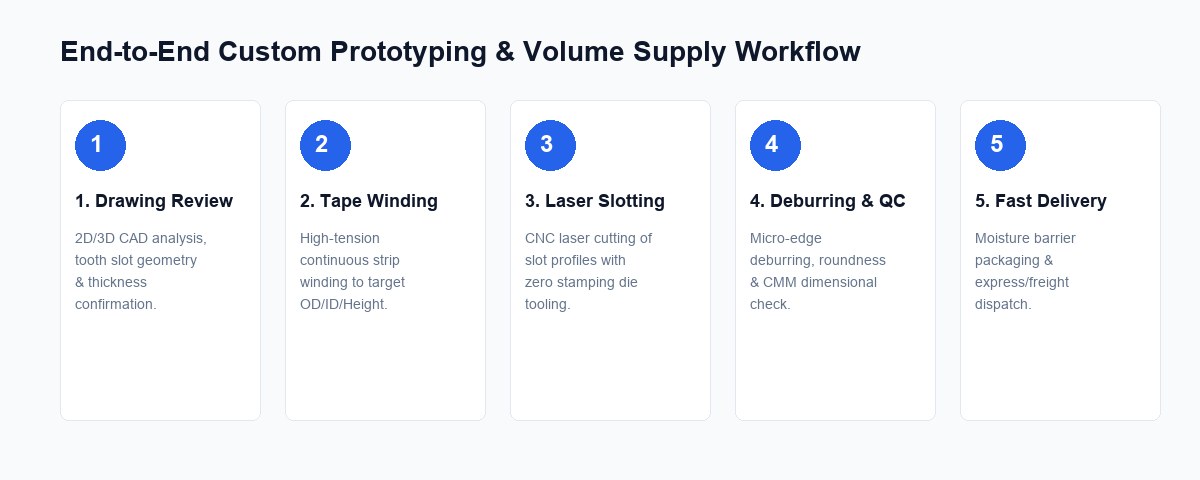
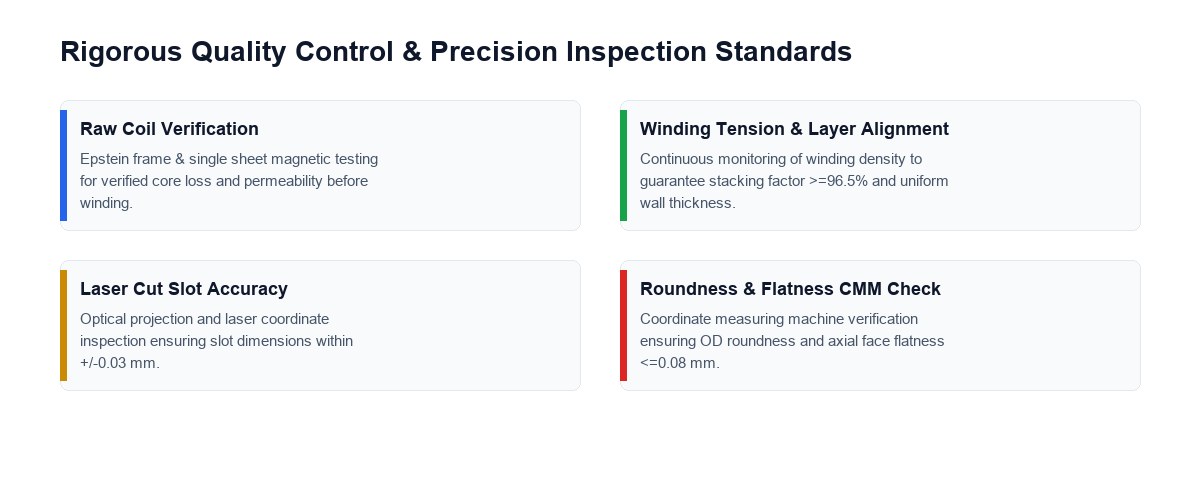
Unlike traditional radial micro motor stators that rely on complex stamped lamination tooling, our axial flux micro stator cores are produced through precision tape winding of ultra-thin electrical steel strips (0.10 mm to 0.35 mm), followed by high-accuracy CNC laser cutting to form custom tooth and slot profiles (such as 6-slot, 8-slot, 12-slot, or custom skewed geometries). This process eliminates expensive stamping die investments, enabling rapid prototyping, flexible design iterations, and highly cost-effective batch manufacturing for medical tools, robotics, optical devices, and aerospace micro-actuators.
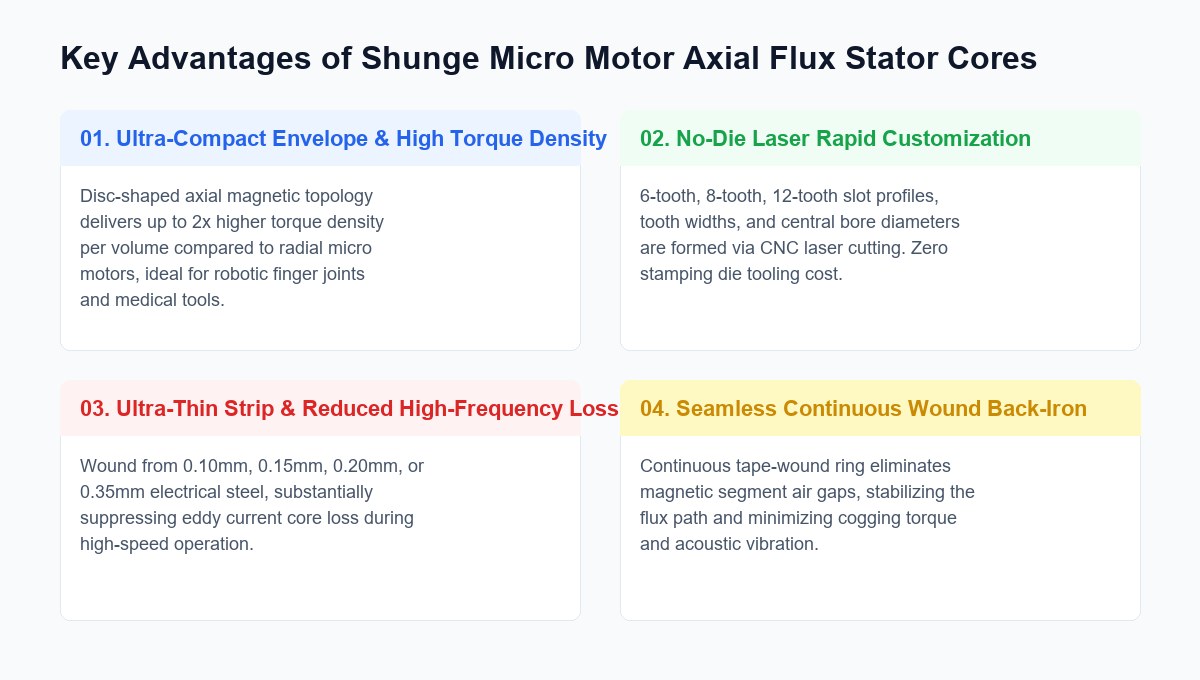
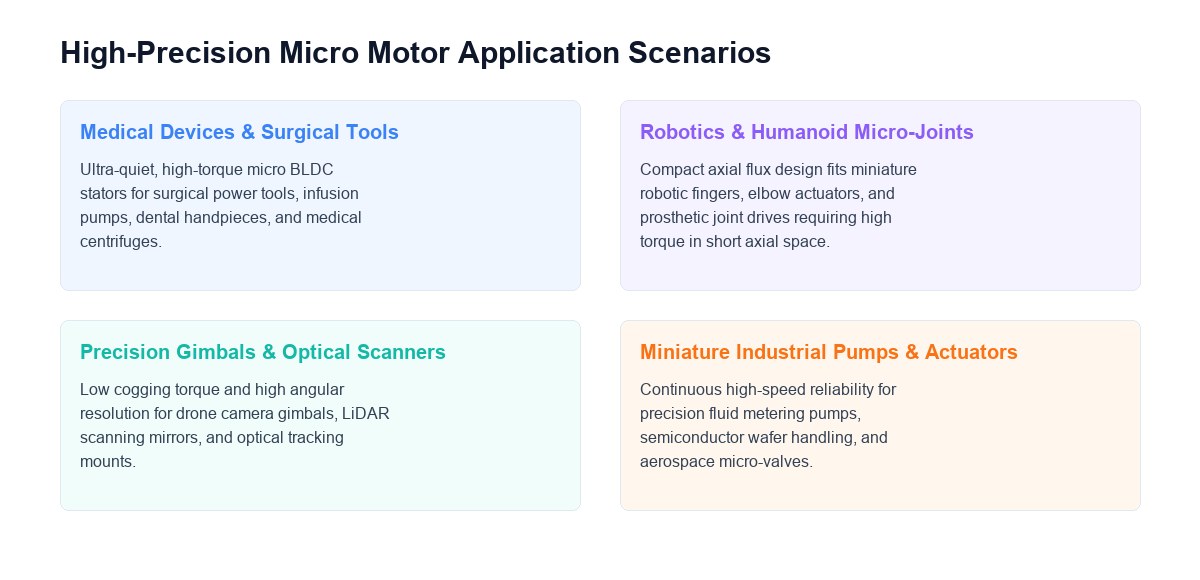
Our custom axial flux micro motor stator cores provide the ideal magnetic core foundation for high-end micro-motion applications:
Q1: What is the main advantage of an axial flux micro motor core compared to a radial flux micro motor?
A: An axial flux micro motor core utilizes an axial magnetic field crossing the air gap parallel to the rotor shaft. This disc-shaped geometry maximizes the active torque-generating surface area within a remarkably short axial length, delivering up to double the torque density of cylindrical radial motors while significantly reducing overall drive weight.
Q2: Do we need to pay for tooling or stamping dies to make a custom 6-slot or 12-slot micro core?
A: No. Because our slot features and tooth shapes are formed via high-precision CNC laser cutting on wound cores, there is zero stamping die tooling cost. You can modify slot geometries or test prototype tooth counts without paying for new dies.
Q3: What electrical steel thickness options do you offer for high-speed micro motors?
A: We routinely process ultra-thin electrical steel strips ranging from 0.10 mm, 0.15 mm, and 0.20 mm up to 0.35 mm. For high-speed micro motors operating at high electrical frequencies, thinner material dramatically reduces eddy current core losses and thermal rise.
Q4: Can Shunge Steel manufacture miniature stators with hollow central bores?
A: Yes. Inner diameters can be customized down to Ø 8 mm or enlarged to accommodate hollow-shaft designs, optical beam paths, slip rings, or internal cable routing for robotic joints.
Q5: What is the turnaround time for micro motor core prototypes?
A: With our no-die laser manufacturing process, engineering prototypes are typically produced, inspected, and dispatched within 7 to 15 business days following CAD drawing sign-off.
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
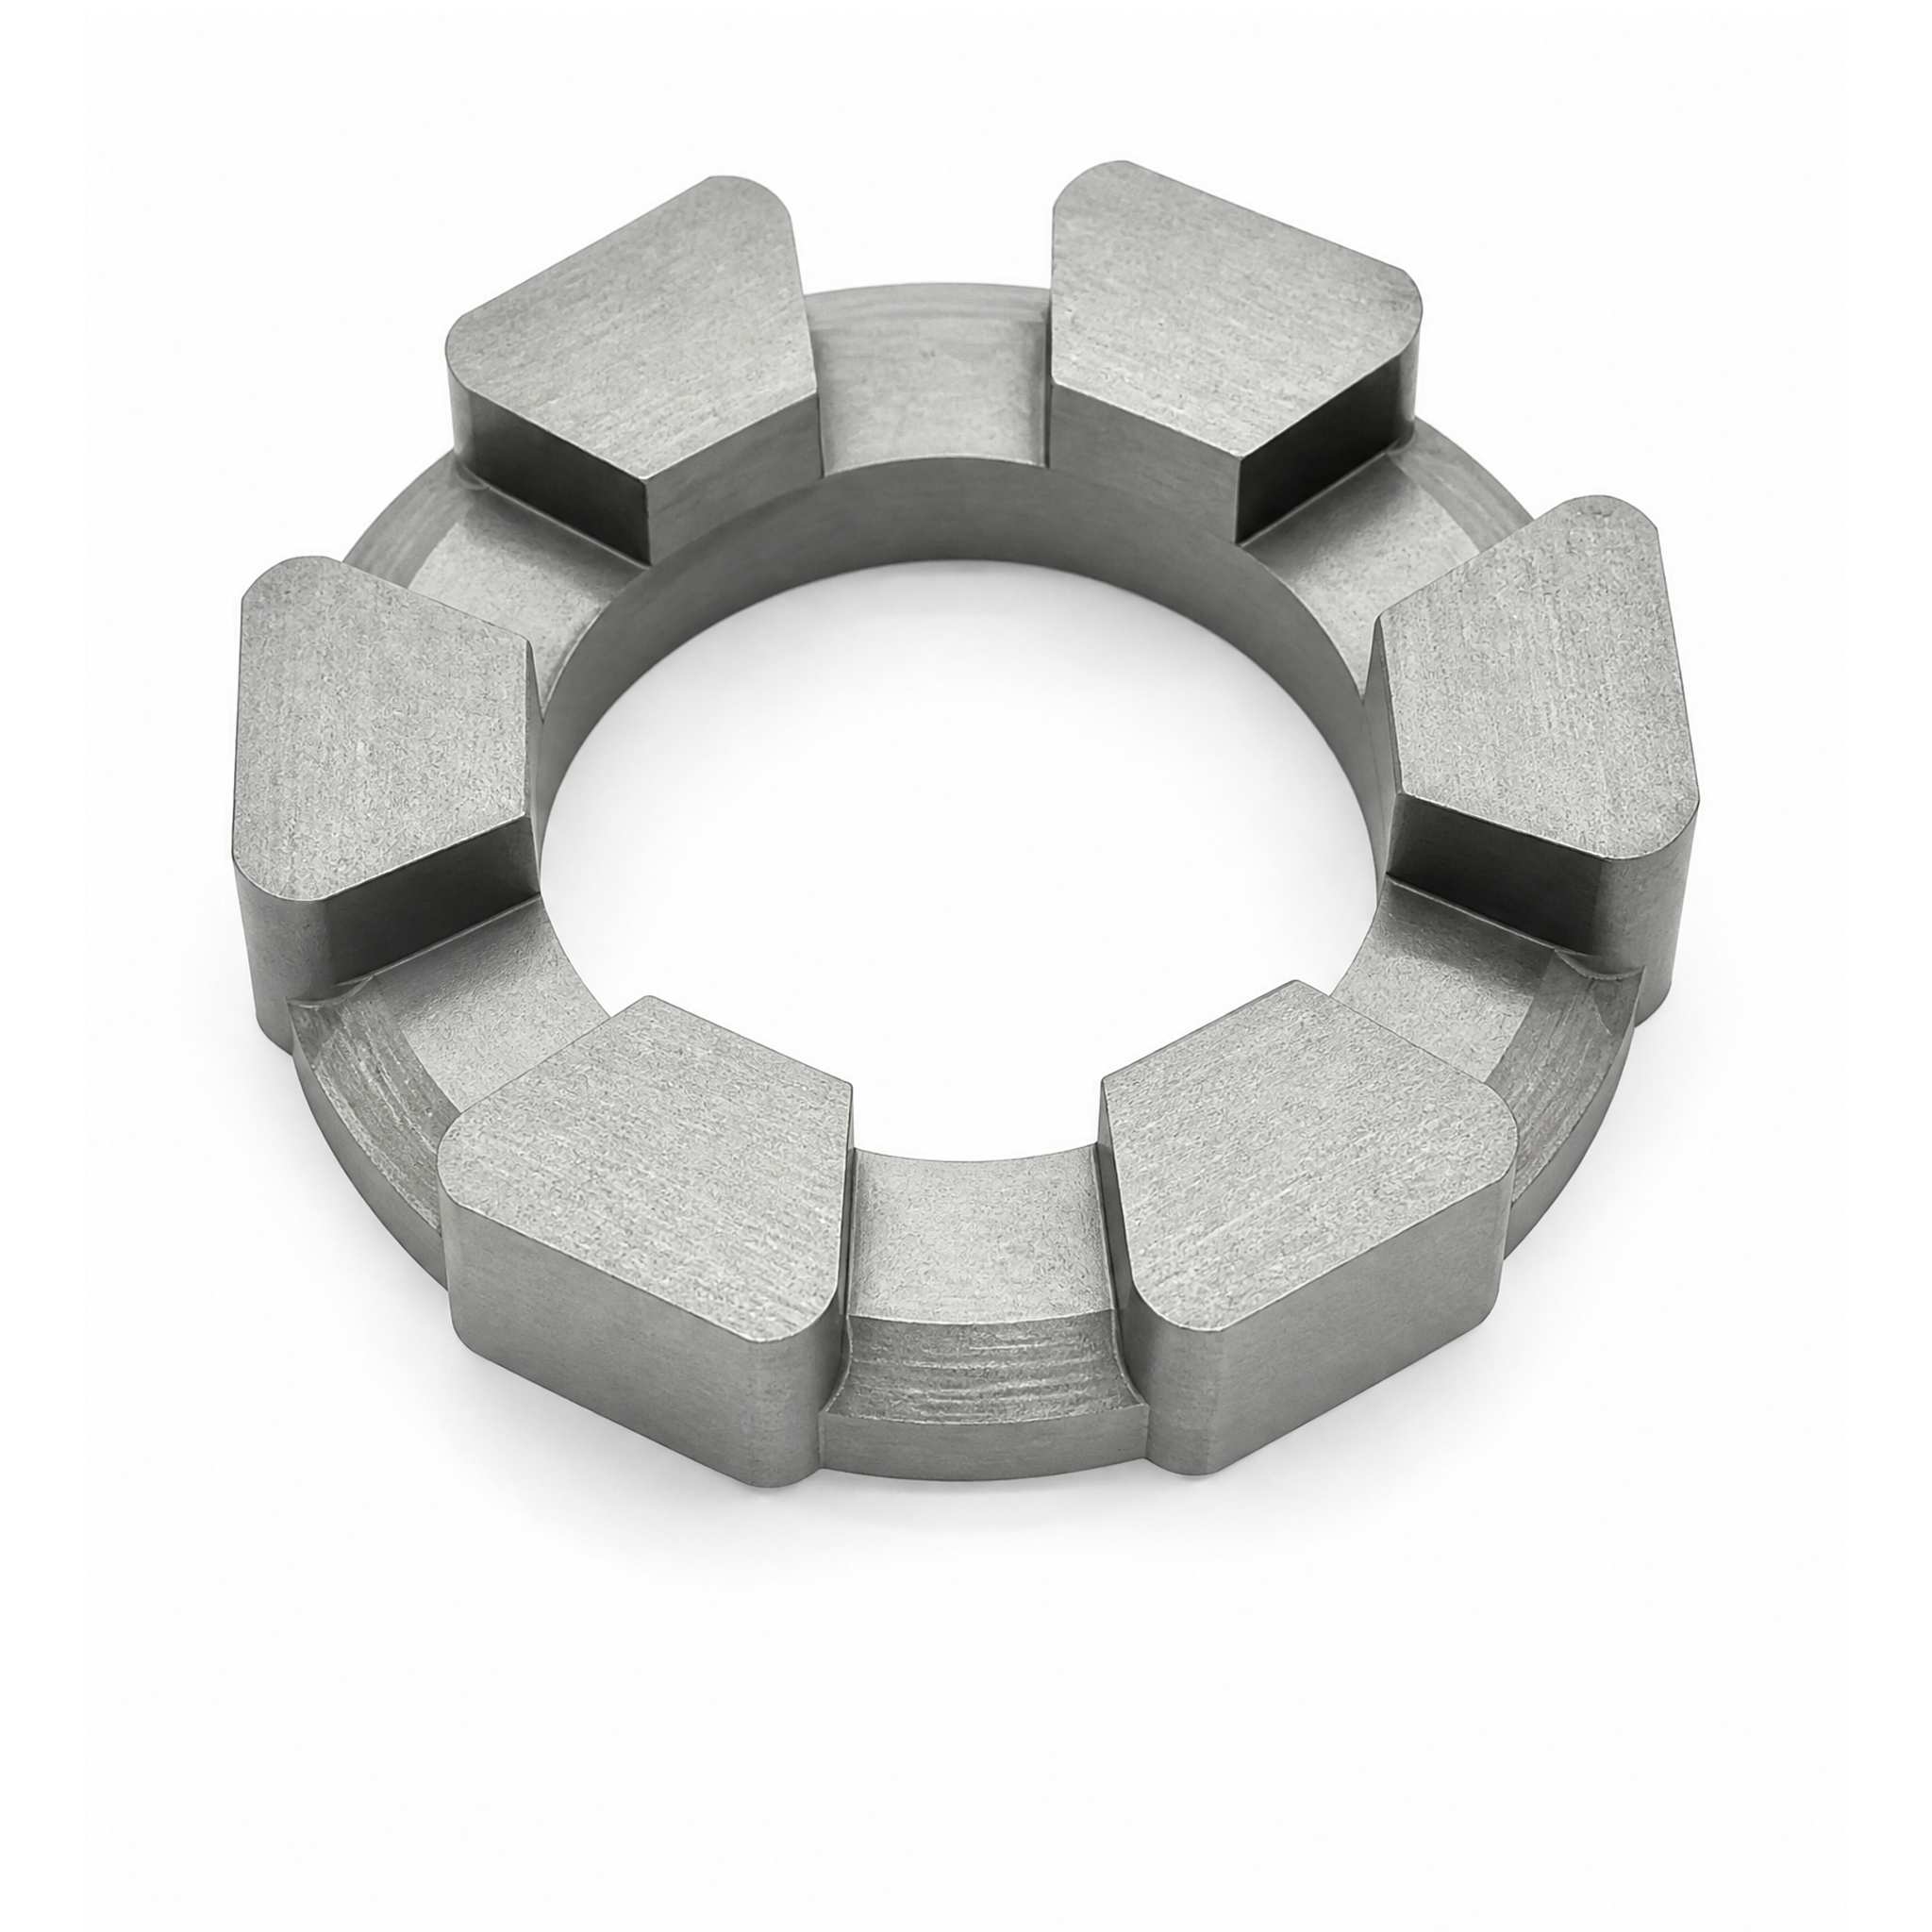
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
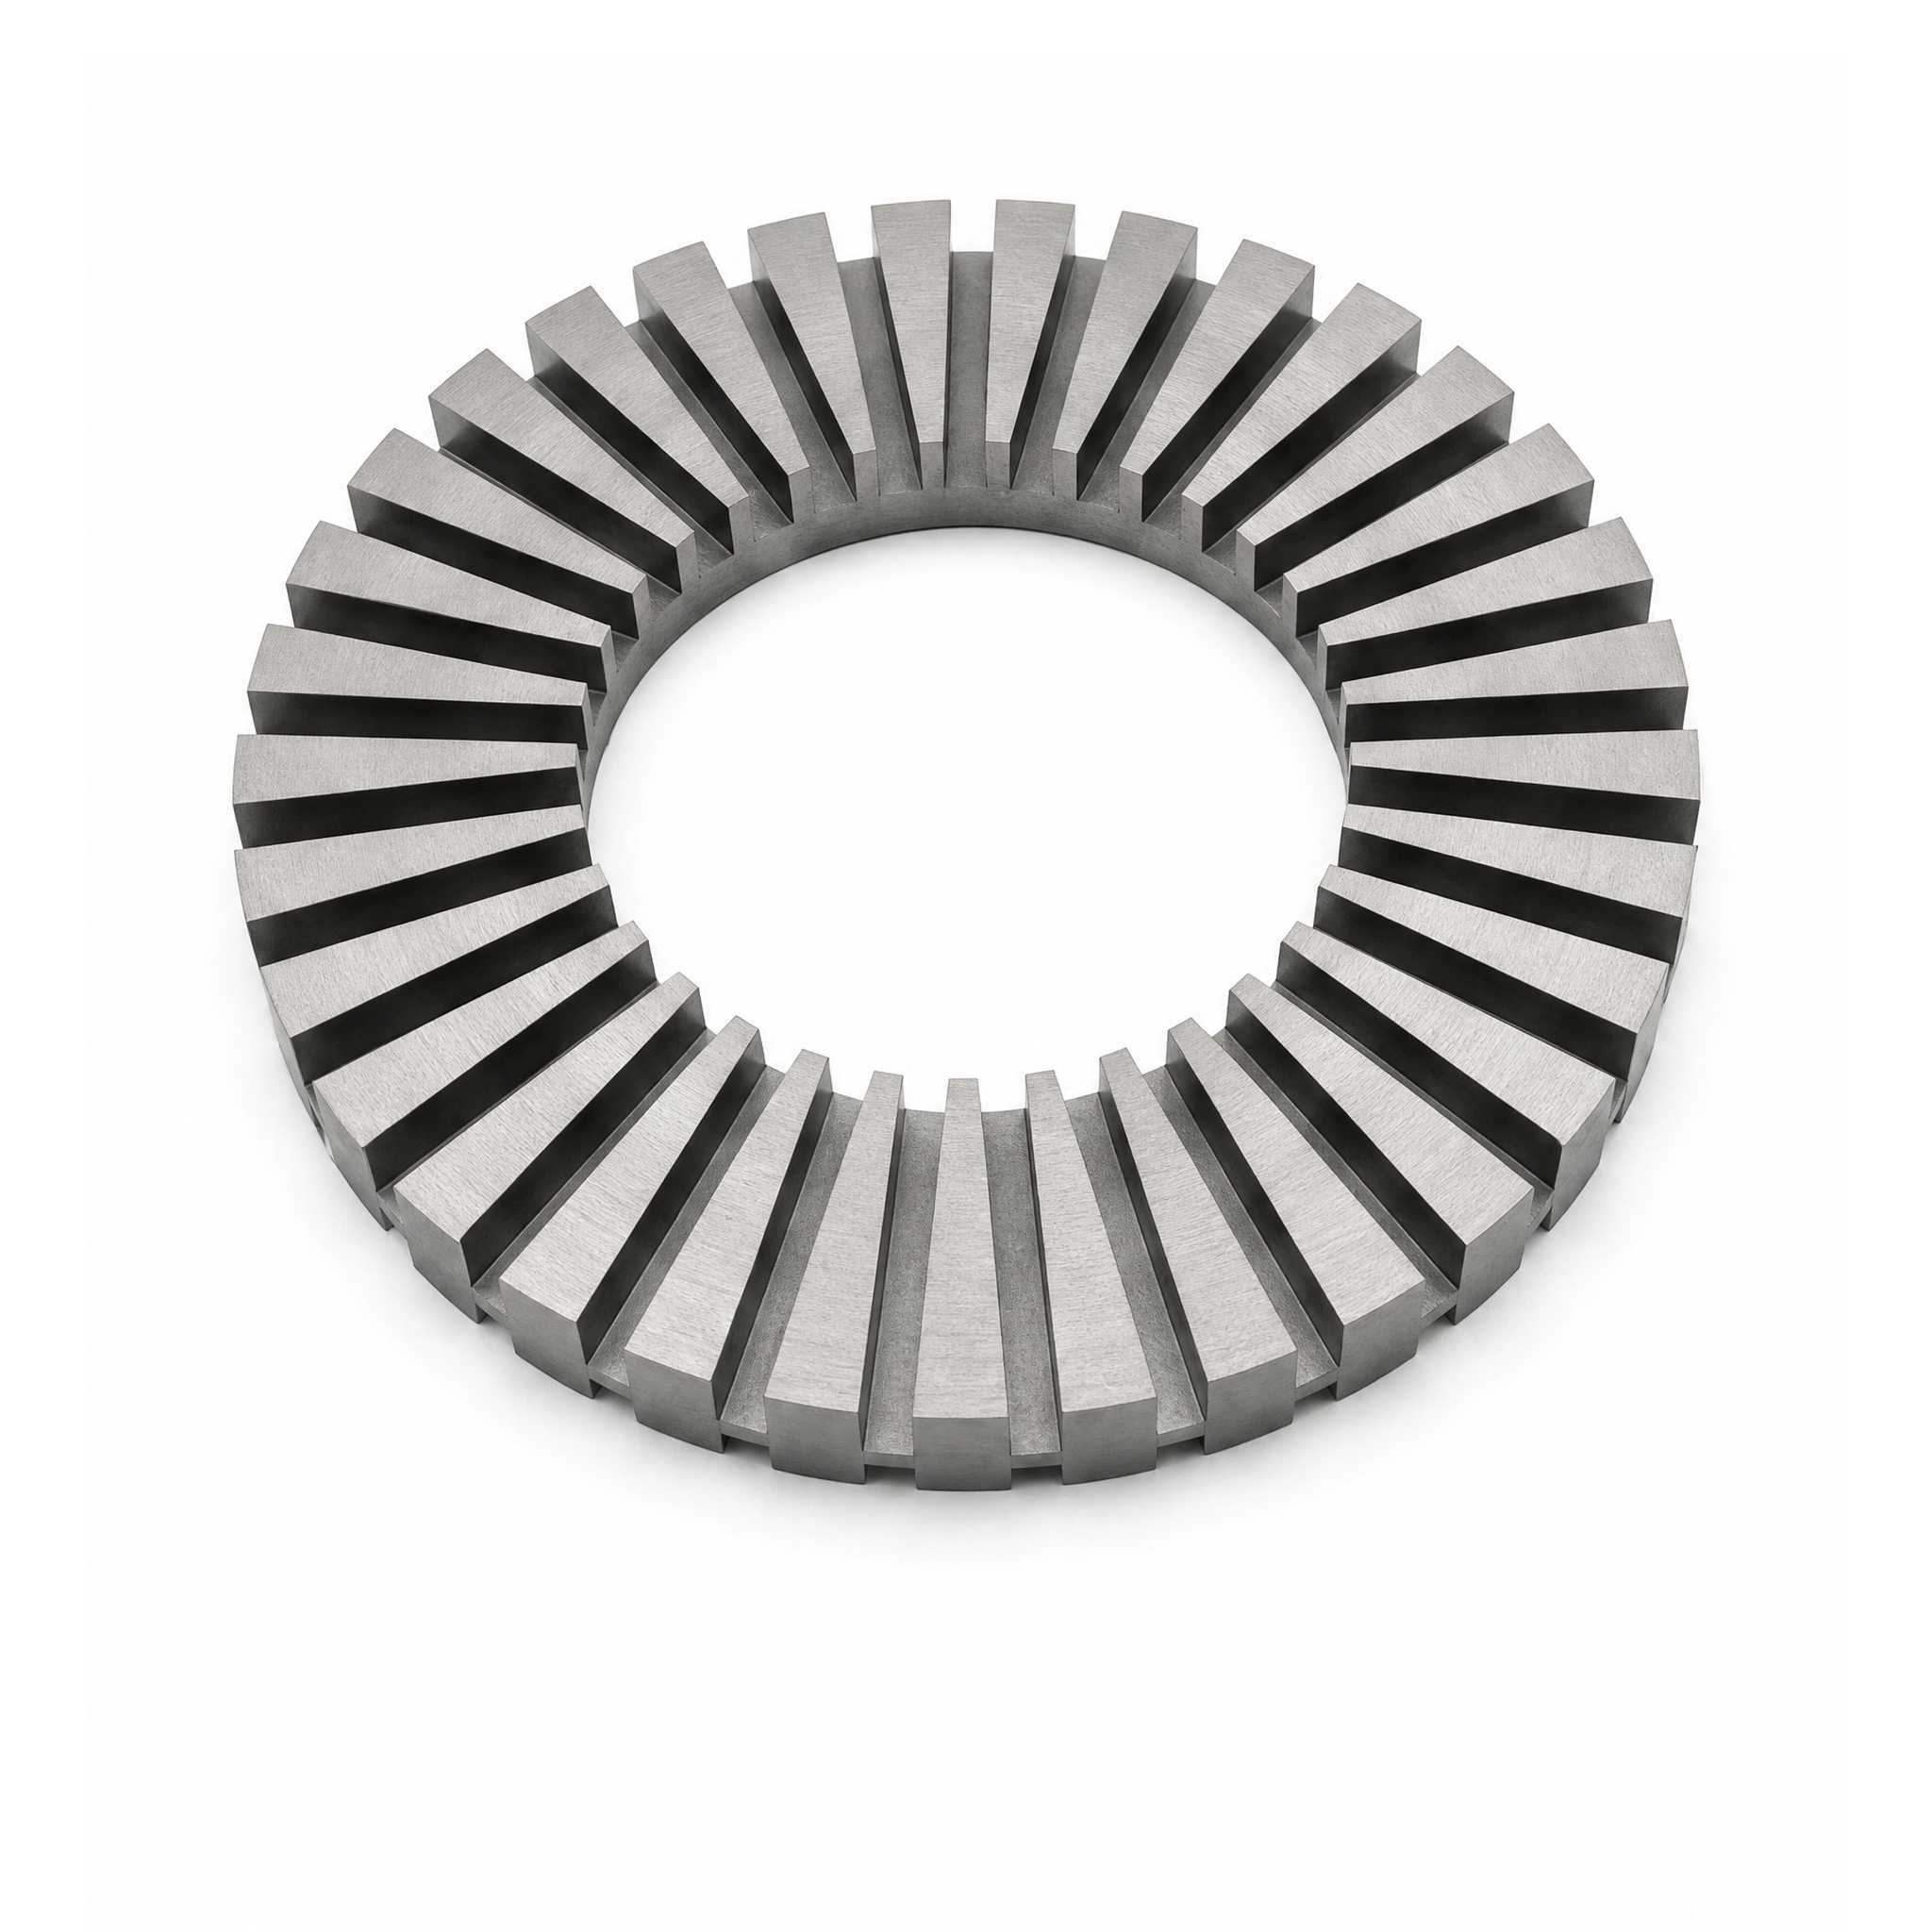
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
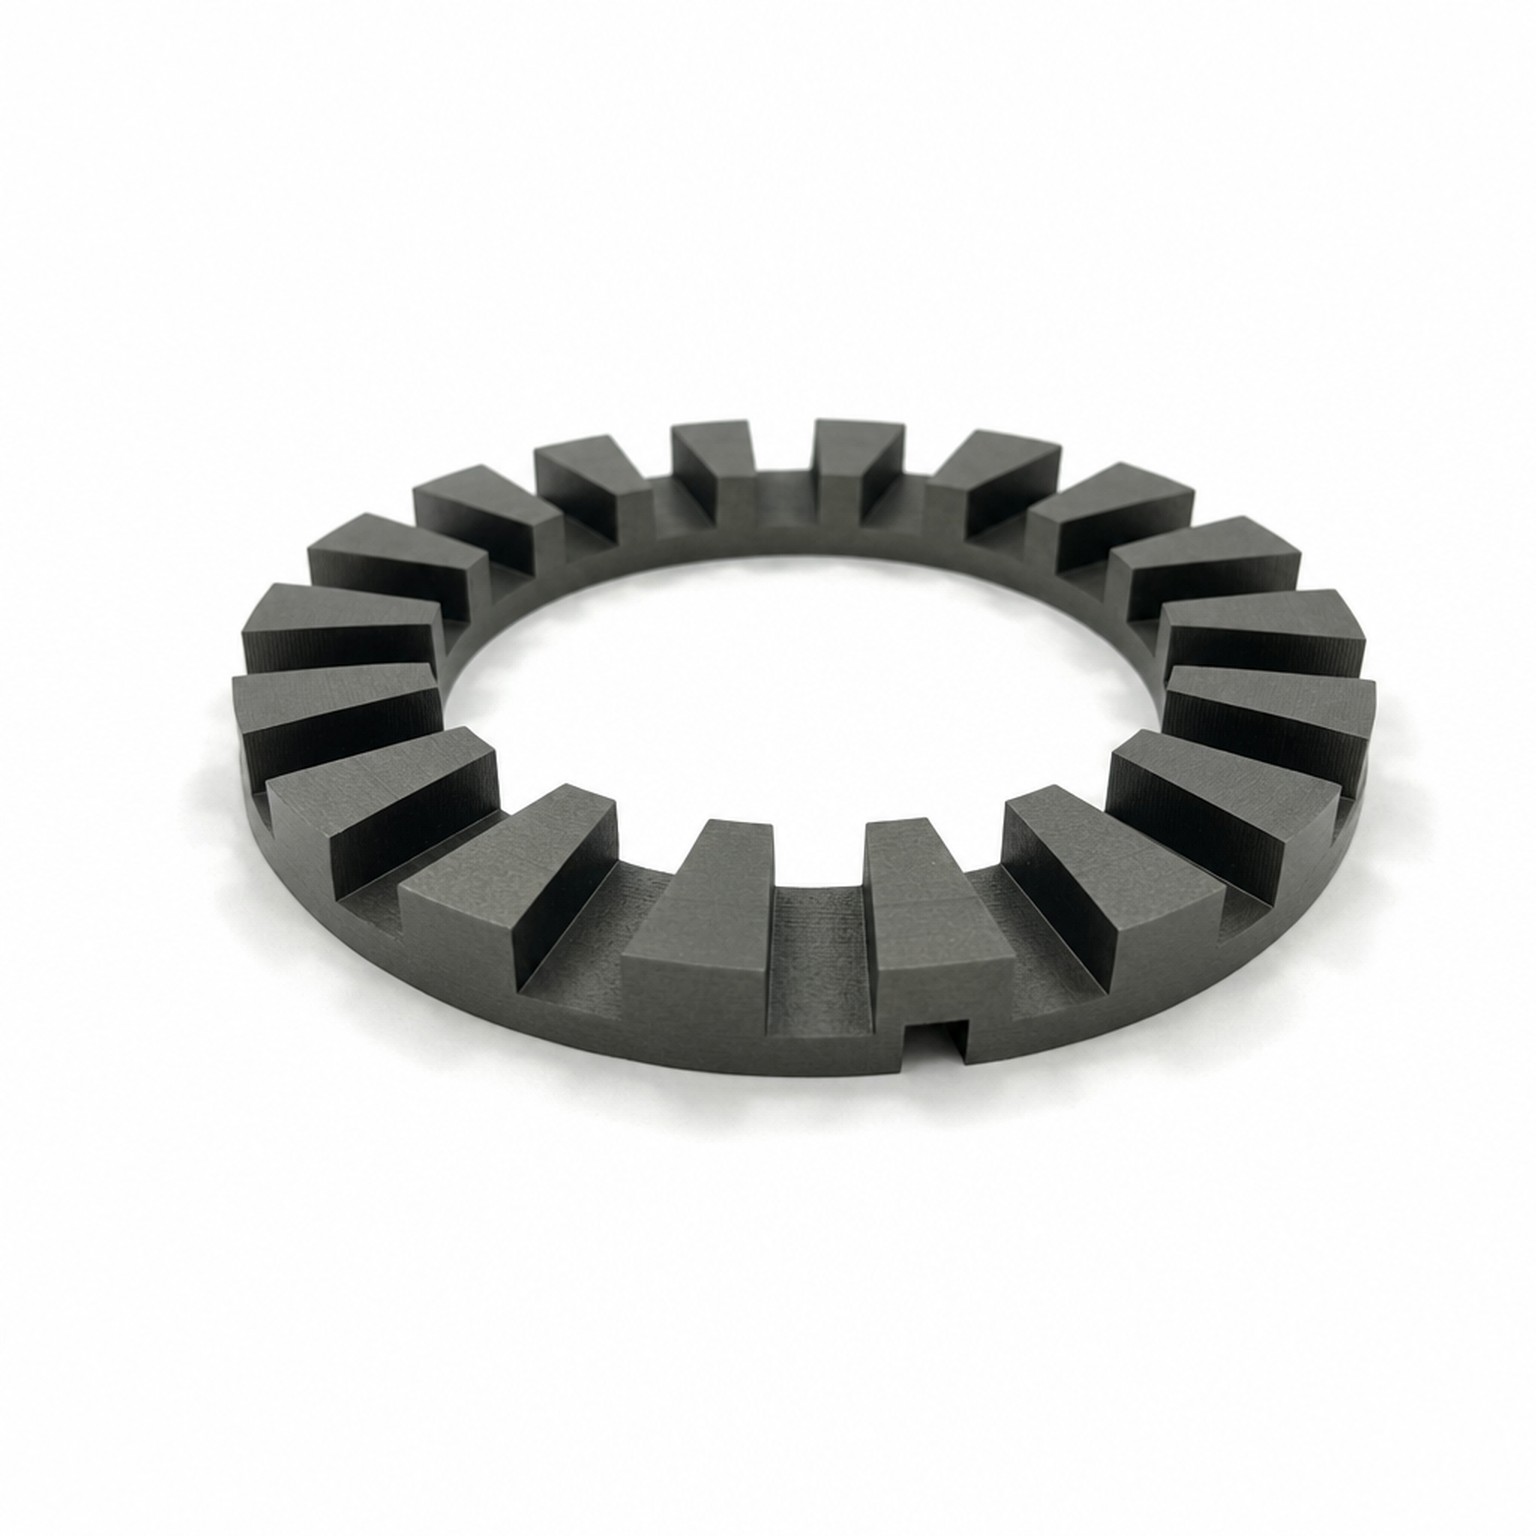
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
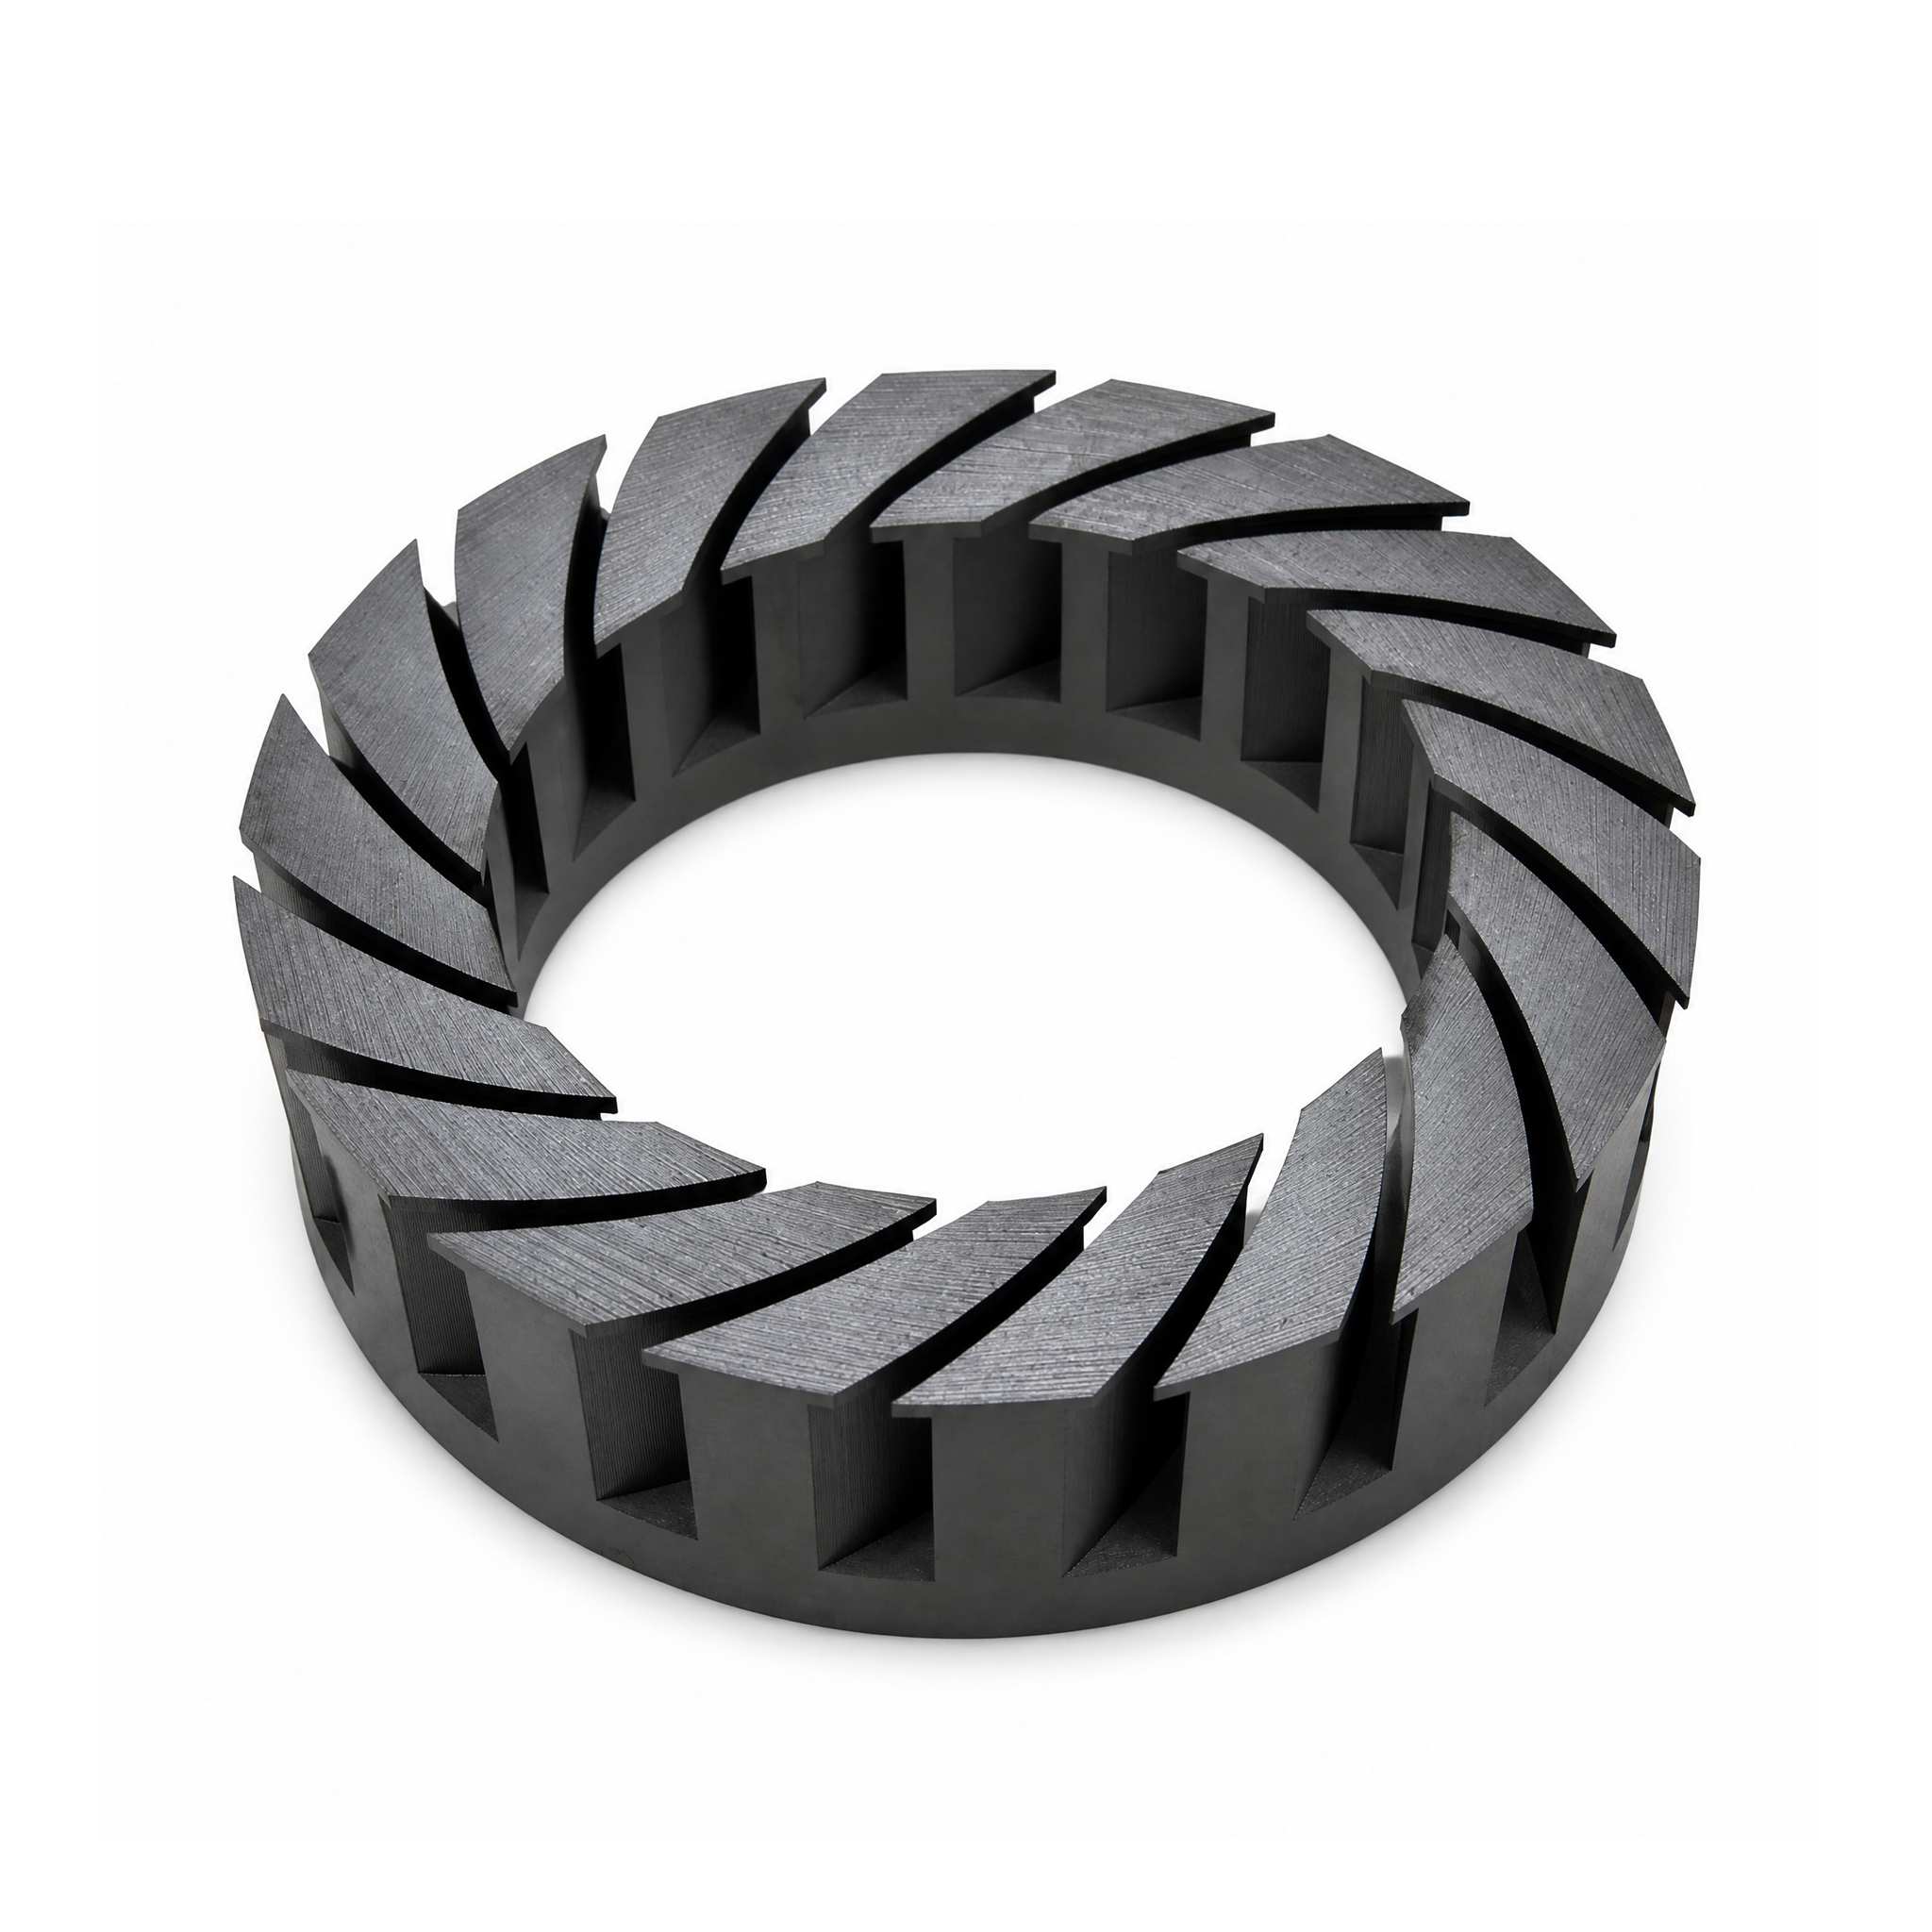
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
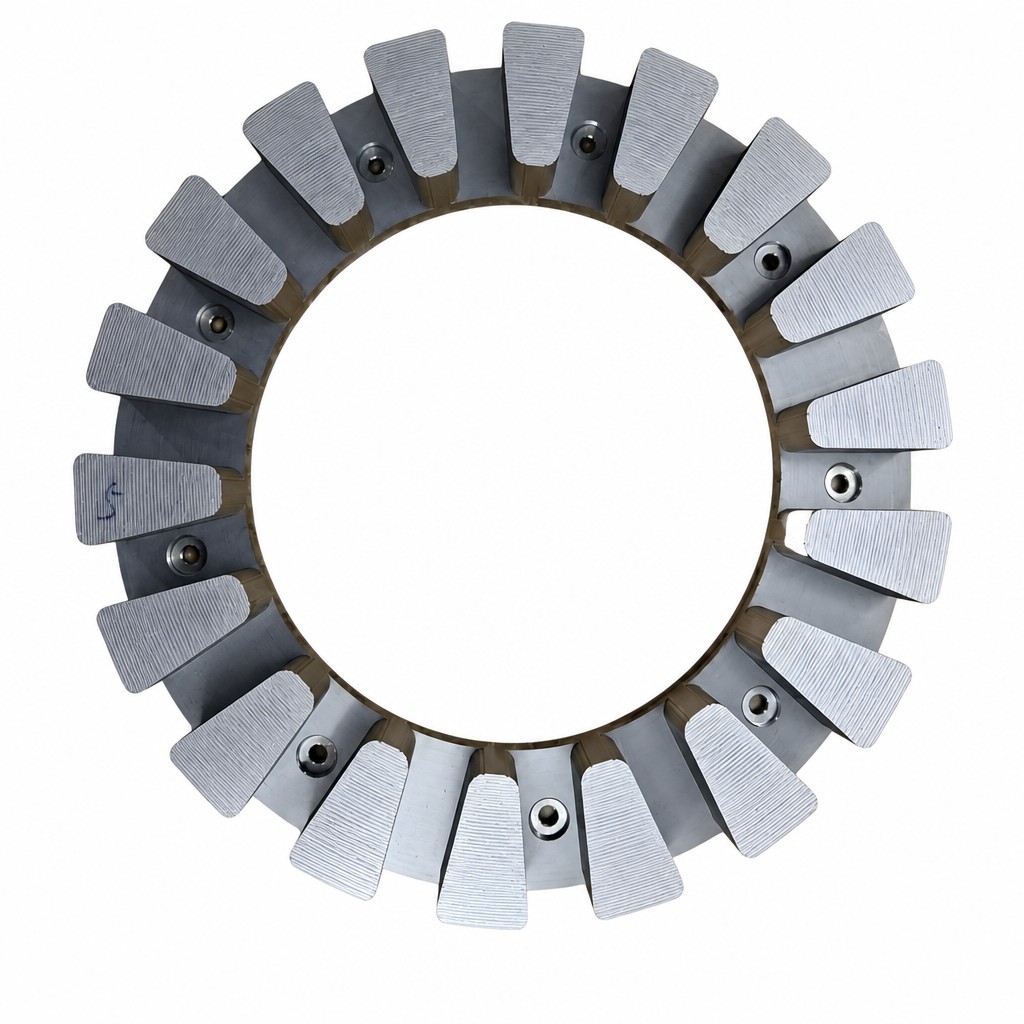
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
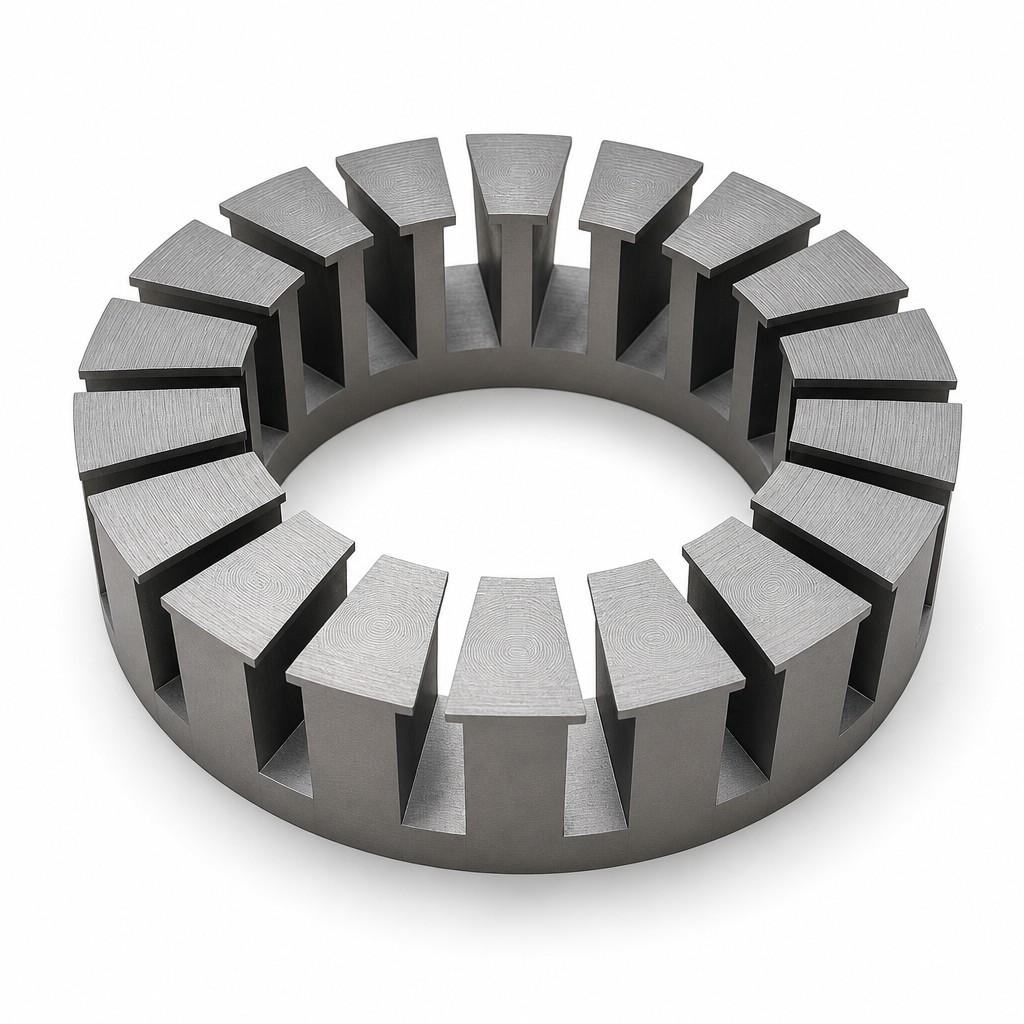
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
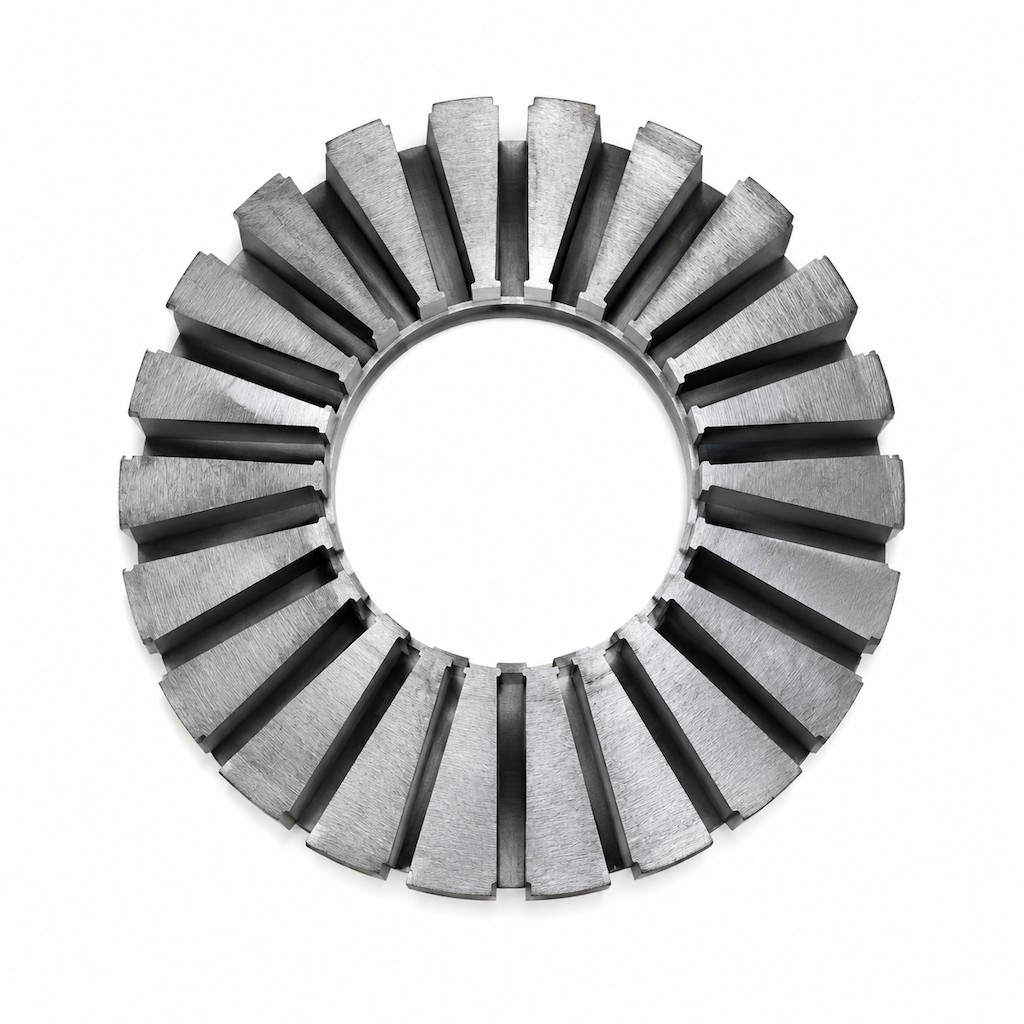
Custom high-precision axial flux micro motor stator cores manufactured from ultra-thin silicon steel strip (0.10 mm to 0.35 mm) using continuous tape winding and precision CNC laser slotting. Engineered specifically for micro BLDC motors, miniature robotic joint actuators, medical surgical devices, precision optical gimbals, and micro-pumps. Features zero stamping die tooling cost, rapid prototype customization, ultra-compact axial height, and high torque density with minimal cogging torque.
Address : Room 201, West Building A, Dawei Logistics, Xihai Industrial Zone, Lecong Town, Shunde District, Foshan City
You may unsubscribe at any moment. For that purpose, please find our contact info in the legal notice.


 IPv6 network supported
We will contact you as soon as possible
Hi! Click one of our members below to chat on